 FOSTA
P 1127 - Materials science-based development of simulation strategies for the use of adiabatic cutting in sheet metal part production
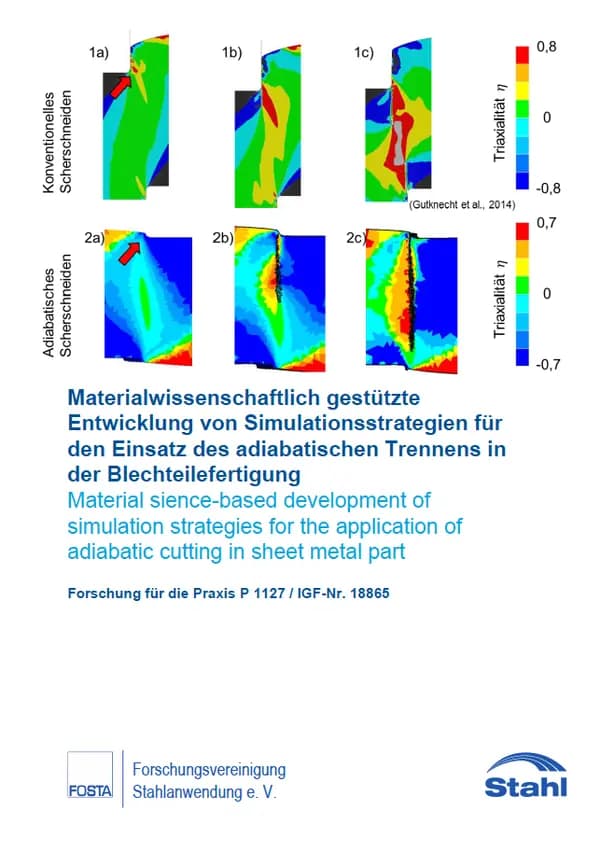
P1127 - Materials science-based development of simulation strategies for the use of adiabatic cutting in sheet metal part production In order to reduce the amount of material used and at the same time pursue the concept of lightweight construction, high-strength steels with tensile strengths greater than 1000 MPa are increasingly being used in automotive engineering. Practically every sheet metal component undergoes a trimming operation during the manufacturing process. However, conventional shear cutting or fine blanking cannot be used for ultra-high-strength steels, or only at great expense in terms of pre- and post-treatment. Here, adiabatic shear cutting offers an alternative to conventional shear cutting or cost-intensive laser trimming. It has already been shown that this process has a high quality in terms of straightness, roundness and surface finish of the shear-cut edge. However, for the industrial use of adiabatic shear cutting, there is a lack of fundamental investigations for relevant high-strength steels, such as frequently used press-hardening steels. Furthermore, the microstructural processes occurring during adiabatic shear cutting and their effect on technological properties have not been described for these steels. Basic approaches for estimating the necessary process energy, process speed and a classification regarding the suitability of the materials to be used are also lacking. The aim of the project is to answer these open questions and to close the gap to industrial application by means of a fundamental characterisation of the process. Furthermore, a methodology for the simulation of the strongly temperature- and strain rate-dependent process is required. Extensive material characterisation tests (temperatures up to 1000 °C and strain rate ?̇ up to 1000 1/s) were carried out to achieve the objectives. Tensile tests with notch geometry were used to determine the failure behaviour. A total of three different steel grades were analysed. Based on these investigations, numerical and analytical models were developed to estimate the locally generated temperature and the process energy required to perform the separation operation. Adiabatic shear cutting tests were carried out to produce cylindrical components and various demonstrators (rectangular plates with rounded edges). Furthermore, it was shown that two of the investigated steels (20MnB5 and C75S), despite almost similar mechanical properties at room temperature under quasi-static load, showed significant differences during adiabatic cutting. In particular, it was shown that the strain rate sensitivity of the steels has a major influence on the initiation and formation of adiabatic shear bands, but at the same time the required process energy is also strongly influenced by this factor. Using finite element simulations, the resulting characteristic shape of the shear-cut surfaces could be predicted with a high degree of accuracy. The methods developed can be used for process design. Publication: May 2020 Authors: Prof. Dr.-Ing. A. E. Tekkaya, Dr.-Ing. T. Clausmeyer, Dipl.-Ing. D. Staupendahl, F. Schmitz M.Sc., Univ.-Prof. Dr.-Ing. habil. M. F.-X. Wagner, Dipl.-Ing. S. Winter
available anytime
View details →€30.00
excl. VAT
 FOSTA
P 1126 - Determination of the load-bearing capacity of novel steel shell structures under realistic consideration of welding distortion
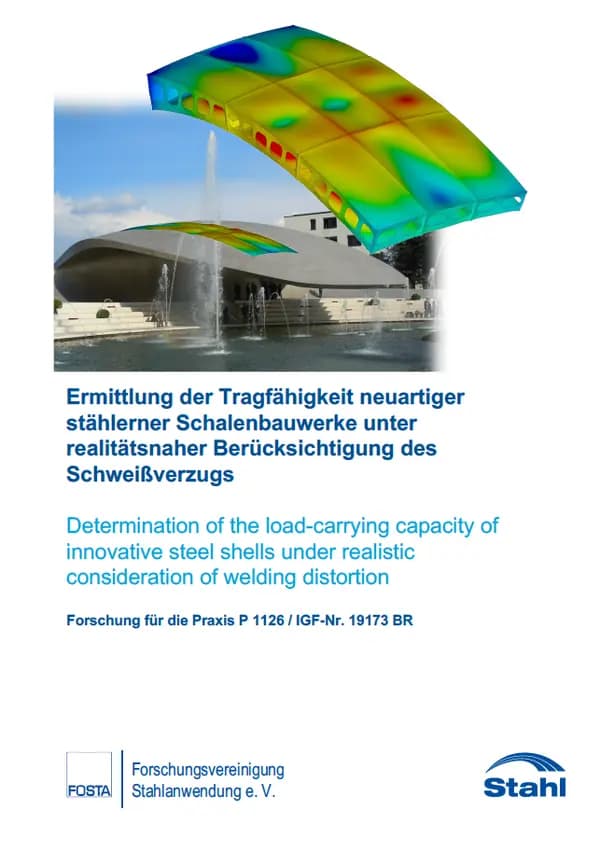
P 1126 - Determination of the load-bearing capacity of novel steel shell structures under realistic consideration of welding distortion Recently, stiffened shell structures (so-called monocoque) have been increasingly used in steel construction. Due to the slender construction methods, buckling is a limit state that must be taken into account. A geometrically and materially non-linear analysis of the imperfect shell structure (GMNIA) has the highest theoretically achievable degree of reality. Its verification quality depends crucially on whether the imperfections introduced into the calculation model describe the effect of the imperfections of real structures equivalently. In principle, it is now possible to reliably predict the effects of the welding process using welding simulation. The analytical-numerical hybrid model developed at the LFT offers a practice-relevant methodology for the welding simulation of large components. From a design perspective, an interface to the welding simulation is to be realised and subsequently verified. The aim of the project was to provide a robust and reliable calculation method for a numerically supported GMNIA verification of welded shell structures. In contrast to previous approaches, this is the first time that this has been done directly using hybrid approaches to capture the influences of the welding process. The analytical numerical hybrid model was used to calculate the welding imperfections. In order to be able to use the model to calculate the welding imperfections that occur when welding curved structures in space, the underlying analytical model had to be extended. Based on numerical variation calculations, an acquisition function was derived that takes into account the curvature in space and the resulting reduced stiffness. The hybrid model has already been successfully applied to a large number of differently complex components. However, the focus was on welding distortions. Little attention has been paid to the localised stress state in the near-seam area. However, it influences the load-bearing behaviour of welded components. Both the verification of the stresses calculated using the hybrid model with the results from thermomechanical calculations and the validation with radiographic measurements showed good agreement. Only a new meshing strategy was developed to improve this. Since in most cases the stiffeners are welded on both sides, an influence function was derived based on the source method, which takes into account the intermediate time between the two welds and records its effect on the plastic strains. Publication: August 2020 Authors: Prof. Dr.-Ing. habil. H. Pasternak, Dr.-Ing. Ch.Stapelfeld, Dr.-Ing. Launert, Prof. Dr.-Ing. habil. V. G. Michailov, Dr.-Ing. N. Doynov, C. A. Kaya
available anytime
View details →€30.00
excl. VAT
 FOSTA
P 1125 - Increasing technological properties by cryo-treatment of tool steels
P 1125 - Increasing technological properties by cryo-treatment of tool steels As part of the project, the effects of cryogenic treatment on the microstructure, mechanical properties and wear resistance of the high-alloy tool steels X38CrMoV5-3 (electroslag remelting process (ESR)), X153CrMoV12 (powder metallurgy (PM) and fusion metallurgy (SM)) and ~X190CrVMo20-4 (PM) were investigated. The tempering parameters of the samples for the mechanical tests and those of the wear samples were selected on the basis of the tempering curves so that a similar hardness was present for both the conventionally heat-treated and the cryo-treated samples. Although a finer, martensitic microstructure and a more homogeneous distribution of secondary carbides in the X38CrMoV5-3 was achieved by including a cryogenic treatment in the conventional heat treatment or an increased amount and a more homogeneous distribution of secondary and nano carbides in the X153CrMoV12 and ~X190CrVMo20-4 steels could be attributed to the cryogenic treatment, no differences were found in the mechanical properties and in various wear tests (sandpaper method, wear cup and cavitation erosion). The wear resistance of the high-alloy tool steels depends to a large extent on the primary carbides and the macro hardness, less on the secondary or nano carbides. Both cryo-treatment and tempering three times at high temperatures achieved an almost complete conversion of the retained austenite into martensite in the small samples. Cryogenic treatment of tool components with large wall thicknesses would have a positive effect, as a uniform and complete transformation of the retained austenite is achieved over the entire cross-section. This allows the user to better assess the cryogenic treatment technology and thus utilise it in a more targeted manner, thereby achieving improved results or saving costs. Publication: 2021 Authors: Dr.-Ing. A. Schulz, Dr.-Ing. F. Nürnberger, Dipl.-Ing. T. Ümit
available anytime
View details →€30.00
excl. VAT
 FOSTA
P 1123 - Hollow section truss structures with bonded strut connections
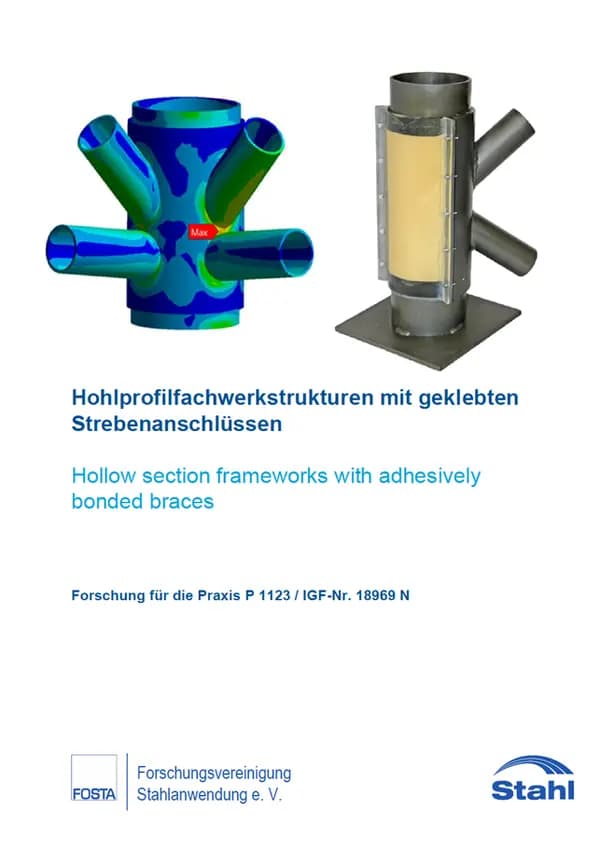
P 1123 - Hollow section truss structures with bonded strut connections Foundation structures for offshore wind turbines are often designed as jacket truss structures for water depths of more than 20 metres. Until now, the individual hollow profiles of these truss structures have been joined by welding. Due to the spatial intersection of the pipe profiles at the junctions and the resulting complex weld seam geometries, as well as the large open areas required for final assembly, this represents a major manufacturing effort. An innovative hybrid connection of the struts to the corner posts of these supporting structures is the focus of this research project. The concept combines the joining methods of bonding, welding and bolting by forming nodal partial shells at the ends of the struts. These individual partial shells are formed in such a way that they enclose the corner strut and are completed to form a complete shell during assembly. After the individual partial shells have been bolted together, the remaining gap between the gusset ring shell and the corner post tube wall is joined using adhesive technology. This work step takes place in the manufacturing plant and therefore under defined ambient conditions. This design has the advantage that permanently acting static loads (such as dead weight) are almost completely dissipated by the continuous corner stems. Furthermore, the lack of welded connections on the corner posts results in an increase in local fatigue strength. In addition, the hybrid connection enables prefabrication of the struts and the modular design of the jacket. First, the requirements and boundary conditions of the jacket support structure are analysed and defined in the research project. In close cooperation with companies from the offshore wind energy sector, the stresses from wind, wave impact and turbine operation are determined. Real climate data measured on research platforms in the North Sea is also analysed and the requirements for the adhesive bond are derived from this. Due to the dimensional tolerances of the bonded parts, thick-film bonds of up to 25 mm are required. Extensive numerical investigations are used to analyse the stress on the bonded joint and steel structure. Numerical models of the entire jacket support structure are created for this purpose. A global framework model is combined with volume models in the area of the bonded connections in order to determine the local stress of the bond. It is shown that both highly rigid and elastic adhesives can be used due to the design of the connections. In the next step, suitable, commercially available 2-component adhesives are selected on the basis of the boundary conditions and requirements. These are characterised experimentally. Based on the results, two adhesives are then prioritised in coordination: a highly rigid 2-component polyurethane adhesive and an elastic 2-component adhesive based on EP-PU hybrid. Publication date: January 2021 Authors: Dr.-Ing. M. Albiez, J. Damm, M.Sc., Prof. Dr.-Ing. T. Ummenhofer, Dipl.-Wirt.-Ing. S. Myslicki, Dr. T. Vallée, H. Ehard, M. Eng., Prof. Dr.-Ing. Ch. Schuler
available anytime
View details →€30.00
excl. VAT
 FOSTA
P 1121 - Development of a method for the design of bonded joints in structures subject to vibration in agricultural machinery and plant engineering
P 1121 - Development of a method for the design of bonded joints in structures subject to vibration in agricultural machinery and plant engineering In constructions made of thicker steel sheets (approx. 3-8 mm) in agricultural machinery and plant engineering, adhesive bonding technology has so far only been used to a limited extent, although it is already an established joining method in other areas of application. Bonded joints are generally characterised by excellent behaviour under vibration load, which was also demonstrated on thicker steel sheets in a previous SME study by FOSTA e.V. in random sample tests. The main objectives of the project are - Experimental investigation of the strength behaviour of bonded joints made from thicker thicker sheets using higher-strength steels. Comparison of the strength behaviour of bonded and welded joints, - Development of a procedure for the design of bonded joints under cyclic loading as an cyclic loading as an alternative to welded joints. For this purpose, the joint and seam forms of welded construction details commonly used in agricultural machinery and plant engineering are analysed at the beginning and evaluated with regard to the feasibility of adhesive bonding solutions. A bracket connection is selected as a bonded sample component for subsequent investigations. At the beginning of the research project, the strength behaviour is examined in quasi-static, Wöhler and fatigue strength tests using the example of a lap joint suitable for adhesive bonding technology without and after exposure to media or corrosion. It is shown that bonded joints under quasi-static loading fall significantly short of the strength of the welded joints investigated. However, the strength of the bonded joints can be increased by using higher-strength adhesives. The potential of bonded joints lies in the high-cycle fatigue range. Due to the significantly lower notch effect, the fatigue behaviour above approx. 105 to 106 load cycles is much more favourable compared to welded joints. The influence of medial and corrosion effects must always be taken into account, i.e. seam seals are required in zones subject to greater stress in this respect. The high resistance to fatigue identified at the lap joint is also evident in the sample components analysed, provided the joint zones are sufficiently rigid. The lightweight construction potential of bonded high-strength steels is clearly demonstrated by the fact that a reduction in sheet thickness has a significantly lower impact on the service life compared to welded joints. To ensure handling strength in production, mechanical processes accessible from one and two sides (blind rivets, etc.) are analysed and evaluated. Finally, recommendations for the methodological procedure for the development of structural adhesive bonds for agricultural machinery and plant engineering are formulated from the project results. Based on the data obtained, a concept for determining the component S-N curve and the component fatigue strength using nominal shear stresses in accordance with the FKM guideline is presented. Publication: 2019 Authors: Prof. Dr.-Ing. G. Kötting, Prof. Dr.-Ing. G. Meschut
available anytime
View details →€30.00
excl. VAT
 FOSTA
P 1118 - Influences of steel and composite construction on the life cycle costs and marketability of multifunctional office and commercial buildings
P 1118 - Influences of steel and composite construction on the life cycle costs and marketability of multifunctional office and commercial buildings Demographic change and increasing sustainability awareness are examples of changing social conditions that have an impact on the user requirements for multi-storey buildings. Resource conservation, recyclability, life cycle costs and value retention, even under changing property conditions, are increasingly at the centre of planning. The competitiveness of rental and usable space depends, among other things, on whether the spatial structures offer the necessary flexibility to adapt to these dynamic processes. Experience in recent decades has shown that the construction of low-cost monofunctional building structures and urban districts, as has been the case in many places since the 1970s, often leads to premature vacancies and even demolition, as the primary structure is not sufficiently adaptable. The aim of the research project was to develop multifunctional building structures and to utilise the potential of steel and composite construction. This should increase the long-term marketability and sustainability of the properties. The subject of the research report is firstly an analysis of the current situation of the property market and the causes of structural vacancy. This is followed by a presentation of revitalisation projects that have already been carried out and a summary of the findings for property planning. The basics of the sustainability assessment of buildings and building elements as well as the assessment methods used in the project are presented in the second chapter. Based on the findings from previous revitalisation projects, Chapter 3 develops recommendations for the property planning of multifunctional buildings. The requirements of different types of use, such as clear storey height, building depth or access, are summarised. The requirements of variable building structures result from the overlapping of these aspects. These are illustrated using designs of reference buildings with different degrees of variability. Building on the property planning requirements, Chapter 4 derives the design implications resulting from multifunctional utilisation. The properties of classic and multifunctional ceiling systems in composite construction as well as the influences of fire protection, façades and building foundations are analysed. The ecological, monetary and functional influences of the various building components are assessed in parameter studies. The effects of increased variability and the extension of the service life are analysed using the reference building as an example. Chapter 5 analyses the market segments relevant to the research project and their development. Furthermore, the utilisation type-specific revenues and monetarily assessable risks are determined. The investigations form the basis for stochastic scenario analyses, through which a statement can be made on the fluctuation range of the forecast costs, revenues and defined target figures. Building on this, Chapter 6 uses the example of the reference buildings to determine the expected returns based on the return on equity for various conversion scenarios. The effects of the individual input parameters are analysed in sensitivity analyses. The analyses carried out show that suitable planning precautions can increase the variability of building structures and enable a variety of uses. The steel and composite construction method with efficient load-bearing structures allows the adaptability of buildings without significantly increasing the ecological or monetary costs of construction. If the extension of the life cycle is created by the increased variability, there are clear advantages. Ultimately, the profitability analyses show that a higher initial investment leads to a long-term increase in returns and a reduction in the risk of vacancy in many scenarios. Publication: March 2020 Authors: Prof. Dr.-Ing. Richard Stroetmann, Dipl.-Ing. Lukas Hüttig, Prof. Dipl.-Ing. Johann Eisele, Dipl.-Ing. Architect Benjamin Trautmann, Prof. Dr.-Ing. Dipl.-Wirt.-Ing. Jens Otto, Dipl.-Ing. Anne Harzdorf, Dipl.-Ing. Cornell Weller
available anytime
View details →€30.00
excl. VAT
 FOSTA
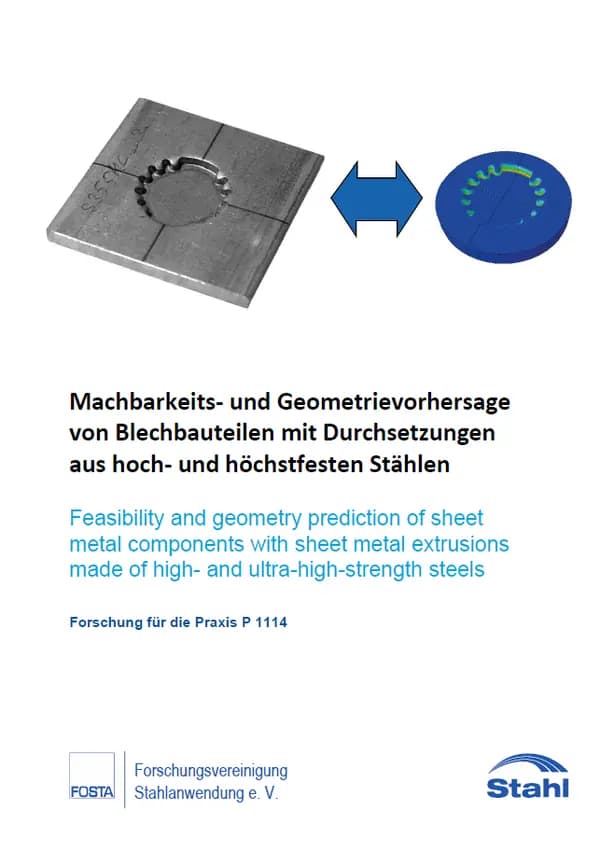
P 1114 - Feasibility and geometry prediction of sheet metal components with high and ultra-high strength steels
P 1114 - Feasibility and geometry prediction of sheet metal components with high and ultra-high strength steels Reducing manufacturing costs is a key factor in increasing the competitiveness of manufacturing companies. In this context, clinching offers great potential, as this process makes it possible to produce functional surfaces in just one production step and without post-processing. Push-through forming is defined in DIN 8587 as a shear forming process in which one workpiece part is displaced relative to another with a rectilinear tool movement. The plastic deformation is achieved, analogous to fine blanking or shearing shear cutting with a small cutting gap, plastic deformation is mainly caused by a state of shear stress. The tool technology and tool kinematics of the processes are also similar. This leads to the conclusion that piercing largely corresponds to a cutting process without cutting through the workpiece. In order to reduce the weight of components and to be able to dispense with a tempering process, sheet metal made of high-strength and ultra-high-strength steel is increasingly being used. However, there is hardly any experience in the design and development of these grades. In order to ensure the safety of the process in the early development phase the process is simulated using the finite element method. This poses particular challenges in terms of material modelling. It is known from shear cutting that the temperature in the shear zone can rise to over 300 °C. Furthermore, degrees of deformation and strain rates are to be expected that cannot be modelled using conventional experiments such as the tensile test. In order to reduce the experimental effort, a methodology is presented and validated in this research project in order to nevertheless enable an efficient prediction of the geometry and feasibility of a sheet metal component with through-set. For this purpose, the interleaving line is broken down into recurring mould elements. The characteristic shape of these interspersions is determined experimentally for four different sheet metal materials. materials. Subsequent material modelling based on a simple test procedure is used as the starting point for determining the correction model. This is followed by an adjustment of this model in order to minimise the deviation between simulation and experiment. By interpolating between the mould elements, it is possible to adapt the material model locally for complex interspersion geometries. This makes it possible to assess the feasibility and geometry of interspersions made of high-strength and ultra-high-strength steels at an early stage of development. Authors: Prof. Dr.-Ing. W. Volk, J.-M. Stahl M.Sc. Publication: March 2020
available anytime
View details →€30.00
excl. VAT
 FOSTA
P 1112 - Statistical validation of small batches in steel processing
P 1112 - Statistical validation of small batches in steel processing The research project "Statistically safeguarding small series in steel processing" focussed on the development of a concept for the introduction of statistical process control (SPC) in small series production. The focus was on the steel processing value chain. The particular potential of the concept includes a sustainable increase in product quality and a reduction in scrap and quality costs. The basic approach for the concept development was the development of a similarity model for the expert-based grouping of small series on the basis of similar quality characteristics and processes with the help of a suitable classification and coding system. By analysing entire small series groups within the framework of statistical process control, it is possible to increase the number of available samples and thus also the statistical reliability. The latter can be quantified using a developed risk model. The quantified certainties provide a basis for describing similarities between small batch groups and their small batches. In addition, a similarity measure can be derived that can be used to evaluate the small series groups formed. The implemented KleiSta software demonstrator makes it possible to visualise the group samples in the context of adapted interactive quality control charts and calculates the statistical certainties for various quality statements as well as the similarity measures. The Fraunhofer Institute for Production Technology IPT developed the concept and the KleiSta software demonstrator as the executing research centre and project coordinator during the project period from 1 September 2015 to 31 August 2017 in close cooperation with a project support committee consisting of the following 14 manufacturing companies (small, medium-sized and large companies) and with the Forschungsvereinigung Stahlanwendung e.V. (FOSTA): - 3win Maschinenbau GmbH - ArcelorMittal Ruhrort GmbH - ASK GmbH - Bittner Werkzeugbau GmbH - EZM Edelstahlzieherei Mark GmbH - Innolite GmbH - Krott & Heuter GmbH - Leistritz Turbomaschinen Technik GmbH - Lemken GmbH & Co KG - Ortlinghaus-Werke GmbH - Phiesel GmbH - Rolls-Royce Germany Ltd & Co KG - Saarstahl AG - Ziehwerk Plettenberg GmbH & Co KG I n the course of the research project, regular committee meetings and topic-specific workshops provided a platform for the participating companies to define individual requirements for the concept and the KleiSta software demonstrator as well as suitable small series products and processes for the application of statistical process control. Individual meetings were also held to identify and compile available data that could be used for initial sample analyses and subsequent validation. Further information on the project can be found on the website www.kleista.de. Publication: 2018 Authors: K. Kostyszyn
available anytime
View details →€30.00
excl. VAT
 FOSTA
P 1110 - Localised laser heat treatment of work-hardened steels to improve forming and functional properties for lightweight construction in the automotive industry
P 1110 - Localised laser heat treatment of work-hardened steels to improve forming and functional properties for lightweight construction in the automotive industry The overarching research objective of the project was to use a combination of cold rolling and local laser heat treatment to achieve customised properties in steel blanks with regard to formability and crash behaviour for the subsequent forming process and later use in the automobile. To investigate this approach, a cost-efficiently producible ferritic steel, the micro-alloyed S550MC, and an established steel with high application relevance, the dual-phase steel HCT780X, were selected. Firstly, the temperature ranges in which relevant softening mechanisms occur depending on the degree of rolling were determined. For this purpose, short-term heat treatments similar to laser softening were carried out in a forming dilatometer and the resulting mechanical properties were then tested in a tensile test at room temperature. The results serve on the one hand as a target value for the process development of localised laser heat treatment and on the other hand as a basis for the material data required in the simulation. In deep-drawing simulations of a work-hardened cross-section, softening strategies for maximising the drawing depth were developed, while in crash simulations of a hexagonal hollow profile, softening strategies for increasing the energy absorption were determined. The most promising strategies were verified in real tests and the methodology developed was validated using a sample component, a B-pillar. The results of this interdisciplinary collaboration prove that the design and optimisation of local heat treatment areas is possible in principle using simulation. To increase the formability, it is most effective if potential failure areas are work-hardened and surrounding areas are softened to enable flow. The improvement in crash behaviour can be demonstrated in drop tower tests: Crash boxes produced using the process combination exhibit an up to 28% shorter compression path compared to a conventional crash box with the same energy absorption. The production of the sample component shows that process limits can also be predicted with the aid of simulation. When integrating local laser heat treatment into the sheet metal forming production chain, straightening to minimise the resulting distortion and the removal of the laser-induced oxide layer before galvanising to ensure corrosion resistance must also be taken into account. A scanner and special optics with a customised beam profile were tested to increase the feed rate of the laser irradiation. The combination of cold rolling to increase strength and laser heat treatment for localised softening revealed new potential for lightweight construction and crash safety. According to the results, the potential of the investigated process combination can be rated as high. Publication: 2018 Authors: Prof. Dipl.-Ing. G. Hhirt, Prof. Dr rer. Nat. R. Poprawe
available anytime
View details →€30.00
excl. VAT
 FOSTA
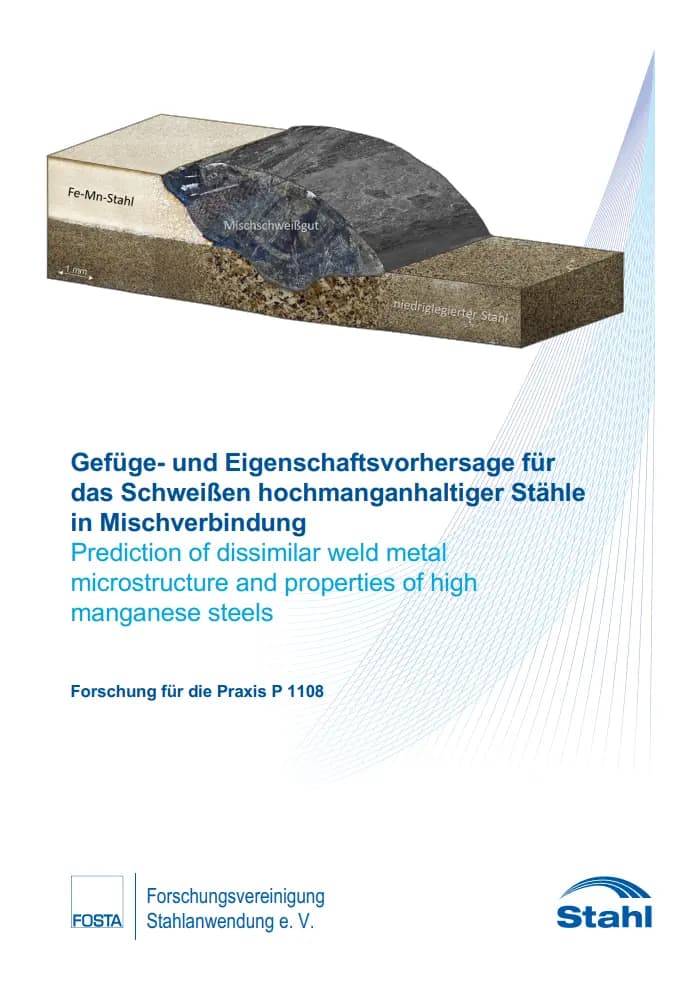
P 1108 - Microstructure and property prediction for welding of high manganese steels in dissimilar joints
P 1108 - Microstructure and property prediction for the welding of high-manganese steels in dissimilar joints The primary aim of the research project was to improve the welding processing of high-manganese steels in dissimilar joints by predicting the microstructure and properties of the dissimilar weld metal using a newly developed constitution diagram. Three economically relevant Fe-Mn steels with different alloying concepts were used as test materials. The steels HC340LA (1.0548) and 22MnB5 (1.5528), which are widely used in car body construction, were used as joining partners. Various high-manganese metal powder flux-cored wire electrodes were also available. Using a TIG arc melting furnace, a remelting method was developed for experimental weld metal simulation, which makes it possible to produce mixed weld metals of any material combination in defined mixing ratios under MSG-adequate cooling conditions. Using this method, a large number of remelting samples (dissimilar weld metal) were produced in a wide range of different chemical compositions, which were characterised in terms of microstructure type, microstructure proportions, hardness and ferrite number. A total of eight microstructure groups were determined, which can occur in the mixed weld metal depending on the material combination and mixing. The different martensite types ε and α' are of particular importance, as these cannot always be clearly distinguished metallographically, but differ significantly in their properties. The results show that the paramagnetic ε-martensite mainly occurs in dissimilar weld metal with a relatively high Mn content. The α'-martensite, on the other hand, is found in dissimilar weld metals with lower Mn contents, i.e. with higher admixtures of low-alloy ferritic or martensitic joining partners or when using low-alloy filler metals. A high hardness in the dissimilar weld metal investigated here is directly associated with the formation of α'-martensite, which is why it is essential to differentiate between the two types of martensite. Investigations into the influence of the cooling rate showed that a significant increase in the cooling rate only has a significant influence on the microstructure and hardness in a few mixing ratios. This applies in particular to dissimilar weld metals with a very high admixture of low-alloy ferritic or martensitic joining partners or low-alloy filler material. It can therefore be assumed that very similar microstructural states and hardness values can be expected in the dissimilar weld metal in welding processes with higher cooling rates than in MIG welding (assuming homogeneous mixing). On the basis of the experimentally simulated dissimilar weld metals and the weld metal properties determined from them, a comprehensive data set was recorded, with the help of which equivalents were derived using statistical evaluation methods, which span the axes of the newly developed constitution diagram, the so-called COHMS diagram. In addition to the microstructure prediction in MSG weld metals, the COHMS diagram enables a rough estimation of the resulting weld metal hardness on the basis of HV-ISO lines. validation of the COHMS diagram using real MSG welds resulted in a very good prediction accuracy. 89 % of the MSG weld metals were predicted correctly. The remaining 11 % were close to the limit lines. The investigations into the influence of the microstructure type - in particular the martensite content - in the mixed weld metal on the mechanical-technological properties of the welded joints showed that a weld metal microstructure of austenite + α'-martensite in particular is to be regarded as extremely critical. The tested joints with this weld metal microstructure exhibited significantly poorer strength values under both static and dynamic impact loads compared to the other welds and predominantly failed in the weld metal Publication: September 2019 Institute of Materials and Joining Technology at Otto von Guericke University Magdeburg Prof. Dr.-Ing. Sven Jüttner M. Sc. Benjamin Wittig Dr Manuela Zink Participating companies: ArcelorMittal Global R&D, Zelzate Benteler Steel/Tube GmbH, Paderborn CIF GmbH, Grünstadt Corodur Verschleiss-Schutz GmbH, Thale Dr Rosert RCT GmbH, Dresden Kirchhoff Automotive Deutschland GmbH, Attendorn MSS Magdeburger Schweißtechnik GmbH, Barleben MSZ GmbH, Blankenburg Outokumpu Nirosta GmbH, Krefeld Salzgitter Mannesmann Forschung GmbH, Salzgitter thyssenkrupp Hohenlimburg GmbH, Hagen Volkswagen AG, Wolfsburg Vorrichtungsbau Giggel GmbH, Bösdorf Research institution(s): Institute for Materials and Joining Technology at Otto von Guericke University Magdeburg Responsible for FOSTA - Forschungsvereinigung Stahlanwendung e. V. Dipl.-Ing. Rainer Salomon
available anytime
View details →€20.00
excl. VAT
 FOSTA
P 1105 - Determination of the influence of processing and environmental hydrogen sources on the tendency of high-strength steels to hydrogen-induced cold cracking
P 1105 - Determination of the influence of processing and environmental hydrogen sources on the tendency of high-strength steels to hydrogen-induced cold cracking A challenge in the welding processing of high-strength fine-grained structural steels is the risk of hydrogen-induced cold cracking (HIC). There is a general consensus that HIC is particularly likely to occur with a critical combination of hydrogen content, hardening structure and stress state. The influence of individual process parameters on hydrogen absorption during welding has already been investigated in the past. However, the different process boundary conditions, such as those that occur during construction site production, were often not taken into account, making the risk of cold cracks occurring in practice almost impossible to predict. As part of this project, various high-strength fine-grained structural steels (primarily structural steel S690QL and pipeline structural steel L555MB and X80) are therefore being investigated with regard to their sensitivity to hydrogen (embrittlement, cracking) in connection with welding processing in the MSG and submerged arc processes, whereby the processing conditions are specifically varied and taken into account. The combination of all the results obtained in the project should serve as a basis for estimating the material and processing-specific cold cracking tendency. The experimental test series are supplemented by numerical simulation approaches. For both welding processes, dependencies of the welding processing and environmental conditions, e.g. through variation of the welding parameters or targeted manipulation of the potential hydrogen supply, on the resulting hydrogen content in the weld metal could be worked out and quantified. The findings will be used to produce joint welds on sheets of the high-strength test materials. No cold cracks are detected under controlled conditions due to the consistently high heat content during welding in multi-layer technology and the resulting favoured hydrogen effusion in the area of the welding zone. On the basis of tensile tests with a low strain rate (slow strain rate tests, SSRT), however, clear hydrogen-related influences can be recognised. In these tests, samples are taken from the unaffected base materials and from joint welds (GMAW and SAW) at various positions and tested. In particular, additional galvanostatic hydrogen loading during the SSRT test leads to a considerable loss of elongation as a result of hydrogen embrittlement, whereby specific differences arise here depending on the materials, the welding processing conditions and the sampling position. By carrying out self-loading cold cracking tests (Tekken), the tendency to cold cracking can also be qualitatively estimated as a function of the selected preheating temperature and the energy of the line in order to narrow down the welding processing window. Publication: 2020 Authors: R. Sharma M.Sc., Dr.-Ing. Ch. Haase
available anytime
View details →€30.00
excl. VAT
 FOSTA
P 1101 - Innovative overhead line pylons for the energy transition, taking into account design, technical and economic aspects
P 1101 - Innovative overhead line pylons for the energy transition, taking into account design, technical and economic aspects The politically driven energy transition requires numerous expansion and grid reinforcement measures. For overhead line masts made of steel, lattice masts are still used almost exclusively, which were already manageable 100 years ago in terms of planning, production and calculation. Today, these are often seen as a visual disturbance or detriment to the aesthetics of the landscape and the townscape. This research project aims to improve the image of overhead power lines and make them a necessary and accepted part of our industrial society. The aim is to develop a new type of steel overhead line mast that not only fulfils the highest technical and economic requirements but also meets the design requirements of the energy transition. The work was therefore carried out by an interdisciplinary team of engineers and architects. This research report first presents the basic principles of overhead line construction as well as the electrical and mechanical requirements for the development of the pylon design. Based on this, various optimisation approaches developed for the lattice tower construction are presented. For the development of the innovative shape for the overhead line mast, four variants of the overhead line mast designs are explained and the detailed investigations in the form of FE analyses of the favoured variant are presented. The experimental approach is then used to analyse the load-bearing behaviour of the innovative pipe-in-pipe press connection. All of the developments are incorporated into the profitability analysis of the innovative design, taking series production into account. As part of the investigations, an attractive and economical alternative to the previous lattice mast constructions was created. The objective of the research project was thus achieved. Publication: March 2020 Participating companies: IHT Ingenieur-, Hoch- und Tiefbau GmbH J.J.Brühl Stahlbau GmbH & Co KG KINA Ingenieurgesellschaft GmbH OCAS N.V. Poetsch GmbH CNC turning and milling PSP - Prof. Sedlacek & Partner R. Lange GmbH Salzgitter Mannesmann Forschung GmbH SSF Ingenieure AG Stahlbau Raulf GmbH thyssenkrupp Steel Europe AG Vallourec Germany GmbH
available anytime
View details →€40.00
excl. VAT