
FOSTA
As part of the project, the effects of cryogenic treatment on the microstructure, mechanical properties and wear resistance of the high-alloy tool steels X38CrMoV5-3 (electroslag remelting process (ESR)), X153CrMoV12 …
As part of the project, the effects of cryogenic treatment on the microstructure, mechanical properties and wear resistance of the high-alloy tool steels X38CrMoV5-3 (electroslag remelting process (ESR)), X153CrMoV12 (powder metallurgy (PM) and fusion metallurgy (SM)) and ~X190CrVMo20-4 (PM) were investigated. The tempering parameters of the samples for the mechanical tests and those of the wear samples were selected on the basis of the tempering curves so that a similar hardness was present for both the conventionally heat-treated and the cryo-treated samples. Although a finer, martensitic microstructure and a more homogeneous distribution of secondary carbides in the X38CrMoV5-3 was achieved by including a cryogenic treatment in the conventional heat treatment or an increased amount and a more homogeneous distribution of secondary and nano carbides in the X153CrMoV12 and ~X190CrVMo20-4 steels could be attributed to the cryogenic treatment, no differences were found in the mechanical properties and in various wear tests (sandpaper method, wear cup and cavitation erosion).
The wear resistance of the high-alloy tool steels depends to a large extent on the primary carbides and the macro hardness, less on the secondary or nano carbides. Both cryo-treatment and tempering three times at high temperatures achieved an almost complete conversion of the retained austenite into martensite in the small samples. Cryogenic treatment of tool components with large wall thicknesses would have a positive effect, as a uniform and complete transformation of the retained austenite is achieved over the entire cross-section. This allows the user to better assess the cryogenic treatment technology and thus utilise it in a more targeted manner, thereby achieving improved results or saving costs.
Machine-translated title and description. The document itself is in German.
Payment by card (Stripe) or invoice (DE, AT, CH). Download link by email: automatically after ordering by card, after order approval for invoice (valid for 30 days). Terms
Digital download
Other parts and editions as well as neighbouring documents of the same series.
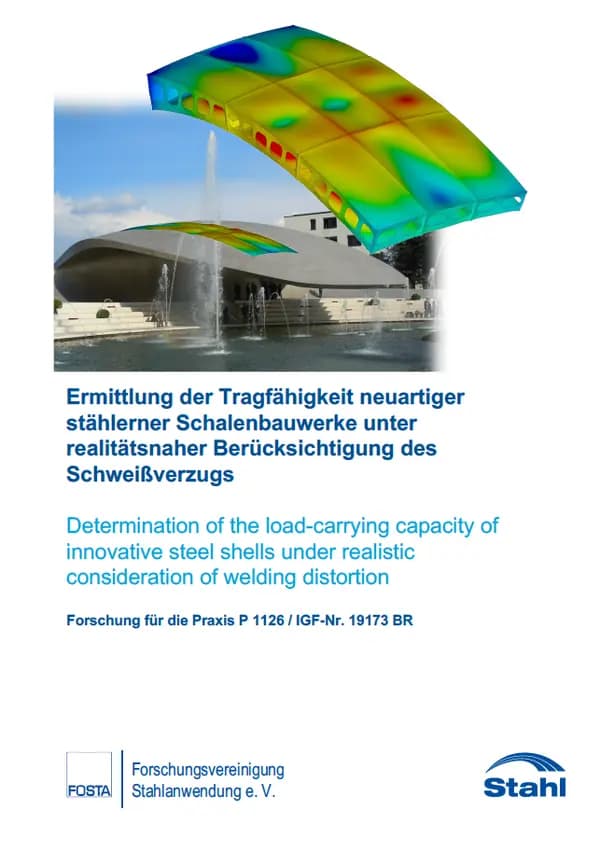
P 1126 - Determination of the load-bearing capacity of novel steel shell structures under realistic consideration of welding distortion Recently, stiffened shell structures (so-called monocoque) have been increasingly used in steel construction. Due to the slender construction methods, buckling is a limit state that must be taken into account. A geometrically and materially non-linear analysis of the imperfect shell structure (GMNIA) has the highest theoretically achievable degree of reality. Its verification quality depends crucially on whether the imperfections introduced into the calculation model describe the effect of the imperfections of real structures equivalently. In principle, it is now possible to reliably predict the effects of the welding process using welding simulation. The analytical-numerical hybrid model developed at the LFT offers a practice-relevant methodology for the welding simulation of large components. From a design perspective, an interface to the welding simulation is to be realised and subsequently verified. The aim of the project was to provide a robust and reliable calculation method for a numerically supported GMNIA verification of welded shell structures. In contrast to previous approaches, this is the first time that this has been done directly using hybrid approaches to capture the influences of the welding process. The analytical numerical hybrid model was used to calculate the welding imperfections. In order to be able to use the model to calculate the welding imperfections that occur when welding curved structures in space, the underlying analytical model had to be extended. Based on numerical variation calculations, an acquisition function was derived that takes into account the curvature in space and the resulting reduced stiffness. The hybrid model has already been successfully applied to a large number of differently complex components. However, the focus was on welding distortions. Little attention has been paid to the localised stress state in the near-seam area. However, it influences the load-bearing behaviour of welded components. Both the verification of the stresses calculated using the hybrid model with the results from thermomechanical calculations and the validation with radiographic measurements showed good agreement. Only a new meshing strategy was developed to improve this. Since in most cases the stiffeners are welded on both sides, an influence function was derived based on the source method, which takes into account the intermediate time between the two welds and records its effect on the plastic strains. Publication: August 2020 Authors: Prof. Dr.-Ing. habil. H. Pasternak, Dr.-Ing. Ch.Stapelfeld, Dr.-Ing. Launert, Prof. Dr.-Ing. habil. V. G. Michailov, Dr.-Ing. N. Doynov, C. A. Kaya
available anytime
€30.00
excl. VAT
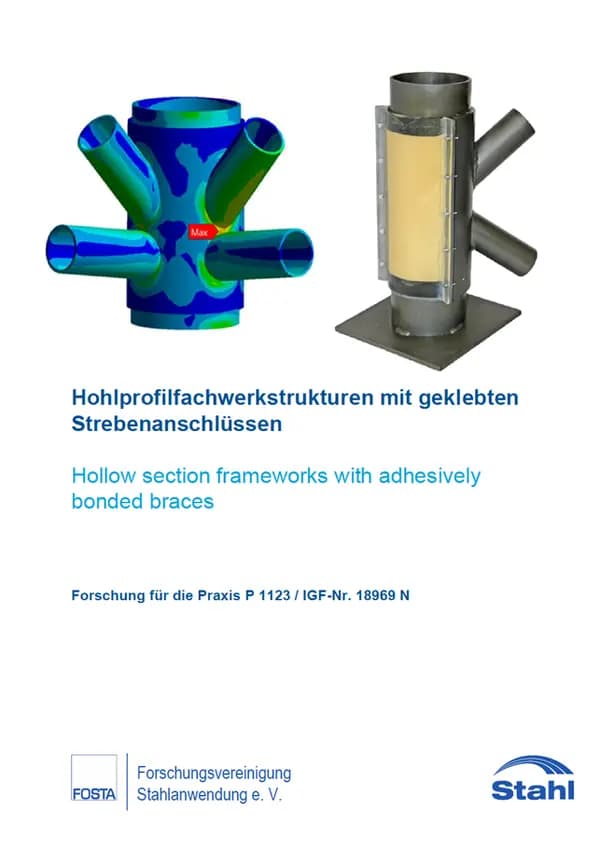
P 1123 - Hollow section truss structures with bonded strut connections Foundation structures for offshore wind turbines are often designed as jacket truss structures for water depths of more than 20 metres. Until now, the individual hollow profiles of these truss structures have been joined by welding. Due to the spatial intersection of the pipe profiles at the junctions and the resulting complex weld seam geometries, as well as the large open areas required for final assembly, this represents a major manufacturing effort. An innovative hybrid connection of the struts to the corner posts of these supporting structures is the focus of this research project. The concept combines the joining methods of bonding, welding and bolting by forming nodal partial shells at the ends of the struts. These individual partial shells are formed in such a way that they enclose the corner strut and are completed to form a complete shell during assembly. After the individual partial shells have been bolted together, the remaining gap between the gusset ring shell and the corner post tube wall is joined using adhesive technology. This work step takes place in the manufacturing plant and therefore under defined ambient conditions. This design has the advantage that permanently acting static loads (such as dead weight) are almost completely dissipated by the continuous corner stems. Furthermore, the lack of welded connections on the corner posts results in an increase in local fatigue strength. In addition, the hybrid connection enables prefabrication of the struts and the modular design of the jacket. First, the requirements and boundary conditions of the jacket support structure are analysed and defined in the research project. In close cooperation with companies from the offshore wind energy sector, the stresses from wind, wave impact and turbine operation are determined. Real climate data measured on research platforms in the North Sea is also analysed and the requirements for the adhesive bond are derived from this. Due to the dimensional tolerances of the bonded parts, thick-film bonds of up to 25 mm are required. Extensive numerical investigations are used to analyse the stress on the bonded joint and steel structure. Numerical models of the entire jacket support structure are created for this purpose. A global framework model is combined with volume models in the area of the bonded connections in order to determine the local stress of the bond. It is shown that both highly rigid and elastic adhesives can be used due to the design of the connections. In the next step, suitable, commercially available 2-component adhesives are selected on the basis of the boundary conditions and requirements. These are characterised experimentally. Based on the results, two adhesives are then prioritised in coordination: a highly rigid 2-component polyurethane adhesive and an elastic 2-component adhesive based on EP-PU hybrid. Publication date: January 2021 Authors: Dr.-Ing. M. Albiez, J. Damm, M.Sc., Prof. Dr.-Ing. T. Ummenhofer, Dipl.-Wirt.-Ing. S. Myslicki, Dr. T. Vallée, H. Ehard, M. Eng., Prof. Dr.-Ing. Ch. Schuler
available anytime
€30.00
excl. VAT
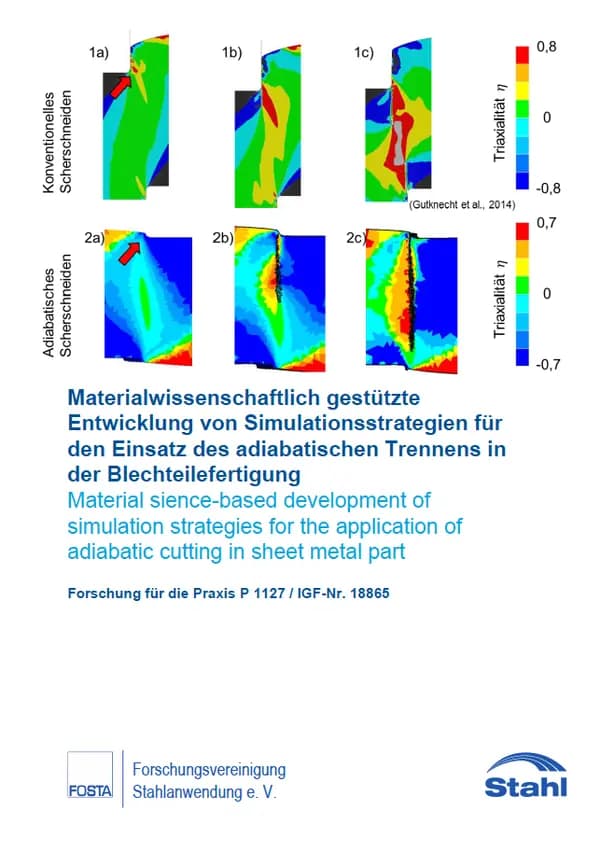
P1127 - Materials science-based development of simulation strategies for the use of adiabatic cutting in sheet metal part production In order to reduce the amount of material used and at the same time pursue the concept of lightweight construction, high-strength steels with tensile strengths greater than 1000 MPa are increasingly being used in automotive engineering. Practically every sheet metal component undergoes a trimming operation during the manufacturing process. However, conventional shear cutting or fine blanking cannot be used for ultra-high-strength steels, or only at great expense in terms of pre- and post-treatment. Here, adiabatic shear cutting offers an alternative to conventional shear cutting or cost-intensive laser trimming. It has already been shown that this process has a high quality in terms of straightness, roundness and surface finish of the shear-cut edge. However, for the industrial use of adiabatic shear cutting, there is a lack of fundamental investigations for relevant high-strength steels, such as frequently used press-hardening steels. Furthermore, the microstructural processes occurring during adiabatic shear cutting and their effect on technological properties have not been described for these steels. Basic approaches for estimating the necessary process energy, process speed and a classification regarding the suitability of the materials to be used are also lacking. The aim of the project is to answer these open questions and to close the gap to industrial application by means of a fundamental characterisation of the process. Furthermore, a methodology for the simulation of the strongly temperature- and strain rate-dependent process is required. Extensive material characterisation tests (temperatures up to 1000 °C and strain rate ?̇ up to 1000 1/s) were carried out to achieve the objectives. Tensile tests with notch geometry were used to determine the failure behaviour. A total of three different steel grades were analysed. Based on these investigations, numerical and analytical models were developed to estimate the locally generated temperature and the process energy required to perform the separation operation. Adiabatic shear cutting tests were carried out to produce cylindrical components and various demonstrators (rectangular plates with rounded edges). Furthermore, it was shown that two of the investigated steels (20MnB5 and C75S), despite almost similar mechanical properties at room temperature under quasi-static load, showed significant differences during adiabatic cutting. In particular, it was shown that the strain rate sensitivity of the steels has a major influence on the initiation and formation of adiabatic shear bands, but at the same time the required process energy is also strongly influenced by this factor. Using finite element simulations, the resulting characteristic shape of the shear-cut surfaces could be predicted with a high degree of accuracy. The methods developed can be used for process design. Publication: May 2020 Authors: Prof. Dr.-Ing. A. E. Tekkaya, Dr.-Ing. T. Clausmeyer, Dipl.-Ing. D. Staupendahl, F. Schmitz M.Sc., Univ.-Prof. Dr.-Ing. habil. M. F.-X. Wagner, Dipl.-Ing. S. Winter
available anytime
€30.00
excl. VAT
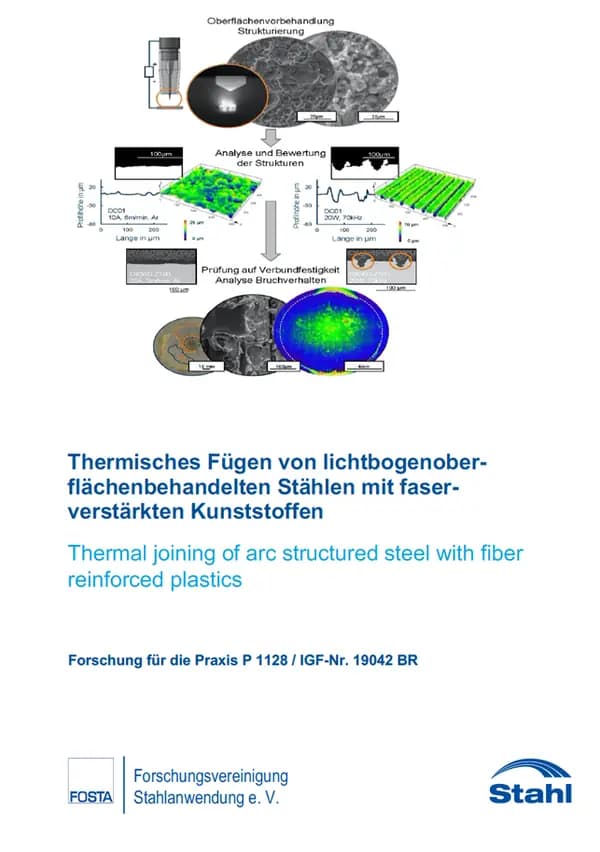
P 1128 - Thermal joining of arc surface-treated steels with fibre-reinforced plastics The thermal joining of metallic and polymer materials offers advantages over mechanical joining processes and bonding. In order to achieve sufficient adhesive strength, it is advantageous to increase the surface area of the metallic joining partner. Beam or laser processes are mainly used for this purpose. The surfaces produced are evaluated by determining geometric parameters, but also by wettability tests. Depending on the material and structuring process, adhesion strengths of between 5.2 MPa and 43 MPa could be researched in the available literature. Surface structuring using electric arcs has hardly been documented to date. The structures produced are highly irregular and it is not known to what extent existing methods can be used for surface evaluation. The aim of the project was to structure metallic surface structures using conventional arc technology. The surface-treated metals are used to produce hybrid metal-plastic composites. Laser structures were generated in continuous wave (cw) and pulsed mode as a reference for the arc structure. The focus of the investigations was the characterisation of the generated structures with regard to their topographical and energetic properties as well as their effects on the wetting and the resulting fracture behaviour. The investigations were initially carried out on model point-shaped tests to determine the tensile strength for different material pairings. The results were then transferred to industrial joining geometries (linear tests). In addition to the materials mentioned, fibre-reinforced thermoplastics were also used. The knowledge gained is intended to contribute to current research into new joining processes for hybrid material composites. The process parameter analysis for the creation of laser-structured surfaces in pulsed and cw laser operation shows clear differences in the achievable structural shapes. Using the cw process, mainly deep structures can be produced. The number of passes is decisive for the geometry of the resulting pattern. From a number of passes of i = 2, a drop-shaped pattern with undercuts is produced. Pulsed laser radiation can be used to create wide, flat structures with low pulse frequencies (f = 20 kHz). As the pulse frequency increases (f = 60 - 70 kHz), drop-shaped structures can be produced due to the resulting pressure. Publication: January 2021 Authors: M.Sc. M.-L. Solf, Dr.-Ing. K. Schricker, Univ.-Prof. Dr.-Ing. habil. J. P. Bergmann, Dipl.-Ing. M. Lohse, Dr.-Ing. M. Hertel, Prof. Dr.-Ing. habil. U. Füssel
available anytime
€30.00
excl. VAT
Payment by card (Stripe) or invoice (DE, AT, CH). Download link by email: automatically after ordering by card, after order approval for invoice (valid for 30 days). Terms