 FOSTA
P 1020 - Practice-oriented welded joints of high-strength steels - Further development of the design rules and process optimisation taking into account the deformation capacity
P 1020 - Practice-oriented welded joints of high-strength steels - Further development of the design rules and process optimisation taking into account the deformation capacity Due to various residual reductions in the design and execution of steel and plant structures, the economic use of high-strength structural steels in this area is only possible to a limited extent. The aim of the research project was therefore to create a basis that would lead to a significant improvement in the conditions of use of higher-strength steels in welded joints. The need to improve the technical rules for design and execution arose for a number of other reasons. For example, the permissible weld seam stresses for matching and overmatching joints are defined too conservatively for many joint shapes and combinations of base and filler material. The correlation coefficient βw was defined for the most unfavourable case in which flank fillet welds are subjected to parallel shear. For a large proportion of welded joints, however, it is not necessary for the strength of the base material to be reached or even exceeded. This applies, for example, to neck welds of welded I and box sections, articulated end plate connections, butt joints in areas of low stress and many other cases. To achieve the research objectives, the mechanical properties of weld seams were systematically analysed using a newly developed small-part test. In addition, the influence of welding-induced energy input on the transformation behaviour and mechanical properties of high-strength steels of different manufacturing processes and steel grades was analysed. Knowledge of the influence of the manufacturing parameters makes it possible to specifically address the respective steels and required weld properties by selecting a suitable matching scenario, welding consumables and process parameters. This creates a basis for manufacturing welded constructions from high-strength steels more economically and with greater process reliability. Extensive experimental and numerical investigations were carried out to develop a modern design model. The new design model is based on a systematic separation of the mechanical properties of the weld seam and the design-related requirements placed on it. As part of the investigations, flank fillet welds of lap joints, face fillet welds of cross joints as well as through-welded and non-through-welded butt joints of different welding consumables and production parameters were analysed. By taking into account the actual properties of the weld seams as a function of the filler metal and the cooling time t8/5 as well as the joint shape, more economical weld seam load-bearing capacities can be achieved. A more economical design allows weld seam volumes and, if necessary, sheet thicknesses to be significantly reduced, which leads to an increase in the economic efficiency of welded constructions made of high-strength steels. Publication date: May 2020 Authors: Prof. Dr.-Ing. R. Stroetmann, Dipl.-Ing. T. Kästner, Dipl.-Ing. L. Werner, Dr.-Ing. A. Hälsig, Dipl.-Ing. S. Neyka, Dr.-Ing. M. Kusch, Prof. Dr. P. Mayr
available anytime
View details →€40.00
excl. VAT
 FOSTA
P 1019 - Derivation of new, improved strength criteria for steel components
P 1019 - Derivation of new, improved strength criteria for steel components The design concept contained in the technical regulations for steel construction is aimed at determining the actual load-bearing capacity of components. The underlying load-bearing capacity functions are usually calibrated using tests. However, purely phenomenological engineering models are used, which link the limit load prediction approximately to the yield strength or tensile strength of the material. This has two decisive consequences: (1) The prediction accuracies of current strength functions are limited because the underlying model concepts do not take into account the actual failure behaviour of the material. The current scatter results from the failure to take into account the actual fracture mechanism and the preceding damage history, which are largely dependent on the actual toughness properties. (2) The use of higher-strength steels and the utilisation of their performance characteristics is significantly restricted, as the setting of high yield strengths for high-strength unalloyed structural steels is only possible at the expense of uniform elongation. However, as the regulations prescribe minimum values for uniform elongation and yield strength ratio without taking into account the special failure behaviour of high-strength steels, these steel grades are often unjustifiably excluded from use. However, the use of high-strength steel grades for steel components promises economic and ecological advantages, for example through cost and energy savings with lower material consumption. An improvement in the strength criteria is therefore definitely worth striving for. In similar projects on the use of pressure vessel steels (FOSTA P 758 and FOSTA P 950), new safety factors for the use of high-strength steels in pressure vessel construction were derived by using new strength criteria that take into account the ductility properties of the material. The core of the methodology was a damage-mechanical investigation of the actual failure behaviour by implementing the phenomenological BAI-WIERZBICKI model (BW) as a crack initiation criterion for failure detection. The damage criterion was based on damage location curves derived by means of simulations with the micromechanically motivated damage mechanics model according to GURSON-TVERGAARD-NEEDLEMAN (GTN). However, the procedure used there cannot be easily transferred to design rules for general steel construction. In the present project, the methodology was therefore transferred to steel components and at the same time a comprehensive investigation of the load-bearing behaviour of modern steels was carried out. The experimental investigations enable the analysis of the actual ultimate load and fracture behaviour as well as the comparison with the design rules of EC3. For individual geometries and steel grades, significant safety reserves were identified in some cases. Furthermore, the tests serve to validate the damage model. This showed that the approach is basically suitable for mapping the failure behaviour, but that there are still difficulties in correlating the model parameters with material parameters due to the dependence on the mesh size. FOSTA - Forschungsvereinigung Stahlanwendung e. V. Publication: April 2019 Authors: Prof. Dr.-Ing. M. Feldmann, Dr.-Ing. S. Schaffrath, Prof. Dr.-Ing. W. Bleck, Prof. Dr.-Ing. S. Münstermann, Dr.-Ing. Brinnel P 1019 / IGF No. 17925 N
available anytime
View details →€30.00
excl. VAT
 FOSTA
P 1018 - Characterisation and modelling of the influence of softening zones on weld spots of ultra-high and high-strength steels under crash load on component behaviour
P 1018 - Characterisation and modelling of the influence of softening zones on weld spots of ultra-high and high-strength steels under crash load on component behaviour In automotive engineering, high-strength steels are increasingly being used in thin sheet thicknesses for lightweight construction reasons in order to increase energy efficiency and passive safety while at the same time conserving resources. Currently and in the future, the established and highly automatable resistance spot welding process will be used to join the individual components made from these high-strength steels to form a load-bearing structure. During spot welding, softening zones form in high-strength steels due to tempering effects, which can jeopardise component integrity. The aim of the research project is to establish a generally valid relationship that describes the reduction in the strength of spot-welded high-strength sheets as a function of the geometric dimensions of the softening zone and the strength mismatch of the joint. The influences of the welding parameters on the formation of the softening zone are investigated and experimentally verified by numerical process simulation of spot welding. Spot-welded joints with geometrically different formation of the softening zone are produced and their influence on the mechanical properties of the welded steel sheet is demonstrated. This is investigated on press-hardened 22MnB5 and on complex-phase steel HCT980C. The KS-2 test technique is used to examine the influence of softening zones on the head tension and shear tension load-bearing capacity of the spot welds. With these tests and the characterisation of the softening zone, modelling recommendations for weld spot replacement models for crash simulation are drawn up and validated by simulating the sample component tests and T-impact tests carried out. The hardness measurements in the cross-section of the spot welds in the high-strength steels HCT1180X, HCT980X and HTC980C show all hardness reductions, i.e. softening zones, next to the spot welds. In tensile and puncture tests with samples that contained spot welds with softening zones in the test area, HCT1180X in particular showed the greatest reduction in strength and elongation at break, while the tensile strength of HCT980C and HCT980X was not reduced, but the elongation at break was significantly reduced. If the crack initiation occurs in the softening zone of a weld spot in component tests with bending and superimposed tensile loading, the crack propagates into the base material under further loading. These results are incorporated into a simulation methodology for the evaluation of crack formation in softening zones. This enables steel users in design and calculation to make statements about the load-bearing capacity of spot-welded constructions made of ultra-high-strength and ultra-high-strength steels. This enables the efficient and economical development of spot-welded components made of ultra-high-strength steels and thus contributes to the qualification of these steels for new spot-welded lightweight components. The IGF project 17991 N of FOSTA -Forschungsvereinigung Stahlanwendung e. V., Düsseldorf, was funded by the Federal Ministry for Economic Affairs and Energy via the AiF as part of the programme for the promotion of joint industrial research (IGF) on the basis of a resolution of the German Bundestag. The project was carried out at the Fraunhofer Institute for Mechanics of Materials IWM, Freiburg, at the Laboratory for Materials and Joining Technology (LWF) at the University of Paderborn and at the Materials Testing Institute MPA, Stuttgart. Publication: 2019 Authors: Dr.-Ing. Silke Sommer, Dipl.-Ing. Lilia Schuster, Prof. Dr.-Ing. Gerson Meschut, Dipl.-Ing. Gökhan Tümkaya, Dr.-Ing. David Hein, Prof. Dr.-Ing. Stefan Weihe, Dipl.-Ing. Fabian Schreyer, Dr.-Ing. Ulrich Weber
available anytime
View details →€50.00
excl. VAT
 FOSTA
P 1016 - Self-pierce riveting of high-strength steel materials in mixed structures using self-clinching self-pierce riveting elements
P 1016 - Self-pierce riveting of high-strength steel materials in mixed structures using self-clinching self-pierce riveting elements The statutory regulations to reduce greenhouse gas emissions are prompting the automotive industry to implement consistent lightweight construction. The reduction of CO2 emissions to an average of 95g CO2/km in passenger car traffic by 2020 has been decided. The vehicle body, which accounts for over 30% of the total weight, offers the greatest potential for implementing lightweight construction, which can be achieved by using high-strength steels and other lightweight materials such as aluminium. In particular, the mixed construction of press-hardened steel and aluminium in combination with adhesive bonding leads to economical lightweight construction solutions. One suitable technology for joining this combination of materials is full-punch rivet bonding. However, full-punch rivet bonded joints lead to gaps between the parts to be joined and thus to poor adhesive bonding, especially when using particularly thin materials for the parts to be joined. The aim of the research project is to develop a modified self-pierce riveting technology for joining high-strength sheet materials with aluminium alloys. This is achieved by modifying the solid self-pierce riveting process so that it works without an embossing ring on the die-side tool. The embossing contour is positioned directly under the setting head of the rivet. Joints produced using the innovative self-clinching self-pierce riveting process should then be characterised by low joining process-related deformations and good adhesive bonding. As part of the research project, geometry optimisations were carried out using simulation, which were validated by experimental investigations. The flexibility of the newly developed process was then determined on the basis of a process analysis. In addition, the joining properties of the process in combination with adhesives were optimised and the property profile recorded as part of investigations into hybrid joining. A joining process was developed with which it is possible to produce efficient and economical joints from 22MnB5 sheets and aluminium sheets in the thin sheet range. Publication: 2017 Authors: Prof. Dr.-Ing. G. Meschut
available anytime
View details →€30.00
excl. VAT
 FOSTA
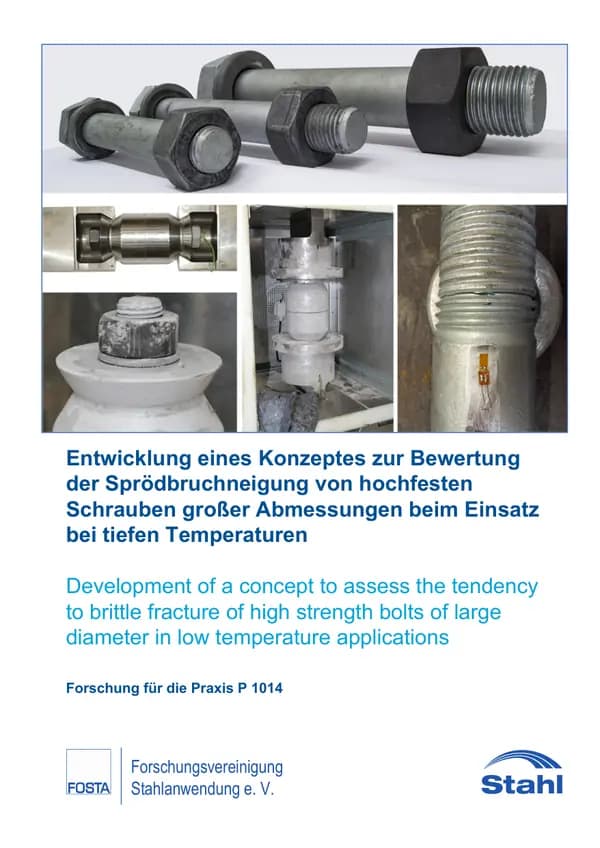
P 1014 - Development of a concept for the evaluation of the brittle fracture tendency of high-strength screws of large dimensions when used at low temperatures
P 1014 - Development of a concept to evaluate the brittle fracture tendency of high-strength bolts of large dimensions when used at low temperatures High-strength HV system bolt assemblies are increasingly being used as prestressed assemblies in large dimensions up to M72 in highly stressed steel structures. In addition to static and cyclical stresses, the connections are also exposed to low temperatures. It is known that the risk of brittle fracture increases with increasing thickness of steel components at low temperatures - in principle, this also applies to larger bolt diameters. In this research project, systematic investigations were carried out into the brittle fracture tendency of high-strength bolts of large dimensions in the diameter range from M24 to M64 at low temperatures. First, the mechanical properties were characterised and the fracture toughness behaviour was described in the form of notched bar impact tests and fracture mechanics tests. The transition temperatures from the notched bar impact test and fracture mechanics test could be correlated with each other using existing correlation approaches. By analysing finite element calculations, it was possible to identify the stress state in the first load-bearing thread as decisive with regard to brittle fracture. In component tests at low temperatures, in which the screws were pre-damaged from a mechanically introduced notch under a fatigue load, it was clearly demonstrated that the screw steels currently used are not at risk of brittle fracture when used at temperatures down to -50 °C. Based on the test results, fracture and damage mechanics calculation models were created in order to define minimum requirements for the material properties to prevent brittle fracture. The damage mechanics model showed very conservative results here, so that it is currently not possible to derive minimum requirements without further development. The fracture mechanics model was able to reproduce the test results, but also delivered conservative results in the derivation of minimum requirements. The fracture mechanics model must be further verified on the basis of a broader database. In the present research project, however, a fundamental evaluation of the brittle fracture tendency of high-strength bolts of large dimensions at low temperatures was carried out. It was shown that the bolt steels currently used are not susceptible to brittle fracture when used at low temperatures. Publication date: April 2019 Authors: Prof. Dr.-Ing. habil. N. Stranghöner, Ch. Lorenz, M.Sc., Prof. Dr.-Ing. M. Feldmann, S. Citarelli, M.Sc., Prof. Dr.-Ing. W. Bleck, Prof. Dr.-Ing. S. Münstermann, Dr.-Ing. Brinnel
available anytime
View details →€40.00
excl. VAT
 FOSTA
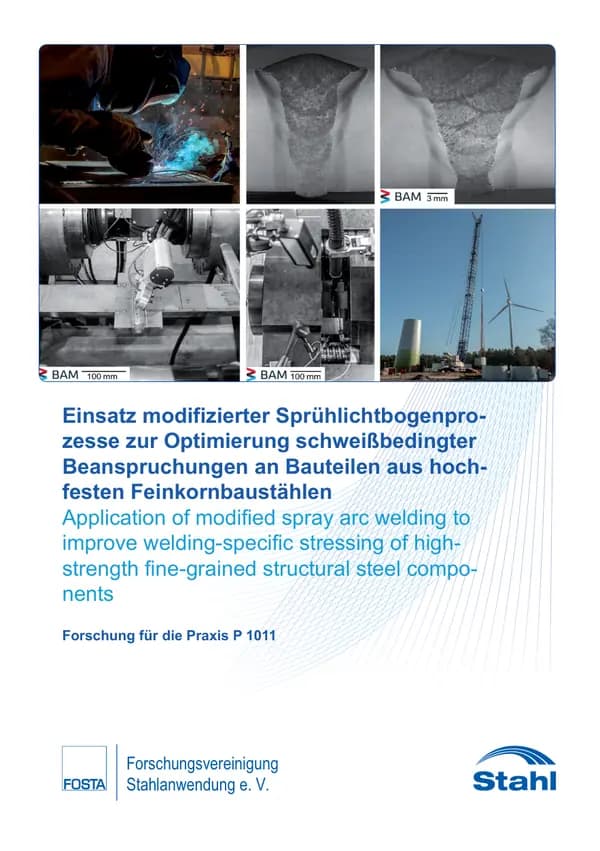
P 1011 - Use of modified spray arc processes to optimise welding-related stresses on components made of high-strength fine-grain structural steels
P 1011 - Use of modified spray arc processes to optimise welding-related stresses on components made of high-strength fine-grain structural steels Due to current lightweight construction efforts and demands for energy and resource efficiency, high-strength fine-grain structural steels with yield strengths ≥ 690 MPa are increasingly being used in modern steel structures. These are primarily processed with yield strengths of up to 960 MPa and joined using MAG welding processes. Modern inverter technology has recently enabled numerous company developments (e.g. "DeepARC", "forceArc"), which have led to modified spray arc welding (mod. SLB) with similar properties. In addition to the well-known economic advantages of these mod. SLB, the reduced possible seam opening angles and the lower heat input are expected to have a positive effect on welding-related stresses. Initial residual stress analyses in previous weldability tests with mod. SLB have already shown lower residual tensile stresses in the weld seam in free-shrinking laboratory samples compared to conventionally welded samples. However, the operationally stable design of high-strength welded constructions and the utilisation of high yield strengths require sufficient quantification of welding-related stresses in mod. SLB under defined, component-relevant shrinkage restraint. This concerns both the forces and stresses in the local weld seam area and the overall stress as well as the influence of heat conduction, component geometry, degree of clamping and seam opening angle. There was hardly any knowledge of this in the industry, especially among SMEs, and the aim of this research project was therefore to develop this knowledge. The comparative investigations with conventional arc and mod. SLB with adapted seam configuration were carried out with the aid of special testing equipment that can be used to model real component stiffnesses. With both process variants, weld seams could be realised with the selected parameters while fulfilling the requirements for the mechanical-technological properties. During the analyses, a significant reduction in internal stresses due to reduced heat input was observed when using a seam configuration with a lowered seam opening angle. In particular, the narrower seam gaps proved to be effective in reducing multi-axial stress states due to bending moments in the welds close to the component. The knowledge gained and recommendations made were presented to the relevant standardisation committees in order to facilitate simpler design and safe processing of high-strength fine-grain structural steels in the medium term, especially for SMEs. Standardisation can reduce qualification and approval costs, which are currently often necessary when using high-strength steels. Furthermore, the results will enable companies to utilise the technical and economic advantages of mod. SLB processes and to achieve significant savings in filler metal, welding and set-up time as well as optimised results with regard to the load-bearing capacity of components, taking into account the inherent stresses, and to increase productivity. Publication: 2017 Authors: T. Kannengießer, D. Schröpfer
available anytime
View details →€30.00
excl. VAT
 FOSTA
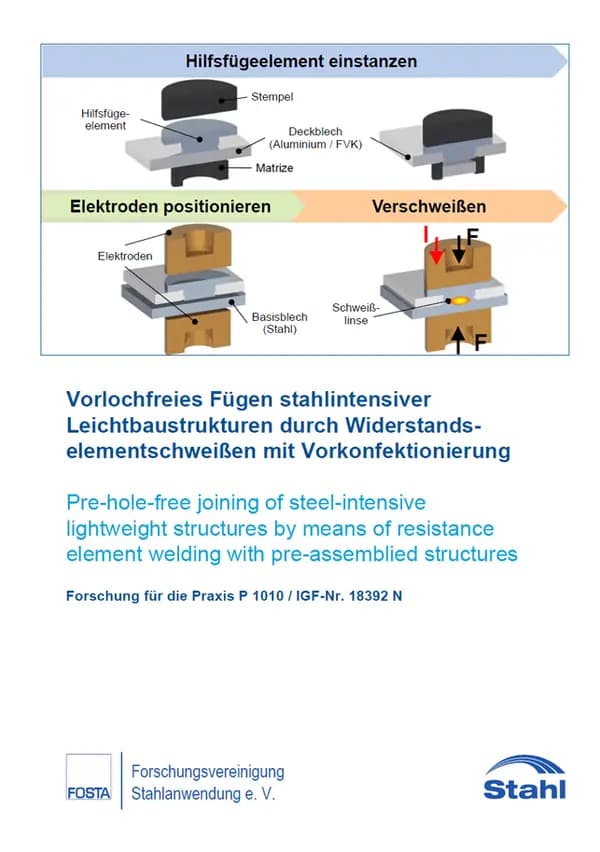
P 1010 - Pre-hole-free joining of steel-intensive lightweight structures by resistance element welding with prefabrication
P 1010 - Pre-hole-free joining of steel-intensive lightweight structures by resistance element welding with prefabrication In recent years, due to legal requirements, the automotive industry has increasingly focussed on lightweight construction measures, particularly in the body structure through the load-appropriate use of various lightweight materials. A mixed construction method, in which high-strength and ultra-high-strength, press-hardened sheet steel parts are combined with aluminium materials, is particularly suitable for large-scale production in order to create lightweight, yet rigid and crash-resistant body structures in shell construction. The thermal-mechanical joining processes developed in recent years for series production and not exclusively for this application offer a high application potential and the first series applications have already been realised. Due to the novelty of resistance element welding, the process-related properties and characteristics have so far been insufficiently investigated, so that there is a lack of sufficient knowledge on the welding, strength and failure behaviour of corresponding joints and material combinations. The aim of the research project was to develop and qualify resistance element welding with prefabrication of an aluminium or FRP composite partner as an economical joining process for joining these lightweight construction materials with high-strength and ultra-high-strength steel materials. As resistance element welding is still a relatively new joining process, the requirements were initially adapted on the basis of the investigations carried out to date. This involved analysing the special process-related features of resistance element welding of prefabricated composite partners and characterising the properties of the resulting joints. By analysing the joining process and the joint formation, taking into account the properties of the rivet elements, it was possible to gain important insights into the design of the rivet elements and processes as well as their reliable use. The evaluation of the performance characteristics in terms of joint and handling strength was also part of the project. As a result, industrial users were provided with information on the use of a flexible joining process for the realisation of future lightweight structures. The implementation of the optimisation derived from the results obtained marks an important contribution to the development of resistance element welding and the economic production of future lightweight structures in mixed steel construction. Publication: December 2020 Authors: Prof. Dr.-Ing. G. Meschut , Dipl.-Wirt.-Ing. V. Janzen
available anytime
View details →€30.00
excl. VAT
 FOSTA
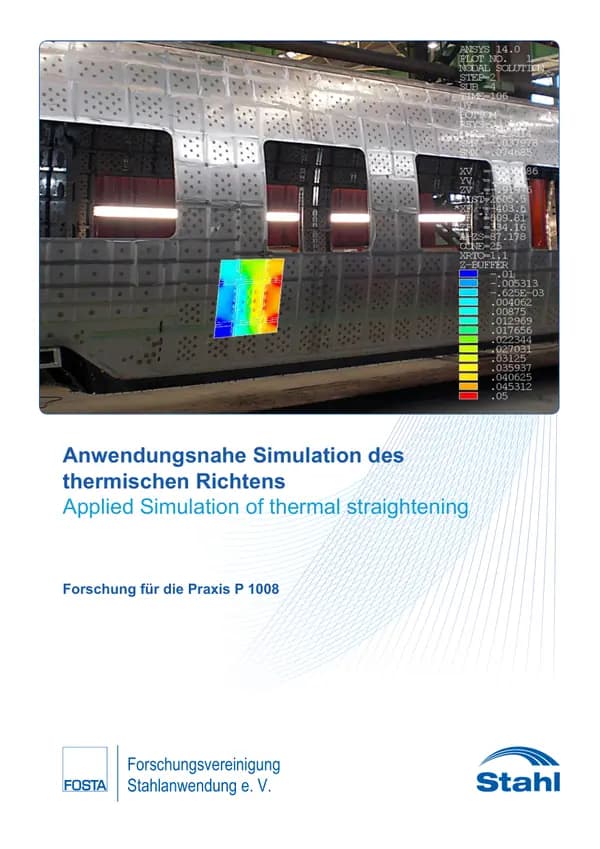
P 1008 - Application-oriented simulation of thermal straightening
P 1008 - Application-oriented simulation of thermal straightening Particularly in the case of large structures, such as those welded in ship and rail vehicle construction, the remaining distortions are very critical due to their enormous dimensions of up to several centimetres. Post-treatment must therefore be included in the work planning just as much as the welding itself. Thermal straightening has been an established process for decades. The straightening process parameters are currently selected on the basis of practical experience. However, the influence of design conditions, the material and the different straightening processes are extremely difficult to determine in this way. The basics of the analytical model, the realisation for practical application and the coupling with the numerical calculation are presented. The coupled analytical-numerical hybrid model is designed to capture the welding process chain and the subsequent thermal straightening. The analytical model is used to determine the equivalent shrinkage strain for the thermomechanical load of each straightening point, taking into account the significant influencing factors. This is transferred to an FE model of the structure and the deformation of the entire structure is calculated using an elastic analysis. The mutual influence of the existing residual welding stresses and individual alignment points is taken into account iteratively by means of feedback. The calculation is based on the application of the analytical numerical hybrid model for welding distortion simulation. The methodological approach is explained in detail in the report. In addition to the fundamentals of the hybrid model, other important aspects such as the recording of different straightening processes, process conditions and industry-relevant materials are also discussed. In addition, the qualitative interaction between thermal levelling and the welding process was investigated and integrated into the calculation procedure. The hybrid model was initially applied and validated on simple sheet metal specimens. Based on a structure joined by means of eight seams, the consideration of the welding sequence and the straightening sequence in the hybrid model was investigated. in the hybrid model was analysed. This was then applied to a test structure from the railway vehicle construction industry. Four 2 mm thick profiles were joined to a base plate measuring 500 x 400 mm using 16 weld seams and then straightened using two independent scenarios. The CPU time of the numerical calculation on the structures was less than 10 minutes in each case. The validity of the calculations was thus verified experimentally. Publication: 2016 Authors: V. Mikhailov, N. Doynov, F. Kuke
available anytime
View details →€30.00
excl. VAT
 FOSTA
P 1007 - Method for characterising the failure behaviour of high-strength sheet steel materials in a wide range of stress states using uniaxial tensile testing machines
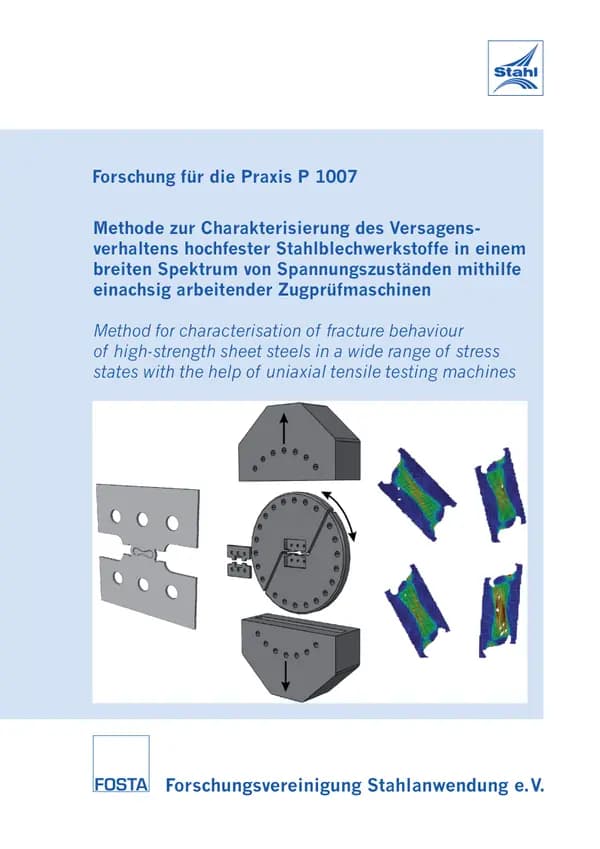
P 1007 - Method for characterising the failure behaviour of high-strength sheet steel materials in a wide range of stress states using uniaxial tensile testing machines The main objective of the project was to develop a new method for characterising the failure behaviour of high-strength sheet steel materials. This method should be based on shear tensile tests on new shear tensile specimens using a new testing module in uniaxial tensile testing machines as well as on hydraulic cupping tests and enable failure characterisation in a wider range of stress states compared to the conventional forming limit curve. The core of the developed approach is the new shear tensile specimen, which is characterised by a localisation of deformation leading to crack initiation inside the material and not at a free edge, regardless of the direction of an external uniaxial load in the specimen plane. A new test module was designed and manufactured for the shear tensile tests on the new shear tensile specimens, which applies a uniaxial test load into the following stresses in the material to be tested: a uniaxial tensile load with a superposition of hydrostatic tension, five different tensile shear loads with a dominant tensile or shear component and a compressive shear load with a dominant shear component. The degree of failure deformation of a dual-phase sheet steel material was experimentally determined using shear tensile tests with five different specimen orientations to the test load using an optical measuring system. In addition, the prevailing stress triaxiality at the material point of crack initiation was determined by numerically modelling the shear tensile tests performed. By combining the respective mean value of the experimentally determined degrees of failure deformation and the respective characteristic value of the numerically determined stress triaxiality, a support point for the fit of the material-specific failure curve was obtained for each tested material stress. In addition to these five support points, a support point from hydraulic cupping tests was also included. From the relative arrangement of the six support points, it can be seen that the dependence of the degree of failure deformation on the stress triaxiality is fundamentally captured using the developed approach. Although the work carried out confirms the fundamental suitability of the approach for characterising the failure behaviour of high-strength sheet steel materials, it also reveals possibilities for its further development. Individual focal points of this further development are an optimisation of the sample geometry to suppress edge cracks, an investigation into the influence of sample production on test results, improvements in recording the time and position of crack initiation and an investigation into the transferability of test results to the numerical simulation of forming processes. In the foreseeable future, these focal points are to be addressed more intensively in newIF UM research projects in order to promote acceptance of the newly developed method in the simulation-based design of sheet metal forming processes in the research landscape and in industrial practice. The research project P 1007 of the Forschungsvereinigung Stahlanwendung e.V., Düsseldorf, was carried out by the Institute of Forming Technology and Machines, University of Hanover, with technical support and financial assistance from FOSTA. Publication: 2015 Authors: B.A. Behrens, M. Vucetic, I. Peshekhodov
available anytime
View details →€20.00
excl. VAT
 FOSTA
P 1005 - Investigations into the load-bearing behaviour and service life of bonded joints in steel structures under cyclic loading
P 1005 - Investigations into the load-bearing behaviour and service life of bonded joints in steel structures under cyclic loading The use of innovative adhesive bonding technology increases the productivity, quality and efficiency of German steel construction. It also represents an alternative to conventional joining methods, which have fundamental disadvantages for steel structures. For example, the bonding joining process can avoid welding-related component distortion and cross-sectional weakening due to bolt holes. Due to the high degree of prefabrication, steel construction is predestined for the use of adhesive bonding, as load-bearing, serviceable and durable bonded joints can be produced under workshop conditions. However, it is not possible to verify such bonded steel joints on the basis of current standards. Time-consuming and expensive approval procedures would be necessary, which is why small and medium-sized enterprises (SMEs) decide against adhesive bonding technology. The inclusion of bonded steel joints in standardisation would provide a remedy here. For this reason, the first step is to develop basic principles for the verification of load-bearing capacity using two application cases from steel façade construction, which relate exclusively to short-term, one-off and quasi-static loads. A further aim of the project is to supplement these findings by investigating the long-term load-bearing behaviour of bonded joints under cyclic loading. The results of the analyses provide input parameters for the development of verification concepts for bonded steel joints. Publication: 2018 Authors: Prof Pasternak, Prof Dilger
available anytime
View details →€30.00
excl. VAT
 FOSTA
P 1004 - Hybrid forging Combined forming and joining
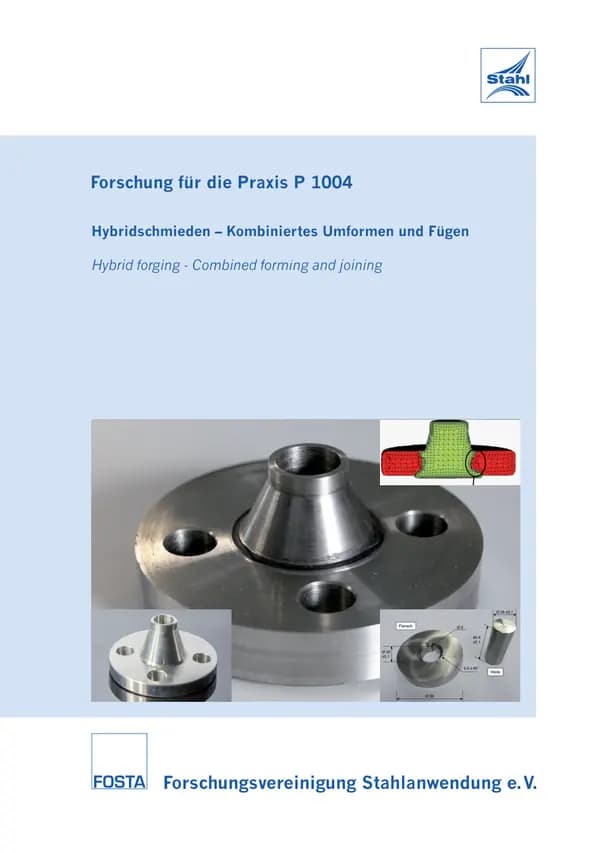
P 1004 - Hybrid forging - Combined forming and joining This study investigated the feasibility and potential of a hot Hyrid forging process for a pressure flange. This process is characterised by the simultaneous forming and joining of a thick plate and a shaft in one step. Firstly, the process was designed using FEM software. Compared to a reference process, significant reductions in the press force were achieved, making it possible to forge larger flanges on smaller forming units. The stainless steel X6CrNiMoTi17-12-2 (1.4571) was used as the material. Tests were then carried out on an industrially used eccentric press. The key feature was to ensure a positive fit between the two components, as it was not possible to achieve a material bond. For this purpose, the sheets were provided with a chamfer and recesses, which were filled with the material of the shaft during the forming process to prevent axial and radial displacement. This goal was achieved. To achieve this, however, the sheet metal had to be heated more than the shaft material, as otherwise gaps would have formed after cooling due to thermal shrinkage. The pressing forces could also be reduced in reality. Normally, the real process requires press forces of approx. 800 tonnes for forging with burrs. These forces are higher with burrless forging. A significant reduction in pressing forces has therefore been achieved. Forging companies can now manufacture rotationally symmetrical parts in a manual production process using hybrid forging. This means that parts can be produced without burrs with a low forming force. This leads to a reduction in tool stress and thus to an increase in tool life. Smaller presses can be used for comparable parts. Automation including feeding technology is still to be developed. This means that long parts can also be produced, which make up a larger proportion of solid moulded components in industry. The research project P 1004 of the Forschungsvereinigung Stahlanwendung e.V., Düsseldorf was carried out by the IPH - Institut für Integrierte Produktion Hannover GmbH with technical support and financial assistance from the Forschungsvereinigung Stahlanwendung e. V., Düsseldorf. Publication: 2015 Authors: J. Langner, M. Stonis
available anytime
View details →€20.00
excl. VAT
 FOSTA
P 1001 - Technology benchmark for pre-hole-free resistance element welding on conventional resistance spot welding systems
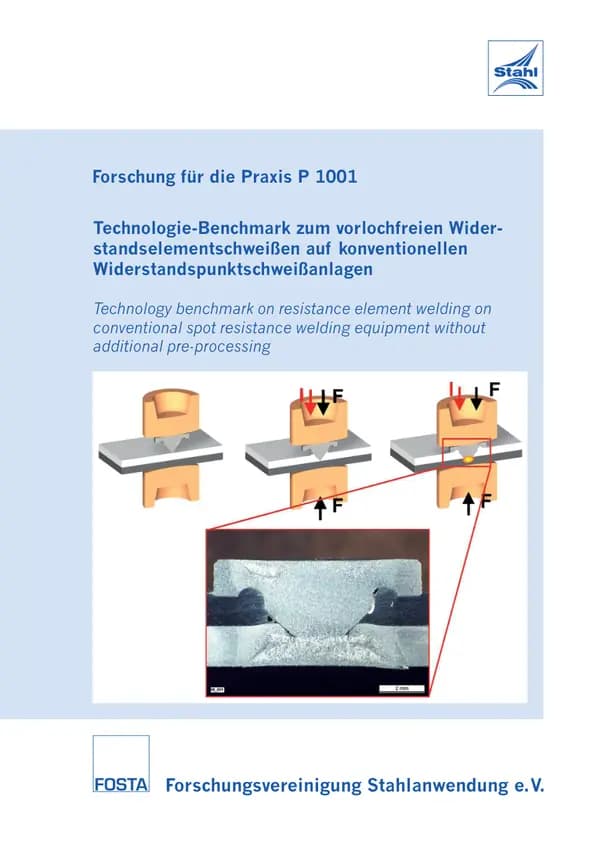
P 1001 - Technology benchmark for pre-hole-free resistance element welding on conventional resistance spot welding systems Increasingly scarce resources against the backdrop of rising customer demands and the implementation of climate policy targets through emission limit values require a reduction in the fuel and energy consumption of automobiles and are therefore the driving forces behind all lightweight construction endeavours. The body is the most massive component in the car and harbours great potential for economical weight reduction through intelligent lightweight construction concepts. Depending on the requirements of the vehicle's substructure, high-strength and ultra-high-strength steels are combined with aluminium and fibre-reinforced plastics (FRP). New joining processes are required for the affordable realisation of these lightweight structures in order to overcome the obstacles that arise, such as the metallurgical incompatibility of these material pairings. The targeted further development of combined joining processes represents a promising solution for this. Resistance element welding (WES) fulfils the above-mentioned requirements and is currently being developed and qualified for body-in-white construction. In WES, a rivet-shaped element is inserted into the composite partner (e.g. aluminium, FRP) and joined to the underlying steel sheet using conventional resistance spot welding technology (WPS). According to the current state of development, the composite partner is pre-punched in the WES and the rivet elements are then positioned or the rivet elements are pre-assembled in the component. This is associated with a high manufacturing effort and an economic disadvantage due to an additional process step. The development of pre-hole-free WES using conventional WPS systems is therefore a worthwhile area of investigation. In contrast to the aforementioned process variants, pre-punch-free WES does not require any preliminary operations, as the rivet element is punched and welded by the electrodes in a single step. The problem in this context is the assessment of the general feasibility of this process variant. Due to the complexity of the joining process, there are numerous boundary conditions, system-related limits and special process-related features. As part of the SME study, these were systematically determined and an investigation into the feasibility of pre-hole-free resistance element welding, in which the riveting elements are inserted into the FRP or aluminium with the electrode forces and then welded by means of resistance heating, was carried out. and welded to the steel materials by means of resistance heating. It has been shown that this is particularly feasible for joining aluminium/steel combinations. The research project P 1001 of the FOSTA Research Association for Steel Application e. V., Düsseldorf, was carried out at the Laboratory for Materials and Joining Technology, University of Paderborn, with technical support and financial assistance from the Research Association for Steel Application e. V., Düsseldorf. Publication: 2015 Authors: G. Meschut, O. Hahn, V. Janzen
available anytime
View details →€20.00
excl. VAT