When constructing large steel structures in bridge or steel building construction, modular factory production is increasingly used today. factory production. However, it is still necessary to join these modules on site …
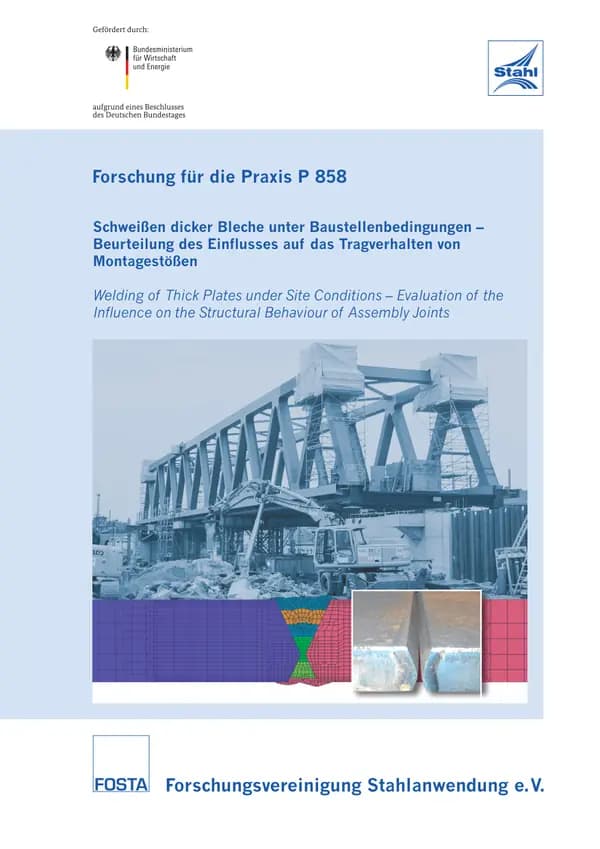
When constructing large steel structures in bridge or steel building construction, modular factory production is increasingly used today. factory production. However, it is still necessary to join these modules on site to form an overall structure. MAG multi-pass welding is often used as the joining process here. Especially on thick sheet metal, construction site welding not only places special demands on the company carrying out the work, the site management and site supervision, but also on the designer. It is important for the designer to be aware of the shrinkage of the components caused by welding, the distortions that occur and the residual stresses.
These aspects must be taken into account during the design phase of the individual components, particularly in the case of construction site welding, in order to maintain the required tolerances during assembly. Construction and assembly companies often only have precise knowledge of the phenomena caused by welding based on several years of experience. A basic, complete picture of the welding processes on the construction site, which would enable this knowledge to be transferred to new constructions, is still lacking. In particular, knowledge of the behaviour of high-strength fine-grain structural steels (e.g. S460), which are increasingly used in bridge and steel construction, is necessary. This is where the research proposal comes in. With the help of welding simulation, the effects of weld seams, such as the formation of distortions and residual stresses on the component, can be visualised globally. Subsequent structural simulations (strength and stiffness calculations) with results integrated from the welding simulation form the basis for supplementary investigations. Assembly joints are also negatively influenced by soiling and weathering. For example, assembly may have to be carried out at low temperatures below freezing. This situation was simulated in a climate chamber and the effects of the ambient temperature during assembly on the load-bearing behaviour of the joint were investigated. For the cases investigated as part of the project, no influence of varying ambient temperatures down to -10 °C on the resulting residual welding stresses was found. The comparison of distortion and residual stress with standardised tolerance values and simplified engineering models for the approximation of the residual stress curve shows major deficits. If the residual stresses are implemented realistically in the ultimate load calculation, large reserves can be utilised in some cases within the framework of the non-linear ultimate load calculation. The IGF project 16937 BG of FOSTA - Forschungsvereinigung Stahlanwendung e.V., Düsseldorf, was funded via the AiF within the framework of the programme for the promotion of joint industrial research (IGF) by the Federal Ministry for Economic Affairs and Energy on the basis of a resolution of the German Bundestag. The project was carried out at the Institute of Joining and Welding Technology at the Technical University of Braunschweig and the Chair of Steel and Timber Construction at the BTU Cottbus-Senftenberg.
Payment by card (Stripe) or invoice (DE, AT, CH). Download link by email: automatically after ordering by card, after order approval for invoice (valid for 30 days). Terms
Machine-translated title and description. The document itself is in German.
Digital download
Other parts and editions as well as neighbouring documents of the same series.

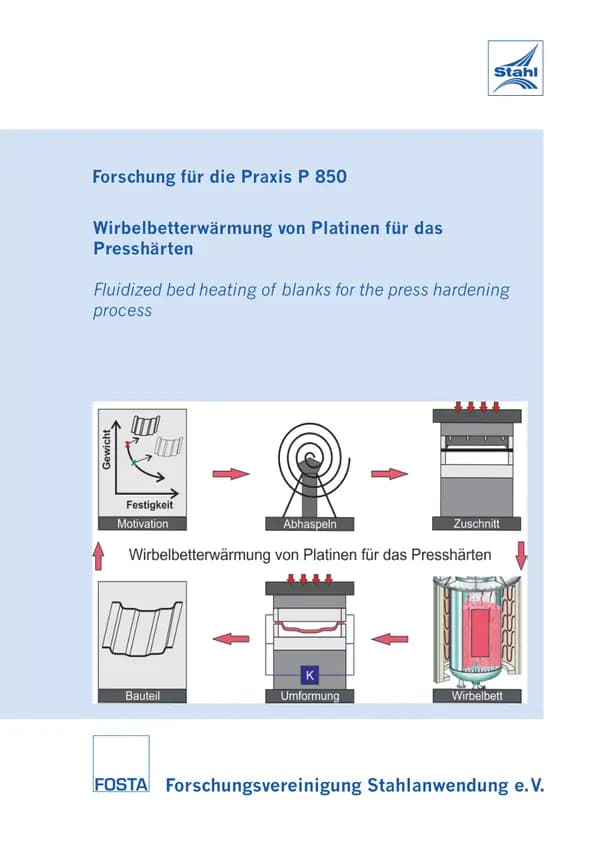
P 850 - Fluidised bed heating of blanks for press hardening The careful use of resources and the avoidance of environmentally harmful emissions, e.g. in production, energy generation and mobility processes, are globally recognised tasks of the international community. In this context, lightweight construction of moving masses is one of the leading technology drivers. A significant reduction in resource and energy consumption can be achieved through the increased use of lightweight products. The material steel will therefore only be able to assert itself in the future if the aspects of lightweight construction become even more important. In fact, steel offers an excellent option here, namely to achieve a considerable improvement in the strength-to-density ratio by increasing strength. The press hardening process offers a prominent possibility for realising this. The press hardening process for manganese-boron steels can be used to produce high-strength, complex component geometries that are already used in many structural areas of vehicles. One disadvantage of these press-hardened components is currently the relatively high process costs, which are caused, among other things, by high investments and the high space requirements of the corresponding roller hearth furnaces for heating the blanks. There is a need here to identify more cost-effective and space-saving heating options. The aim of the research project is therefore to develop and investigate the fluidised bed heating of steel blanks for press hardening. This alternative heating process is already used today, for example, for the industrial heating of solid components and, due to the process parameters, also offers great potential for heating in the press hardening process. Experimental investigations were therefore carried out on corresponding fluidised bed furnaces as part of the research project. This included the determination of heating gradients as well as tests on the use of different coating systems. Finally, the aspect of partial press hardening was examined in more detail, so that the heating behaviour of the blanks during partial heating in the fluidised bed was investigated. The tests carried out in this research project demonstrate the general suitability of fluidised bed heating of blanks for the press hardening process. Blanks made of press-hardenable steels can be heated to the required process temperatures using this heating method. The coating systems currently in use can also be utilised for the press hardening process, subject to certain restrictions. In addition, the production of graded component structures by partially heating the initial blanks before forming can, in principle, be realised using fluidised bed heating. The research project was carried out at the Chair of Lightweight Automotive Design (LiA), Paderborn University, together with Benteler Automobiltechnik GmbH, Paderborn and Schwing Fluid Technik GmbH, Neukirchen-Vluyn, with technical support and financial assistance from the Forschungsvereinigung Stahlanwendung e. V., Düsseldorf, with funds from the Stiftung Stahlanwendungsforschung, Essen. Authors: T. Tröster, T. Marten, S. Adelbert, A. Kadim Publication: 2012
available anytime
€20.00
excl. VAT

P 822 - Use of the laser beam-MSG hybrid welding process on longitudinally welded large-diameter pipes of grade API-X80/ -X100 to increase toughness and efficiency A significant proportion of modern oil and gas pipelines are made from longitudinally welded large-diameter pipes in API steel grades X65 (L450, 1.8726) and X70 (L485, 1.8727). Constantly increasing natural gas and crude oil production rates in conjunction with minimising wall thickness or increasing operating pressure will in future require corresponding material substitutions with modern higher-strength materials, such as API-X80 (L555, 1.xxxx), X100 (L690, 1-xxxx) and X120, with sufficient strength and toughness. The submerged arc welding process is used to weld these pipes. The entire pipe length is first welded with a continuous MSG tack weld. To increase economic efficiency, this process step is to be replaced by the laser beam-MSG hybrid welding process. For the safe operation of large-diameter pipes, the required impact strength of the welded joint must be observed in addition to the strength properties. Against this background, the primary research objective of this research project was to define and systematically investigate the achievement of sufficient toughness in the temperature range of -60°C and -40°C with economic process parameters. Suitable filler materials (solid wire and flux-cored wire electrodes) were identified for the laser-MSG hybrid welding of the aforementioned high-strength pipeline materials and systematic studies were carried out on the dependence of toughness on solidification behaviour and the achievable mixing depth. Increased economic efficiency when using laser hybrid technology is seen primarily in the modified seam preparation. A constructive change in the joint shape leads to a reduction in the seam volume and thus to a considerable reduction in production costs, because in this case the amount of filler material required to fill the seam is reduced. Based on demonstrators produced, an approx. 2.7-fold reduction in the seam cross-section and thus the required quantity of filler material is demonstrated. The IGF project 16415 N of FOSTA -Forschungsvereinigung Stahlanwendung e.V., Düsseldorf, was carried out at the Federal Institute for Materials Research and Testing (BAM), Department 9.3 "Welding Manufacturing Processes", Berlin, and funded by the Federal Ministry of Economics and Technology via the AiF as part of the programme for the promotion of joint industrial research and development (IGF) on the basis of a resolution of the German Bundestag. Authors: M. Rethmeier, S. Gook, A. Gumenyuk Publication: 2013
available anytime
€30.00
excl. VAT
Payment by card (Stripe) or invoice (DE, AT, CH). Download link by email: automatically after ordering by card, after order approval for invoice (valid for 30 days). Terms