As part of the research project "Optimised production of component families with a geometrically flexible deep-drawing tool", the possibilities and limitations of geometrically flexible deep-drawing in comparison to …
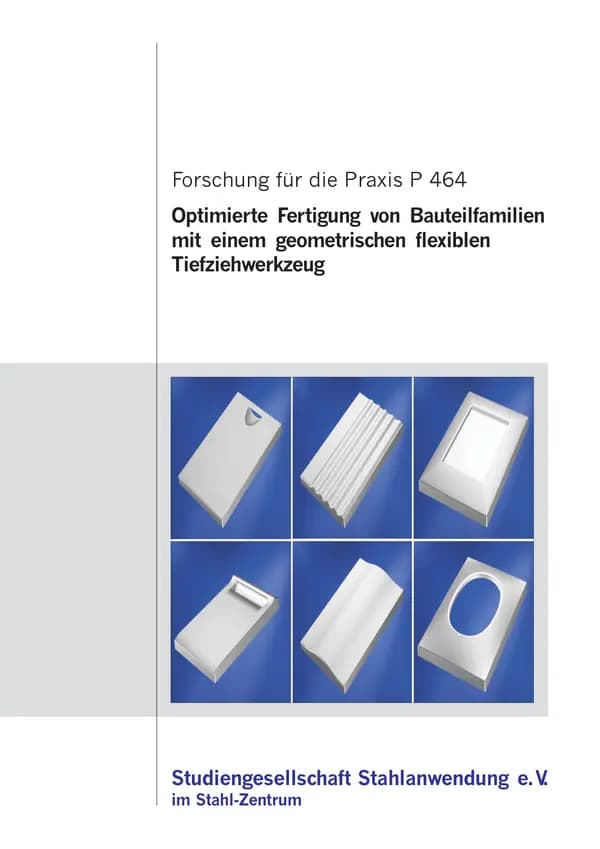
As part of the research project "Optimised production of component families with a geometrically flexible deep-drawing tool", the possibilities and limitations of geometrically flexible deep-drawing in comparison to bending and joining for the production of steel furniture were developed. The process comparison was carried out with regard to quality of the workpiece and the economic use of geometrically flexible deep drawing. In this process, the shaping contour of the upper and lower tool is formed from several basic tool elements in a tool system. The dimensions of steel furniture components are based on standardised series and form so-called component families.
The geometrically flexible deep-drawing manufacturing process therefore has the potential to reduce both tool costs and the number of secondary operations. Tool costs can be reduced as several component geometries can be realised with one tool system. In addition, it is also possible to incorporate secondary mould elements such as drainage channels for counter elements or recesses for door handles into a process. At the same time, the user has new process-integrated options for product design. Taking into account the requirements of the furniture industry, a geometrically flexible thermoforming mould was developed, manufactured and tested as part of the research project. Design studies by a project partner were used to design the realised component geometry. With the currently realised degree of automation of the deep-drawing tool, the economic limits lie at batch sizes above 85 pieces, depending on the workpiece geometry, with an annual volume of 3000 pieces. The component quality is influenced by the unavoidable segment wear, whereby thinner sheet materials react particularly sensitively to segment transitions. The limit to reject parts is closely linked to the respective application. By painting the moulded sheet metal parts produced, any surface defects could be completely eliminated. Investigations into the component properties have shown an increase in dent resistance when using deep drawing compared to bent and joined components. This is caused by a hardening of the sheet material as a result of the stresses in the deep drawing process. The buckling resistance of deep-drawn sheet metal moulded parts is, however, partly influenced by the bottom area's punch-through effect. The punch-through effect occurs depending on the geometry, whereby the sheet thickness and material strength are decisive influencing variables for the occurrence of the punch-through effect. At the end of the research project, the tool principle presented will be available to sheet metal processing companies for series production. Sheet metal moulded parts with high demands on the appearance of the sheet metal moulded parts can be produced with geometrically flexible deep drawing. The potential user can select the process according to the requirements of the component to be manufactured, with the annual volume in particular being a key criterion. The technology of geometrically flexible deep drawing is already being used successfully by a project partner. The results of the research project have been directly incorporated into the component design and mould design of the participating companies. In particular, the analyses for evaluating component quality are taken into account.
Payment by card (Stripe) or invoice (DE, AT, CH). Download link by email: automatically after ordering by card, after order approval for invoice (valid for 30 days). Terms
Machine-translated title and description. The document itself is in German.
Digital download
Other parts and editions as well as neighbouring documents of the same series.

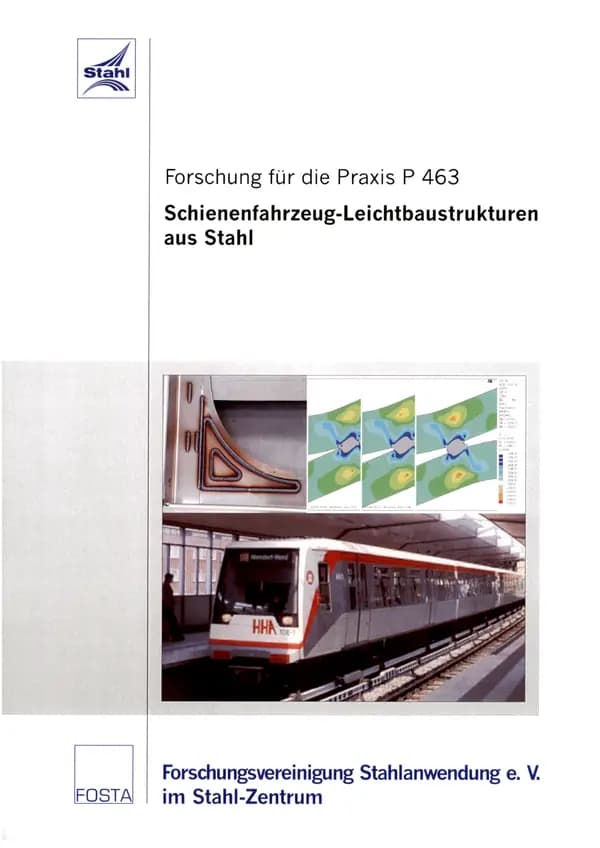
P 463 - Lightweight steel structures for railway vehicles Authors: H. Haferkamp, J. Bunte, P. Cordini, A. Bormann, B. Block Publication: 2004 Abstract This research project focuses on using laser welding technology to increase the competitive potential of steel rail coaches manufactured using differential construction. It is based on the fact that rail coach manufacturing has increasingly been using integral construction with extruded aluminium profiles for the last several years. This manufacturing process is on the one hand cost-intensive, due to the expensive semi-finished parts, and on the other hand there is only limited geometrical flexibility in the rail coach body design, due to the limited variety of aluminium profiles. A laser welding technique for manufacturing stainless steel side panels for rail coaches (passenger transport) has been developed in co-operation with the Alstom-Linke-Hofmann-Busch GmbH in Salzgitter. The structures are built using differential construction. The side panels consist of a framework substructure made of profiles, on which a metal sheet outer skin is welded. In contrast to the similar structure of omnibuses, the outer skin is also load bearing (in a shearing connection). Conventional gas metal arc welding and resistance spot welding in particular cause distortions and local surface defects in the form of stamped impressions on the visible exterior. These can only be minimized by complex and personnel-intensive reworking.
available anytime
€25.50
excl. VAT

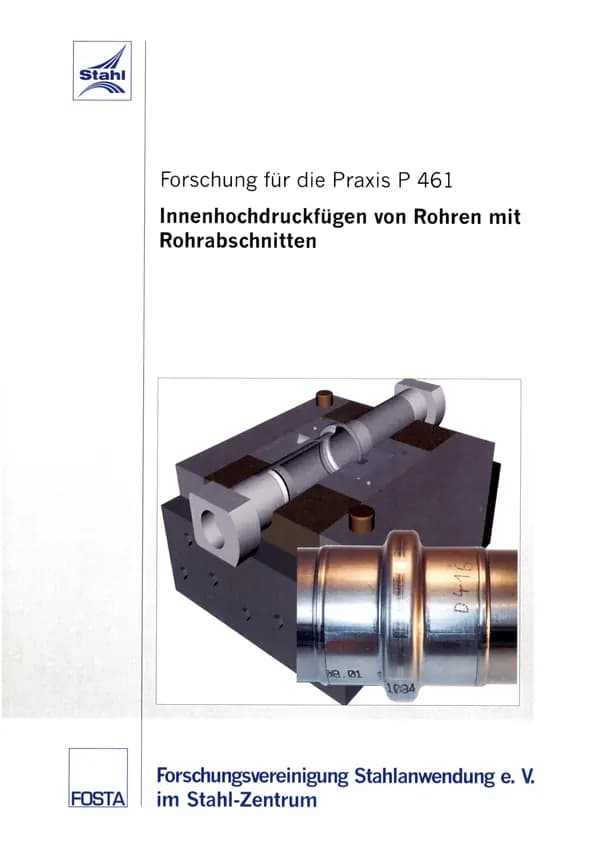
P 461: Hydroforming of pipes with pipe sections (IHF) Based on current demands for innovative lightweight construction solutions, new possibilities for the production of property-optimised hollow moulded lightweight components can be developed with the hydroforming of tubes with tube sections, particularly in vehicle construction. As part of this project, the process fundamentals for joining with dominant force and positive locking of thin-walled tubes with tube sections made of practically relevant steel grades and for the forming and punching of composite parts were investigated, the technological feasibility demonstrated and key process parameters scientifically developed. The knowledge gained from theoretical considerations was verified and expanded with experimental investigations. As a result, the feasibility of hydroforming thin-walled pipes with pipe sections in the process variants of dominant force fit and dominant form fit was demonstrated. In addition to the experimental investigations, the joining processes for certain parameter variations were modelled using FEM simulations. This provides an effective tool for the structural design of the components and for safe process design in hydroforming. The focus of the investigations was on achieving favourable final part properties in interaction with the initial part properties and the conditions of the special hydroforming process when creating the composite. With this in mind, the process parameters and limits were determined for the individual process variants. In addition, the final part properties of the components were determined and summarised in a table. The functional evaluation of the composites was predominantly carried out geometrically and/or functionally neutral using simplified test methods to determine maximum axial forces. Hydroforming as well as hydroforming and perforating of composite parts opens up extended technical possibilities for the production of lightweight hollow moulded components with locally different material and geometric properties at high flexibility and low costs. For the user, the research results were summarised in guidelines for process and tool design with regard to optimum end part properties. On this basis, the user companies can create or secure favourable market positions and a considerable competitive advantage with new lightweight construction technologies, especially for the material steel. FORSCHUNGSVEREINIGUNG STAHLANWENDUNG e.V. Publication: 2004 Authors: Prof. Dr.-Ing. A. Eichhorn, Dipl.-Ing. F. Meyer
available anytime
€30.00
excl. VAT

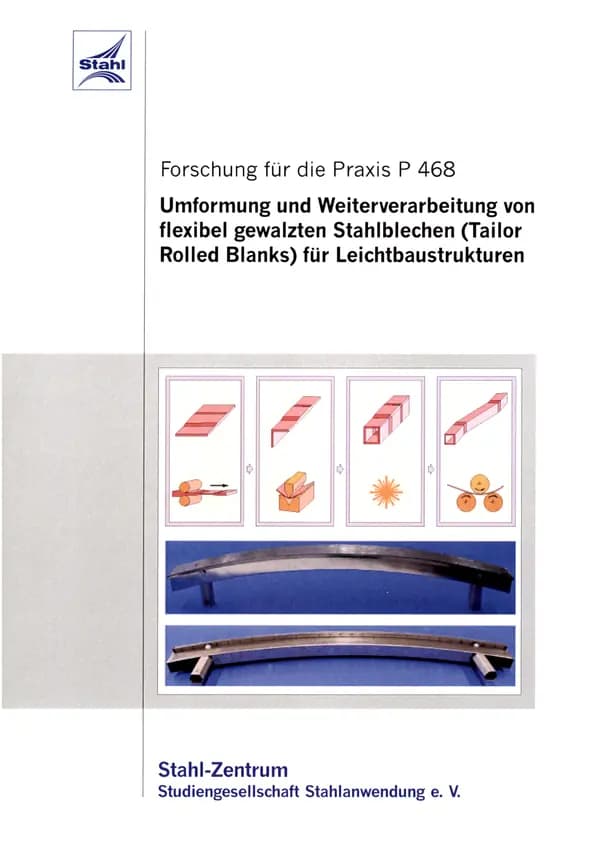
P 468: Forming and further processing of flexibly rolled steel sheets (tailor-rolled blanks) for lightweight structures Compared to Tailor Welded Blanks (TWB), flexibly rolled sheets, i.e. sheets with different thicknesses in the longitudinal direction, so-called Tailor Rolled Blanks (TRB), do not have an abrupt, but a continuous thickness profile. a continuous thickness progression. The advantage of this is the better adaptation to a lightweight component geometry. In addition, the continuous change in thickness under load results in a harmonious stress curve in the transition area, so that stress peaks can be avoided. The microstructure in the transition area of the sheet thicknesses is also not affected by the thermal influence of a welding process. The aim of the research project was to investigate and further develop the possible applications of flexibly rolled sheet metal. The research work focussed on the processing of stainless steel into profile-shaped load-bearing structures in a closed process chain. This included flexible rolling, possibly followed by heat treatment, die bending of the TRB, laser welding and profile bending. The individual production steps and their interaction within the process chain were optimised with regard to the lightweight construction potential in iterative steps between experimental investigations and supplementary FEM simulation calculations. The efficiency of the new process chain was successfully demonstrated using the example of a demonstrator - in this case a front car cross member including crash boxes based on corresponding components in the Ford Focus and Audi A3. Compared to the conventional designs made from standard semi-finished products, a weight reduction of around 13% was achieved with Tailor Rolled Blanks. They also showed significantly more favourable behaviour in the crash tests carried out. Tailor rolled blanks are primarily used in the automotive industry. First and foremost here are load-adapted, weight-optimised components in the passenger car sector. For example, open and closed support structures as transverse and longitudinal beams or hollow profiles are being considered. A further application is seen in the area of crash-relevant components. Here, the deformation behaviour and energy absorption can be specifically optimised by using different wall thicknesses. STUDIENGESELLSCHAFT STAHLANWENDUNG e.V. Publication: 2002 Authors: Prof. Dr.-lng. M. Kleiner, Dr.-lng. S. Chatti, Dr.-lng. B. Heller, Dipl.-Ing. Ch. Wiedner, Dipl.-Ing. P. Böhlke
available anytime
€30.00
excl. VAT

P 469: Use of steel wire for the production of solid metal catalytic converters The aim of this research project was to open up a new application for stainless steels as catalysts by means of appropriate surface activation, analogous to known solid metal catalysts based on Cu-, Co-, Mn- or Ni-rich alloys. The focus of the investigations was the development of a catalyst to minimise CO emissions during the ignition of car airbags. With the help of laboratory tests it was shown that activated stainless steel as a catalyst can reduce the CO content in the airbag propellant by approx. 80 %. In practical chamber tests, however, it was not technically possible to achieve the necessary reduction below the equilibrium temperature of approx. 850 °C for the conversion reaction in a reproducible manner with the specified generator design. In contrast, the field tests on catalytic sterilisation in swimming pools and ventilation systems were also successful on a technical scale. In the presence of a few ppm of hydrogen peroxide, water circuits were sterilised in an environmentally friendly manner without the addition of chlorine, chlorine-containing chemicals or organic biocides using activated stainless steel as a catalyst. The application benefits are worth emphasising: - No contamination with substances foreign to water, - No release of toxic or allergenic substances during germ decomposition (endotoxins) - No formation of hazardous by-products such as carcinogenic chlorinated hydrocarbons (AOX) Biofilms are automatically detached or the formation of new ones is prevented. This enables improved heat transfer and suppresses biologically induced corrosion phenomena. The specifications of the VDI guideline 6022 for the Flygiene operation of ventilation and air conditioning systems of max. 103 CFU/ml can be safely complied with. The tests carried out in the project on disinfection are now being used in an industrial application in the retrofitting of a 140 metre high cooling tower with a throughput of 50,000 m3 of water per hour. This involves the use of 1.5 tonnes of stainless steel mesh as a catalyst and a further 6 to 7 tonnes of steel materials for support elements. STUDIENGESELLSCHAFT STAHLANWENDUNG e.V. Publication: 2003 Authors: Dr rer. nat. H. Lausch
available anytime
€20.00
excl. VAT
Payment by card (Stripe) or invoice (DE, AT, CH). Download link by email: automatically after ordering by card, after order approval for invoice (valid for 30 days). Terms