
FOSTA
Normally, traditionally built houses as well as prefabricated houses have similar components as regards building technology. For example, this includes the supply with power and gas, the heating technology, the supply …
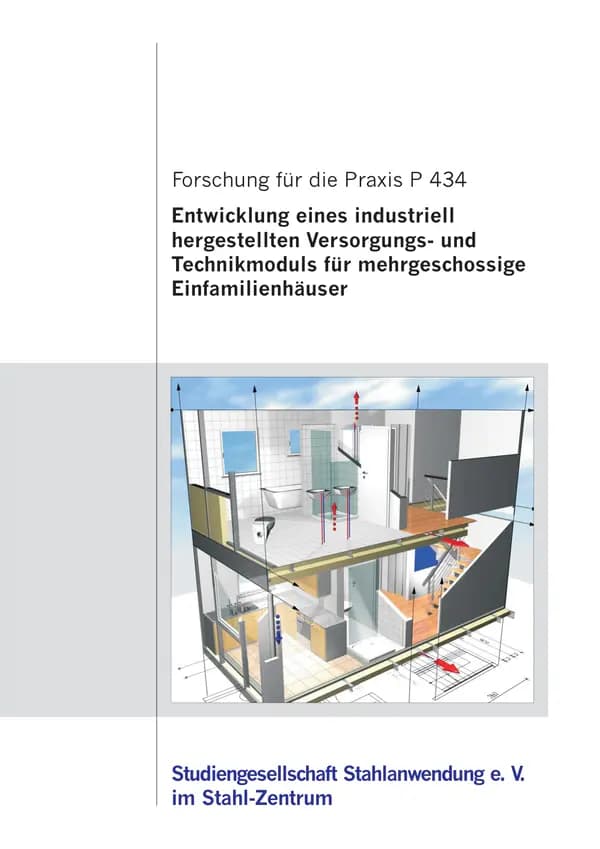
Normally, traditionally built houses as well as prefabricated houses have similar components as regards building technology. For example, this includes the supply with power and gas, the heating technology, the supply and disposal of water, sanitary equipment, communication technology as well as staircases and an optional lift. The current research project aimed at the concentration of these technologies to form a so-called supply and technical (VT) module for universal applications as far as possible. As an example, a product suitable for series production and adaptable to individual conditions was to be developed and produced for series production.
The cost-efficient high-quality steel frame design proven in module construction was the starting point for this as a static support structure. During an intensive planning phase predictive requirements were collected and designed to form a model. Static calculation showed that the VT modules could compatibly be placed one above the other for houses with up to 5 floors. The concept is based on a strict separation of the VT modules from the other rooms in the building. All interfaces have largely been standardized and are of the plug-in or screw-type. Thus, building units erected with the traditional building technology, room module and prefabricated wood design can be interconnected easily. During a modernization of old buildings with multiple floors the specially designed VT modules can be “docked” to existing buildings.
Machine-translated title and description. The document itself is in German.
Payment by card (Stripe) or invoice (DE, AT, CH). Download link by email: automatically after ordering by card, after order approval for invoice (valid for 30 days). Terms
Digital download
Other parts and editions as well as neighbouring documents of the same series.
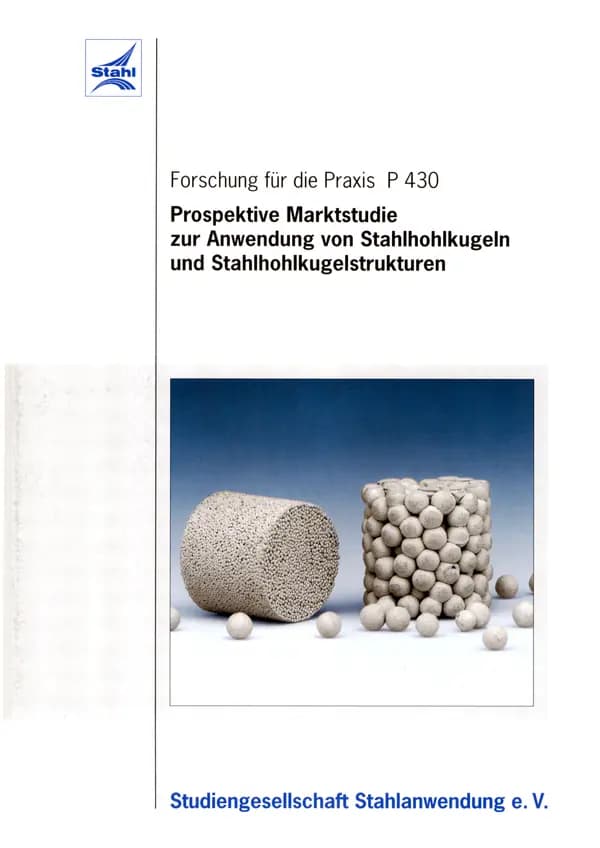
Metallic hollow spheres and hollow sphere structures made from them are an interesting technical alternative to metal foams. This study presents an assessment of the potential properties and possible applications of steel-based hollow sphere products. Based on literature and patent research, the currently available options for manufacturing hollow spheres are explained and compared. From today's perspective, the most favourable technology for mass production is the coating of polystyrene spheres with powdered materials and subsequent thermal treatment. The organic components are expelled and the metal powder particles are sintered to form a solid spherical shell. Requirements for the starting raw materials and the most interesting properties to be achieved, such as sphere diameter, shell thickness, bulk density, porosity and strength, are described. Possible applications for hollow steel spheres or structures made from them are seen in particular for crash absorbers, sound and heat insulators and lightweight structural elements. Comparisons are also drawn with the relatively similar application potential of metal foams, particularly those made of aluminium. The survey of industrial companies resulted in numerous suggestions for the market potential of hollow steel spheres or hollow steel sphere structures and the properties required. The study presents a development strategy for the manufacture and utilisation of products based on hollow steel spheres. The work is supplemented by an estimate of the likely manufacturing costs. The use and thus utilisation of secondary raw materials from steel production and processing may be a particularly advantageous option. STUDIENGESELLSCHAFT STAHLANWENDUNG e.V. Publication: 1999 Authors: Dr.-Ing. L. Schneider, Dipl.-Ing. U. Waag
available anytime
€20.00
excl. VAT
P 443 - Laser coating of cut surfaces on galvanised/coated sheet metal Authors: D. Maischner, K. Wissenbach, N. Pirch, H. Müller Publication: 2003 The corrosion protection of products out of steel sheets will be carried out mainly by continuous strip galvanics and subsequent coil coating with polymers (″Duplex″ technique). The cutting and stamping areas, which result from further manufacturing processes will be protected by conventional techniques like painting, lubricating, flanging of the edges and dip coating, which are not convincing solutions for the corrosion problem. Against this background the aim of this project is the development of basics for a laser induced coating process for cutting areas. The research work is focused on the process layout for a 1-step coating process for the cutting areas. This means that the powderised coating material and the laser beam interact simultaneously with the cutting area. For zinc coatings the zinc particles will be melted directly by the laser radiation and the laser heated cutting area. In contrast for polymer coatings the powder will be indirectly melted by the heated cutting area. The processing parameters will be adapted to prevent combustion and evaporation of the powder particles. The bonding strength and the corrosion resistance of the coated cutting areas were investigated. For zinc coatings as well as for the thermoplastic coating polyamid 11 (RILSAN) processing parameters could be developed, which show an excellent corrosion protection. Nd:YAG as well as diode lasers are suitable for this coating process.
available anytime
€25.50
excl. VAT
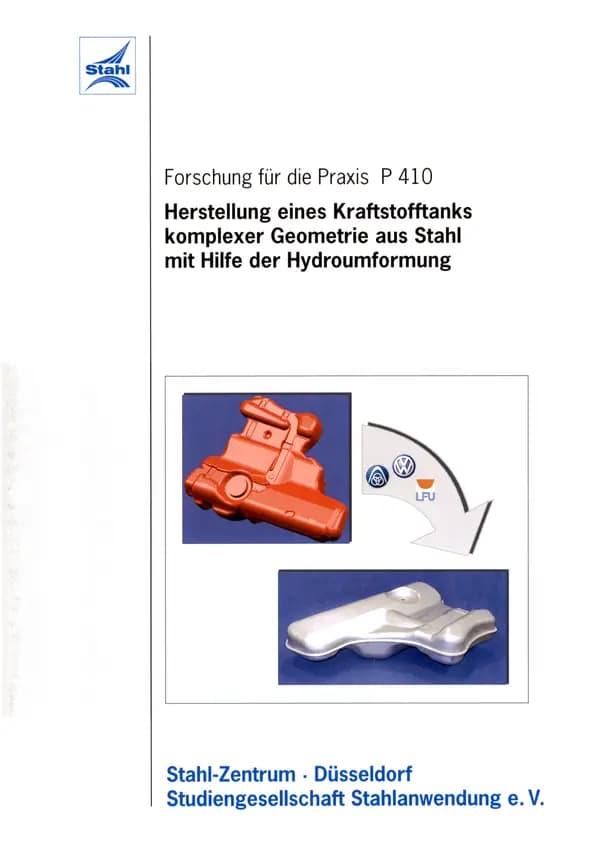
P 410: Production of a fuel tank of complex geometry from steel using hydroformingIn the course of stricter environmental protection requirements, the release of fuel oil components must be completely avoided. This requirement will soon apply to fuel tanks and can currently only be safely fulfilled with steel as a material. Design and safety requirements in car construction demand the positioning of the fuel tank in the less critical but very complex cavities of the car body in the event of a crash. The aim of this research project was to develop technical and economical solutions for the production of geometrically highly complex hollow bodies made of steel for this application with the help of active-media-based sheet metal forming. For the investigations, the tank of a New Beetle, PQ 34, from Volkswagen AG, which was previously made of plastic, was selected as an example for a medium-volume compact car. The austenitic stainless steel 1.4301, which had been tested in preliminary tests (P 242 Untersuchung der Herstellmöglichkeiten eines modernen Kraftstofftanks aus Stahl mit Hilfe hydromechanischer und hydrostatischer Umformverfahren, Order No. P 242, ISBN 3- 930621-78-9, Verlag und Vertriebsgesellschaft mbH, Düsseldorf), served as the material basis. In preliminary simulation work, promising forming processes, adapted process control and special tool design were investigated and selected. Finally, the upper shell of the tank was manufactured by deep-drawing 0.6 mm thick sheet metal. The geometrically much more demanding lower shell was successfully produced by single-stage hydromechanical deep drawing from 0.8 mm thick sheet metal. The tanks, which were joined to prototypes from the two half-shells using TIG welding, were then subjected to Volkswagen AG's factory-internal component tests. This showed that all necessary safety requirements could be fully met due to the material-specific high residual deformation capacity. Without further optimisation steps, a weight reduction of 1.7 kg or 20 % was achieved for the steel tank compared to the plastic version. In some cases, the wall thickness in steel is only one tenth of that in plastic, resulting in a filling quantity that is almost 3 litres or almost 4% higher. Based on these test results, it can be concluded that Stainless steels, and probably also other corrosion-protected steels, can be processed into geometrically very complex fuel tanks in conjunction with modern hydroforming processes and a process and material-appropriate design. Steel thus offers a highly topical alternative material for solving future environmental protection requirements for fuel tanks. STUDIENGESELLSCHAFT STAHLANWENDUNG e.V. Publication: 2001 Authors: Prof. Dr E. Friebe, Dipl.-Wirtsch.-lng. T.Langhammer, Dipl.-Ing. P. Corsten, ]}, Dr W. Homberg, Dipl.-Ing. A. Wellendorf, Dr A.t Birkert, Dr F. Trösken, M. Carl, Dr J. Krautschick, Dr P. Papaiacovou
available anytime
€20.00
excl. VAT
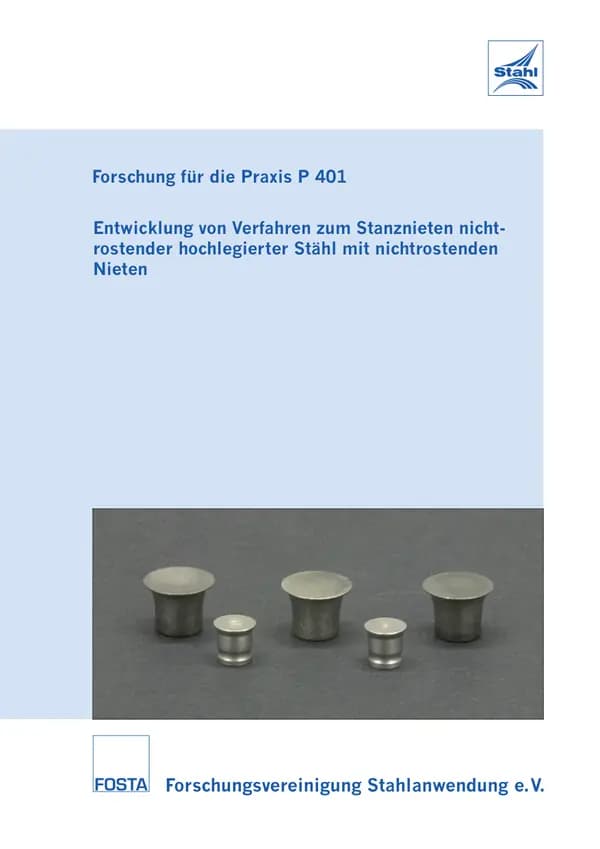
P 401 - Development of processes for self-pierce riveting of stainless high-alloy steels with stainless rivets High-alloy stainless steels are increasingly being used in the capital goods and consumer goods industries. The reasons for the growing use of this group of materials can be found in their technical properties. The main characteristics of stainless steels are corrosion resistance, heat and fire resistance, good mechanical and physical properties, favourable processing properties, attractive appearance, germ-repellent hygienic surfaces, environmental friendliness and recyclability. The combination of many of these properties in one material is what makes stainless steels so attractive. steels. Productivity advances have made it possible to reduce the price of the most commonly used material 1.4301 over the last 20 years. The use of stainless sheet materials is increasingly being favoured in various areas of sheet metal processing. The corrosion properties, but also the good forming properties, particularly when using austenitic grades, play an important role here. Resistance spot welding and roll seam welding are successfully used in the processing of stainless sheet steel materials. Although the critical temperature ranges are passed through very quickly, the heat input during joining can have a detrimental effect on corrosion resistance. The occurrence of annealing colours, which have a negative effect on the visual appearance and corrosion resistance, is countered by the use of shielding gas or, more frequently, by reworking using pickling or grinding. This reworking considerably increases the cost of the joint and should no longer be necessary if the joining technology used in this project is utilised. The use of self-pierce riveting processes, in particular semi-tubular self-pierce riveting processes, has so far largely been considered impractical for stainless steel sheets. This is not least due to the fact that there was no rivet on the market in the field of semi-tubular self-pierce riveting technology that enabled the processing of stainless steel materials as a stainless rivet. The project created the basis for describing the self-pierce riveting processes in terms of their processing properties when using stainless steels. Results have been compiled for the user which provide information on the reliable processing of stainless steels with stainless self-pierce rivets for the design of a joining device and work with the setting unit. Furthermore, characteristic values are provided that describe the load-bearing behaviour of these joints. The investigations demonstrated that stainless self-pierce rivets can be produced using methods comparable with industrial standards and can be processed in combination with stainless sheet materials. The research project was carried out at the Laboratory for Materials and Joining Technology at the University of Paderborn, at the Department of Mechanical Engineering - Automation Technology, South Westphalia University of Applied Sciences, Soest department and at ThyssenKrupp Nirosta GmbH, Krefeld, with technical support and financial assistance from the Forschungsvereinigung Stahlanwendung e. V., Düsseldorf, with funds from the Stiftung Stahlanwendungsforschung, Essen. Authors: O. Hahn, W. Flügge, A. Schulz Beenken, J. Schulte, S. Schuberth Publication: 2009
available anytime
€36.00
excl. VAT
Payment by card (Stripe) or invoice (DE, AT, CH). Download link by email: automatically after ordering by card, after order approval for invoice (valid for 30 days). Terms