
FOSTA
Highly porous materials with a cellular structure are characterised by their low specific weight and high stiffness. The little known fact that metals with a cellular structure can also be produced is the basis of …
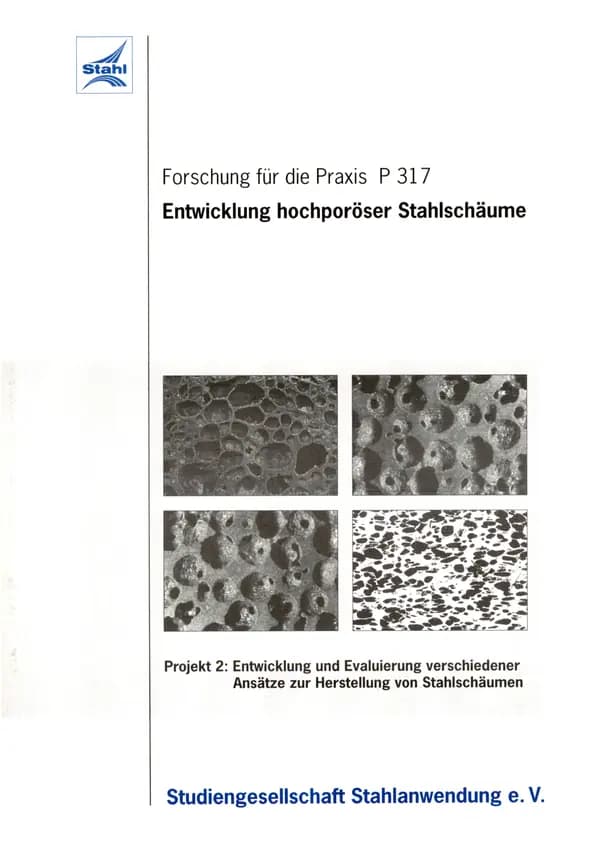
Highly porous materials with a cellular structure are characterised by their low specific weight and high stiffness. The little known fact that metals with a cellular structure can also be produced is the basis of numerous research approaches to produce lightweight materials. Recent developments in the field of metal foams prompted the Studiengesellschaft Stahlanwendung e.V. and the two research participants in Bremen and Aachen to investigate the production possibilities and areas of application of highly porous steel materials. Closed-cell steel foams can be produced by transferring the "blowing agent process", which is already used for low-melting-point metals on a semi-industrial scale.
Promising results have been achieved with the research work for iron-carbon alloys, which have yet to be transferred to high-alloy steel grades. Three different processes have been investigated for the production of open porosity in steel foams, namely working with spacer materials, reaction sintering of iron and aluminium powders and foaming of MIM feedstock. The investigated possibilities of producing steel foam by powder metallurgy have proven to be promising: The production of larger volumes of material is the next task for further research. Melt metallurgical processes for the production of highly porous iron-based foams have also been investigated. According to the available findings, it appears difficult to produce closed-pored structures. On the other hand, it is possible to produce open-pored steel foams by recasting spacer materials or using the investment casting process. Further development of the test equipment used will make it possible to produce larger sample volumes in the future. Particularly in view of the prospective market study that precedes the present investigation, the production of open-pored structures of steel foams appears to be very promising. After the encouraging first step within the framework of a study to identify innovative fields of application for steel foams, the research results presented here have shown concrete possibilities for the production of closed-pore and open-pore steel foams on a laboratory scale, so that the step towards the semi-industrial production of larger steel foam volumes can now be tackled. STUDIENGESELLSCHAFT STAHLANWENDUNG e.V.
Machine-translated title and description. The document itself is in German.
Payment by card (Stripe) or invoice (DE, AT, CH). Download link by email: automatically after ordering by card, after order approval for invoice (valid for 30 days). Terms
Digital download
Other parts and editions as well as neighbouring documents of the same series.
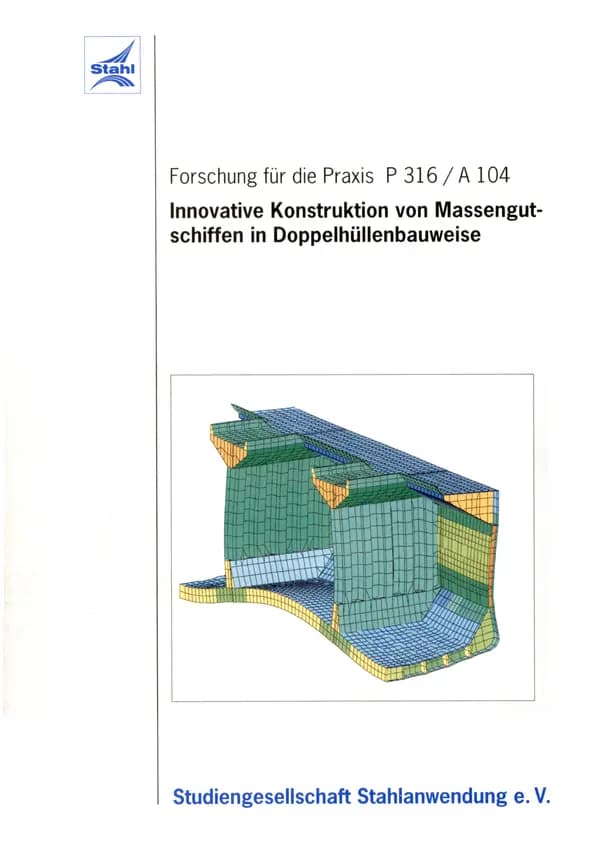
P 316: Innovative construction of bulk carriers in double-hull design In view of the high average age of the bulk carrier fleet of over 17 years - with a normal service life of 20 to 25 years - this type of ship is definitely of interest to the German and European shipyard industry if innovative solutions can be found to compensate for the cost disadvantage compared to international, particularly Asian, competitors. In the present research project, the constructive development of a bulk carrier in double-hull design has been analysed for an optimal solution with critical consideration of different variants. The prototype development is intended to create the conditions for a quick and targeted response to specific enquiries without the need for time-consuming preliminary investigations. As part of the innovative approach, this type of ship was also to be used as an example to investigate the extent to which new steel materials, semi-finished products and production methods can be used to improve quality and ensure competitiveness. The project was applied for by Germanischer Lloyd, Hamburg, and Flensburger Schiffbaugesellschaft at the Studiengesellschaft Stahlanwendung e.V. and the Forschungsvereinigung der Arbeitsgemeinschaft der Eisen und Metall verarbeitenden Industrie e.V. (AVIF) - through the Forschungszentrum des Deutschen Schiffbaus e.V. (German Shipbuilding Research Centre). Germanischer Lloyd is an internationally active organisation for the classification of ships of all kinds. Flensburger Schiffbaugesellschaft is a medium-sized shipyard that builds a wide variety of ship types up to a carrying capacity of approx. 80,000 tonnes. The research and development specialists from the above-mentioned companies were assisted by materials specialists from the steel industry (AG der Dillinger Hüttenwerke, Krupp Hoesch Stahl AG, Preussag AG, Stahlwerke Bremen GmbH and Thyssen Stahl AG); in addition, experts from the production technology sector were also involved. The solution developed was finally subjected to an economic efficiency comparison, which also included the operating costs including the expected maintenance and repair costs. The shipping company Egon Oldendorf, Lübeck, which operates in the bulk shipping sector, was involved in this analysis. The result shows an advantage for the research result with a long service life. On the basis of a 75,000 tdw bulk carrier, the conventional design with a single outer skin on the sides of the ship was compared with several constructive variants of the double-hull design. The elaboration of the designs showed that the steel weight and thus also the load-bearing capacity is almost the same for the different variants. In the case of the conventional design, the planned, internationally agreed additional requirements with regard to strength in the event of a leak have already been taken into account. A minor disadvantage of the double-hull design is the slightly smaller cargo hold volume and the somewhat higher construction costs. Apart from the positive safety aspects, there are clear advantages, especially during the operating time. A profitability calculation showed that the cleaning costs after unloading and maintenance costs in particular are lower for the double-hull bulker. In addition, better availability and a higher residual value can be assumed. A net present value calculation, assuming realistic cost estimates, showed that overall the double-hull design is the more economical option. However, a novel idea with a shell-shaped inner hull on the sides of the ship proved to be too heavy and too expensive, although there may be further potential for optimisation. Based on the results for the other variants of the double-hull bulker, however, it can generally be stated that it is not only aspects of ship safety and component redundancy that speak in favour of a fundamental change in the design of bulk carriers. In addition to the design and constructional elaboration and economic feasibility study of the different variants, the project also analysed aspects of the use of materials, production and the improvement of the strength and corrosion resistance of the inner bottom. It is to be expected that in the latter - apart from the transverse bulkheads - most mechanical damage and corrosion phenomena will occur in a double-hull bulker, so that the service life of the structure will be decisively influenced by innovative solutions. STUDIENGESELLSCHAFT STAHLANWENDUNG e.V. Publication: 1998 Authors: Dr.-Ing. W. Fricke, Dipl.-Ing. R. Nagel
available anytime
€30.00
excl. VAT
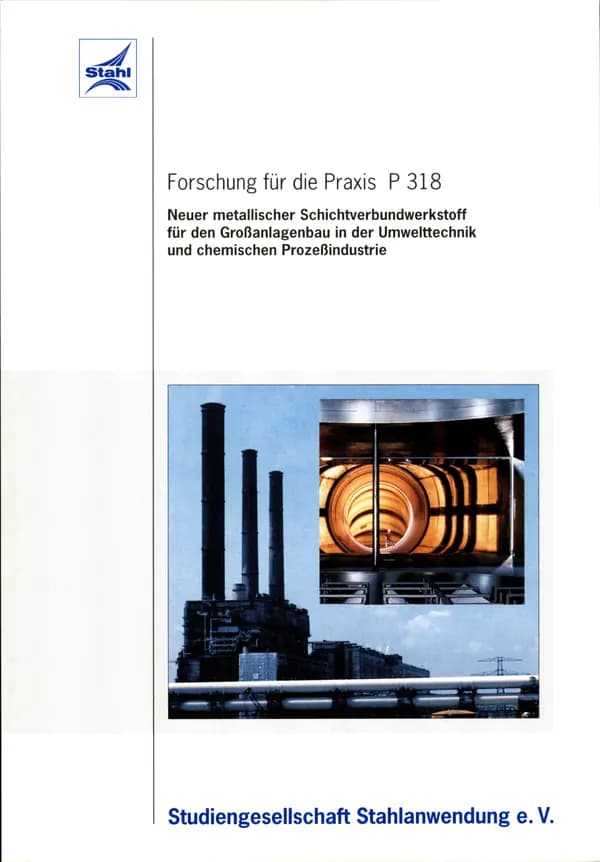
P 318: New metallic layered composite material for large-scale plant construction in environmental technology and the chemical process industry The aim of the research project presented here was the production and process engineering qualification of a new highly corrosion-resistant metallic layered composite material based on steel, to which a nickel-based alloy with a sheet thickness of around 1 mm was bonded as a corrosion-resistant coating. This made it possible to provide a more cost-effective alternative to organic-based corrosion protection systems, which is characterised by the technical advantages of a metallic design - such as high corrosion resistance and wear resistance. This solution was made possible by the operationally secured provision of 1 mm thick Ni-based alloy sheets and strips. This research report describes the requirements profile for the new metallic bonded laminated composite material from the perspective of manufacturers, users and processors. It also provides an overview of the characterisation of the adhesives and adhesive technology used on a laboratory and industrial scale. The bonded metallic layered composite material proved its resilience under various practical ageing stresses. In addition to answering processing-related questions such as cold formability or plasma cutting, a non-destructive testing method was developed for the bonded metallic layered composite on an ultrasonic basis. Practical findings on the cold formability of the bonded metallic layered composite material were underpinned by FEM calculations. The weldability of the bonded metallic layered composite material was investigated to a large extent under workshop and construction site conditions. The positive results obtained in the laboratory and workshop with the bonded metallic layered composite material were confirmed in field tests under practical conditions. Furthermore, the field tests described above demonstrated that the results obtained also provide a technically manageable and cost-effective concept for the metallic restoration of damaged rubber coatings, organic coatings or GRP components in environmental engineering. The layered composite material has been included in the processing range of a major German plant manufacturer; the apparatus and reactor construction company has thus expanded its range of materials. On the basis of the adhesive bonding technology developed for operational use, repair offers have been submitted for two cases of damage (metallic cleaning channel and organically internally coated flue gas stack), which the operators have to decide on when awarding contracts for the necessary repairs to corrosion damage. STUDIENGESELLSCHAFT STAHLANWENDUNG e.V. Publication: 2000 Authors: Dr rer. nat. I. Rommerskirchen
available anytime
€20.00
excl. VAT
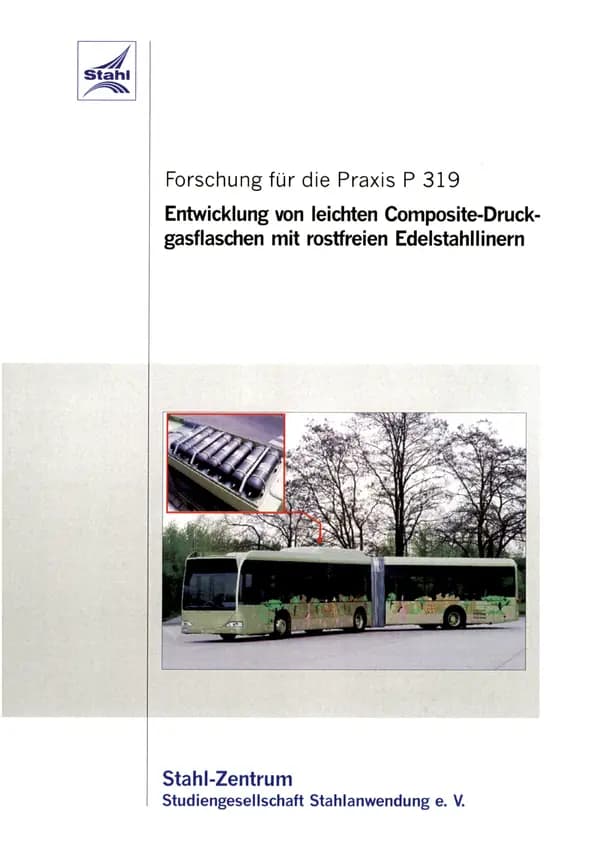
P 319: Development of lightweight composite pressurised gas cylinders with stainless steel liners The use of gaseous fuels for the operation of vehicles is becoming increasingly important. As these should be as light as possible in order to reduce fuel consumption or increase the range, weight-optimised compressed gas cylinders are required. The aim of the research work was to further develop corresponding steel-based composite tanks with carbon fibre wrapping. This is associated with the expectation of increased acceptance of gas-powered vehicles and a more favourable use of energy resources from an ecological point of view. Initial attempts to reduce the wall thickness by using higher-strength variants of the steel 34CrMo4 (1.7220) introduced in pressure vessel construction by modifying it with titanium and boron were not successful. Sufficient safety against stress corrosion cracking could not be demonstrated. Attempts to strengthen welded steel liners made of austenitic material were also unsuccessful. When using the steel grade X5CrNi18-10 (1.4301) with a wall thickness of 1.3 or 1.7 mm, premature failure occurred in the internal pressure swelling tests, which are important for an acceptance procedure, due to the early formation of fatigue fractures starting from the longitudinal or circumferential weld seams of the liner. The greater elastic elongation of the carbon fibre winding compared to steel and the reduced yield point heat-affected zone of the TIG weld seam caused alternating plasticisation of the seam area and triggered premature leakage there. Replacing conventional circumferential welds with laser welds was also unable to sufficiently improve the swelling behaviour. In addition, an edge offset in the circumferential weld area, which could only be avoided by cost-intensive measures, prevented a positive test result. Only the third approach, using cryo-stretched, austenitic stainless steel liners made of X2CrNi19-11 (1.4303) steel, finally showed the possibility of a technically and economically favourable solution. The entire liner, including the longitudinal weld seam, is highly strengthened by cryoforming. Carbonisation tests on this core container variant showed that the service life requirements can be met without restriction. As a result of the work, a weight reduction of approx. 20 % and reliable control of the material behaviour, e.g. avoidance of fatigue cracks and corrosion phenomena, should be emphasised. By optimising the fibre composite and core container wall thickness, a further weight reduction of > 50 % compared to solid steel cylinders is possible according to current knowledge. These results open up promising application possibilities for steel as a material, even with further increased requirements for pressurised gas containers, e.g. for vehicles powered by natural gas. STUDIENGESELLSCHAFT STAHLANWENDUNG e.V. Publication: 2002 Authors: Dipl.-Ing. G. Junker
available anytime
€20.00
excl. VAT
P 312 - Development of a rotating arc sensor system for the detection and processing of joint shape and geometry when welding sheet steel When stiffeners (Holland profiles, flat bars, etc.) are mounted on panels and sheet metal, component tolerances, bevelled cut edges (plasma cut) or curves at the base of the profile, etc., result in tolerances in the joint preparation for subsequent fillet welding. Tolerances in the joint preparation for the subsequent fillet weld. Differing air gaps between the profile and the sheet, insufficient squareness and seam runs that deviate laterally from the nominal contour make the use of automatic welding systems difficult. The welding robots previously used at Howaldtswerke - Deutsche Werft AG (HDW) in micro-panel production and in double bottom production (Hall 4 and Hall 10) are equipped with an arc sensor system. By oscillating the welding torch transversely to the welding direction, the centre of the fillet is detected and tracked due to the different arc lengths and thus changing welding voltages. The disadvantage of this arc sensor system is that the performance of the welding process cannot be fully utilised due to the oscillation. Above certain process parameters, melting notches occur on the web and the appearance of the seam deteriorates. Attempts to weld more powerful cored wires with this sensor system show this phenomenon to an even greater extent. Further disadvantages are that expensive pulse welding power sources are also required for the conventional MAG welding process and that the permanent pendulum movement leads to wear in all torch axes. In order to avoid the transfer of the oscillation to the entire gantry, very complex and expensive welding gantry supports have been designed. Until now, it has not been possible to measure the air gap and make corresponding corrections in the welding process to avoid welding fillet welds of different thicknesses. The industry therefore looked for more elegant sensor systems to eliminate or minimise the disadvantages mentioned. The Institute for Welding Manufacturing Processes (ISF) at the RWTH Aachen University has conducted orientation tests with an arc sensor system with a rotating deflected wire electrode. Following detailed information from the ISF and demonstrations in a laboratory test, the following tasks were formulated for the present project. An arc sensor system is to be developed for a MAG welding robot that works with a welding torch with a rotating, deflected wire electrode and is able to generate control variables for seam tracking, fill level control and torch orientation from the signals from the welding process. The system is also to be equipped with corner detection. Publication: 1998 Authors: Dr.-Ing. D. Hinneberg
available anytime
€40.00
excl. VAT
Payment by card (Stripe) or invoice (DE, AT, CH). Download link by email: automatically after ordering by card, after order approval for invoice (valid for 30 days). Terms