The project P 1427 / IGF-No. 21112 N "Lifetime prediction for steel bonded joints under multiaxial loading with phase shift, variable mean stress and variable amplitudes LAMbdA" aims to efficiently and reliably estimate …
The project P 1427 / IGF-No. 21112 N "Lifetime prediction for steel bonded joints under multiaxial loading with phase shift, variable mean stress and variable amplitudes LAMbdA" aims to efficiently and reliably estimate the lifetime under these complex loads. To achieve this goal, bonded joints with steel substrates and two structural epoxy-based adhesive systems are being investigated: SikaPower 480 (EP1, unmodified system) and Betamate 1496 V (EP2, toughened system). The tests carried out as part of the project were performed at room temperature. To characterise the fatigue behaviour of the structural adhesives, basic tests were carried out on butt-bonded double pipe samples under cyclic pure tensile, pure torsional and multi-axial loading (tensile-torsional).
To validate the prediction approaches, fatigue tests were carried out on bonded samples with an inhomogeneous stress state in the bonded layer. The following specimens were selected as representative specimens: the flanged round bar specimen (EP1) and the L-shaped specimen (EP2) with constant amplitude and the cup specimen (EP1, EP2) with variable amplitude. At constant amplitude, baseline and validation tests showed that (i) the lifetime decreases with increasing mean stress and (ii) the variation of the phase shift does not significantly influence the lifetime. With variable amplitude, however, both the mean voltage and the phase shift had an influence on the service life. Lifetime prediction approaches were developed on the basis of the experimental results. For cyclic loading with constant amplitudes, both invariant-based (BELTRAMI criterion) and critical-plane-based approaches (FINDLEY criterion) were used. Furthermore, a hybrid concept considering stress anisotropy was developed. For cyclic loading with variable amplitude, a multiaxial counting method was combined with an invariant-based failure criterion. The linear damage accumulation according to Palmgren and Miner proved to be expedient. A rheological material model with damage for predicting the service life of bonded joints within the framework of continuum damage mechanics was extended to include the investigated influences and validated using the test results. The model parameters for the rheological model were determined using uniaxial test data series after the modelling had been completed. The rheological model was implemented in FEA for the prediction of a component-like sample. Satisfactory accuracy of the service life estimation was achieved with the developed approaches. The determination of characteristic values is based on uniaxial tests on simple samples with a simple geometry, which significantly reduces the implementation hurdle and the costs for parameter identification for SMEs. The results obtained provide practical added value for those involved in adhesive bonding technology with regard to the service life prediction of bonded steel joints under complex stress conditions with constant and variable amplitude. The objective of the research project was achieved.
Payment by card (Stripe) or invoice (DE, AT, CH). Download link by email: automatically after ordering by card, after order approval for invoice (valid for 30 days). Terms
Machine-translated title and description. The document itself is in German.
Digital download
Other parts and editions as well as neighbouring documents of the same series.

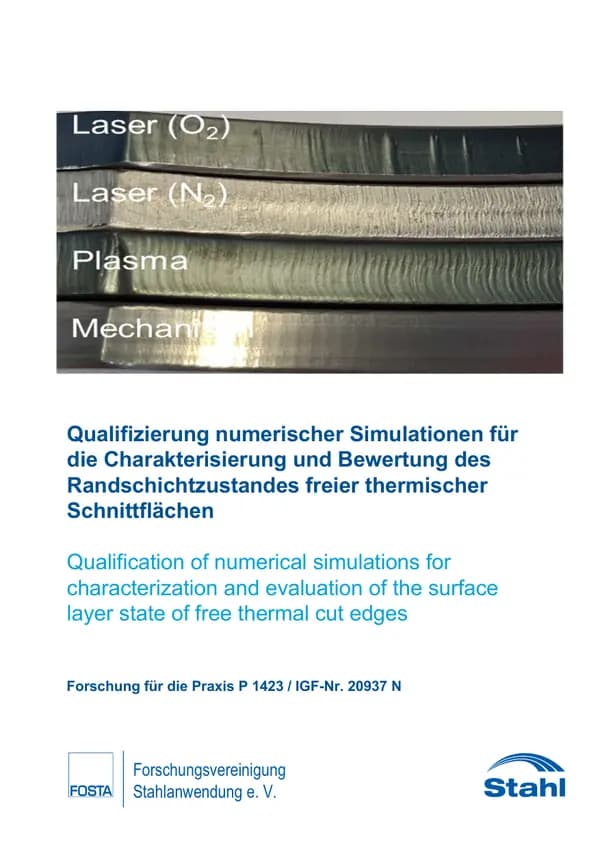
P 1423 - Qualification of numerical simulations for the characterisation and evaluation of the boundary layer condition of free thermal cut surfaces As part of the research project "Qualification of numerical simulations for the characterisation and evaluation of the surface layer condition of free thermal cut surfaces", thermal cutting tests were carried out, the characteristic quality features were determined experimentally and compared with the results from the numerical investigations. For this purpose, the laser cutting process was selected as the main method and tests were carried out on a structural steel S355NC and a high-strength steel S1100M. It can be seen that the hardness integrity value of DIN EN 1090 is clearly exceeded with S1100M and that the maximum hardness of around 570 HV1 is not directly at the cutting edge. It drops to around 480 HV1 to 520 HV1 up to the surface. A decreasing carbon content at the cutting edge could be one reason for this. In comparison to the numerical investigations, the following points can be determined: The dimensions of the heat-affected zone can be determined via the numerical calculations and are in good agreement with the micrographs. The phase fractions at the low cooling rates indicate a complete transformation into martensite at the surface layer. The maximum hardness of the HAZ agrees with the experimental results. The hardness distribution over depth in relation to the HAZ is in good agreement. Deviations in the width of the HAZ are very small. The results show that the cutting process can be modelled by numerical simulation and that the surface layer condition can be evaluated after the cutting process. The microstructure, the maximum temperatures and the hardness distribution can be determined and thus offers the possibility of saving time and costs when determining the quality of thermal cutting edges. The effort required to create the numerical models must be put into perspective here and the method must be accepted in quality testing. The aim of the research project was achieved. Publication: December 2022 Authors: M. Sc. P. Diekhoff, Dr.-Ing. J. Sun, Dr.-Ing. T. Nitschke-Pagel, Prof. Dr.-Ing. K. Dilger
available anytime
€30.00
excl. VAT

The additive manufacturing of metallic components using the DED-Arc process is becoming increasingly important in the industry due to the technical, ecological and economic advantages resulting from the process-specific features. Innovative process strategies are continuously expanding the economically relevant areas of application. In this way, even expensive materials for the high-tech sector such as high-alloy steels or non-ferrous alloys can be processed in a resource-saving and reliable manner using the DED-Arc process. However, high-alloy steels in particular generally have very low thermal conductivity and a high heat capacity, which has a number of negative effects on the additive manufacturing process. This can lead to an increase in construction time or a reduction in the strength of the resulting components. Additional component cooling can be implemented in order to further increase economic efficiency by reducing the required build time and adjusting the cooling rates relevant for microstructure formation. The aim of this research project was therefore to develop a strategy for efficient component cooling and for controlling component properties in the arc-based additive manufacturing of austenitic steels and super-duplex steels using active gas cooling. The research initially focused on the conception and design of cooling nozzle concepts that can be implemented as easily as possible in conventional welding technology and can be used flexibly in the additive build-up process using DED-Arc. With the support of flow simulations, the design of the nozzles and the selection of the most suitable variants for the experimental investigations were carried out on the basis of defined criteria relevant to the welding process. Seven selected cooling gas nozzle concepts were then analysed experimentally using simple and complex additive applications. An essential part of the investigations was the interaction of the cooling gas flow with the shielding gas flow and ultimately the shielding gas coverage at the arc position or at the arc itself, which was quantified by measuring the oxygen content. For this purpose, both cold gas tests (without arc) and hot gas tests (with arc) were carried out by varying the type of cooling gas and the results were compared with each other. Depending on the cooling gas nozzle used and the respective application, maximum cooling gas flow rates were determined that enabled an additive build-up process without significantly influencing the shielding gas coverage. Finally, the test results were validated by comparative structural welds and suitability for use in the additive build-up process using DED-Arc was assessed and derived. In the final step, large-volume wall structures were generated with selected cooling nozzle variants. Depending on the line energy and the cooling gas composition, a reduction in the build-up time and a positive influence on the mechanical properties were achieved. The objective of this research project was accomplished. Published in: 2026 Authors: M.Sc. M. Gierth, M.Sc. S. Eichler, Dr.-Ing. J. Hildebrand, Univ.-Prof. Dr.-Ing. habil. J. P. Bergmann
available anytime
€30.00
excl. VAT

P 1418 - Profile straightening by partial rolling during roll forming As part of the AiF project with the number 20960N, a new and efficient method for straightening defective profiles is being investigated for the established mass production process of roll forming. The aim of the project is to determine the relationship between the longitudinal strain distribution and the profile defects. Based on these findings and the relative longitudinal strain distributions, countermeasures are to be introduced in order to straighten profiles by partially rolling out selected cross-sectional areas. In the first work package, the influencing variables that affect profile defects and longitudinal strains during roll forming are identified. In the second work package, the preparations for numerical modelling and preliminary experimental investigations such as material characterisation are carried out. In the third work package, numerical investigations are carried out on the U and hat profile. Based on the numerically obtained findings on the longitudinal strain curves, partial rolling is investigated. To determine the influence of various parameters on the method of partial rolling, investigations are carried out for both the U-profile and a hat profile. In particular, an asymmetrical geometry is used, as in this case there is a superposition of vertical and horizontal deflection as well as torsion. In parallel, experimental investigations with properties equivalent to the numerical models are carried out for validation. Subsequently, partial rolling for straightening is investigated experimentally. In the first step, partial rolling is applied to the U-profile and then continued with the hat profile. The profile errors can be eliminated by the new method for both the U-profile and the top-hat profile. Equivalent to the numerical and experimental investigations, an analytical calculation model is set up to determine the longitudinal strain distribution based on the profile errors that occur. This analytical calculation model is validated with the numerically determined results for both profiles from the simulation models. The final step is the implementation of the novel method for industrially used profiles. Experimental and numerical investigations are carried out with a complex profile from a project partner. The measured profile errors for the roll-formed profiles are influenced by applying partial rolling and prove that profile errors can also be influenced for more complex geometries. The aim of the research project was achieved. Publication: March 2023
available anytime
€30.00
excl. VAT

P 1416 - Extension of the areas of application of hot-dip galvanised steel components in combination with beam welding processes The aim of the project was to extend the range of applications for hot-dip galvanised components and to increase the cost-effectiveness of infrastructure projects through the advantages of laser beam welding in a vacuum (LaVa). The aim of this study was to determine the extent to which laser beam welding is suitable for joining large hot-dip galvanised components. The key point here was to first galvanise and then weld the components by modifying the process, which is only possible with laser beam welding in a vacuum. The motivation of the project was therefore to model the welding and galvanising process as precisely as possible and to validate the numerical models. It was found that the combination in the new process sequence produces favourable residual stress states. A further objective was to optimise the welding process, including the prevention of contamination of the coupling window of the vacuum chamber and the development of integrated corrosion protection. This serves as an alternative to thermal spraying. Subsequently, welds and tests were carried out on components from different process chains in order to investigate the occurrence and influence of residual stresses. The results of the welding investigation show that the joining of galvanised sheets up to 20 mm sheet thickness with zinc up to 200µm in the joining gap is only possible to a limited extent, whereas solid welded joints can be produced in accordance with the standard up to sheet thicknesses of 40 mm when welding without zinc in the joining gap, only on the surface with up to 400µm. The limited weldability is shown by the fact that the weld seam has a pronounced seam collapse, as there is no material in the joint gap due to the evaporating zinc. A model was developed and validated from experimental tests and their numerical calculations. This allowed the stress and strain states after galvanising, laser welding and their combination to be investigated. It was found that the thermal process does not leave any noticeable restrictions in the component after the production steps. Due to the restrictions imposed by the joining process on butt joints, only these can be considered validated for the time being. Fillet welds and other welded joints should therefore be considered in future investigations. The aim of the research project was achieved. Publication: June 2024 Authors: R. Kühne, Dr.-Ing. H. Bartsch, Ch. Frey, Dr.-Ing. S. Olschok
available anytime
€30.00
excl. VAT
Payment by card (Stripe) or invoice (DE, AT, CH). Download link by email: automatically after ordering by card, after order approval for invoice (valid for 30 days). Terms