Increasingly stringent regulations on work ergonomics, rising transport costs and general efforts to reduce logistics costs mean that lightweight materials must be used in load carrier construction. The aim of the …
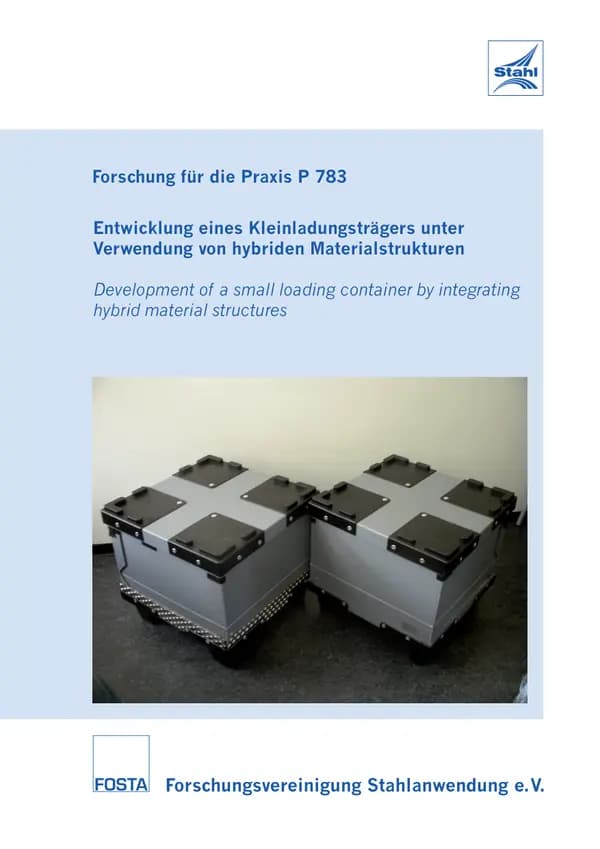
Increasingly stringent regulations on work ergonomics, rising transport costs and general efforts to reduce logistics costs mean that lightweight materials must be used in load carrier construction. The aim of the project was therefore to combine conventional load carriers, which have high requirements for lightweight construction and stability, with the help of the new honeycomb panels made of sheet steel, which fulfils the two generally divergent requirements (weight reduction and stability). In a further step, the use of honeycomb panels in general logistics applications was also investigated in order to determine possible optimisation approaches using lightweight materials.
The following criteria were identified in the project, which are required for the use of honeycomb panels in load carrier construction. The target system consists of maximum flexibility in handling, processing and size while minimising costs. In particular, the limited panel size is currently the biggest obstacle to further optimisation approaches in logistics through the use of honeycomb panels. The construction of a model prototype carried out in the project clearly demonstrated that honeycomb panels can physically compensate for the weak points of current materials in lightweight load carriers, particularly through hybrid solutions, and can therefore clearly lead to optimisation. The use of honeycomb panels in existing standard load carriers - without physical weaknesses - could also lead to optimisations in these, in that stable but heavy solutions can be optimised to the extent that they could be "lightened" by a significant amount while maintaining the same stability (example: lattice box, steel GLT of the Institute of Materials Handling and Logistics, etc.). In addition, the use of honeycomb panels as a substitute for Apitong wooden flooring in container construction can offer considerable potential, provided honeycomb panels can withstand the stability requirements of ISO containers. The two logistics sectors of air freight containers and swap bodies could provide further fields of application. With all the optimisation potentials described, a profitability calculation must be carried out in each individual case to determine the extent to which the use of honeycomb panels instead of the previous solution would lead to a cost improvement for the user. In many cases, higher material costs for the honeycomb panels could be offset by savings, for example through a reduction in weight (in air and land transport, where transport prices are generally based on the weight of the consignment) or, for example, by increasing stability (reduction in maintenance costs, reduction in repair costs, increase in process reliability - less costly safety infrastructure required) or even generate a positive ROI compared to previous solutions. In conclusion, it can be stated that the practical usability of honeycomb panels - in particular the limited dimensions of the panel size - must be further advanced in order to be able to tap optimisation potential in logistics - ultimately also proven by economic efficiency calculations. The research project was carried out at the Institute for Materials Handling and Logistics at the University of Stuttgart with technical support and financial assistance from FOSTA - Forschungsvereinigung Stahlanwendung e. V., Düsseldorf.
Payment by card (Stripe) or invoice (DE, AT, CH). Download link by email: automatically after ordering by card, after order approval for invoice (valid for 30 days). Terms
Machine-translated title and description. The document itself is in German.
Digital download
Other parts and editions as well as neighbouring documents of the same series.

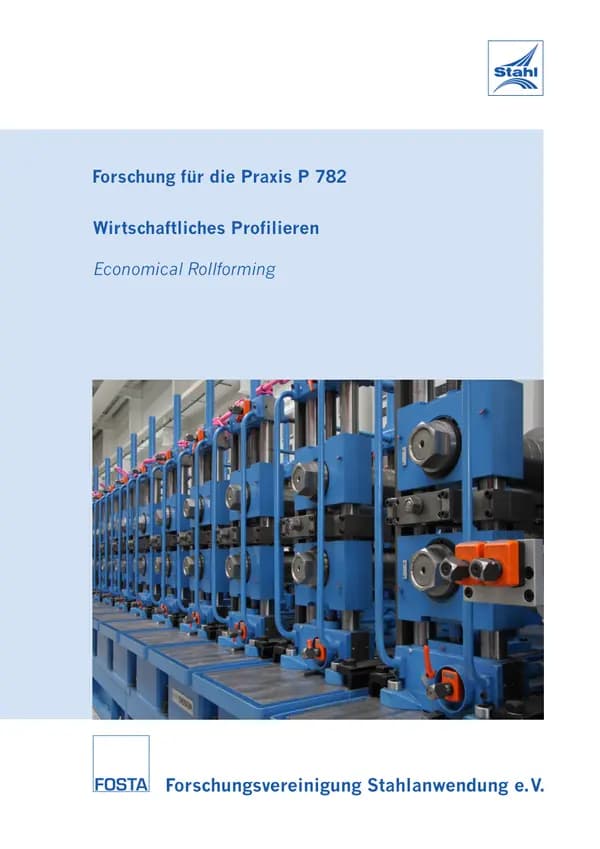
P 782 - Economical profiling in automotive engineering Roll-formed components made from steel materials can be found in a wide range of applications. Products with a wide range of cross-sections can be manufactured cost-effectively in large quantities. This is partly due to the fact that production is carried out continuously from coiled sheet metal strips. Rolled profiles are also used in the automotive industry, although production using discontinuous manufacturing processes such as deep drawing still predominates. However, car manufacturers are interested in increasing the use of roll forming, particularly for the production of structural components. The aim of the study was to investigate the conditions under which the production of steel profiles using roll forming appears to make sense. To this end, a reference component was used to illustrate the possibilities and restrictions offered by roll forming with regard to the range of shapes and the integration of functionality. Furthermore, an economic comparison was made between roll forming and deep drawing for the reference component. The entire production process chain was considered. A vehicle sill was selected as the reference component, which was to be produced in different variants and quantities. The materials also differed. In addition to a standard deep-drawing steel, a high-strength steel grade was included in the investigations. In the scenarios analysed, the components were equivalent, i.e. with comparable properties, and could be produced both by roll forming and deep drawing. In terms of cost-effectiveness, there was only a slight cost advantage for the large series components (one million components per year in each case) of the components to be produced by roll forming compared to the pressed parts, as the comparatively high costs of the deep-drawing tools can be passed on to a large number of units. For small series, however, there were clear advantages of 30 - 40 % in favour of roll forming. This is primarily due to the low tool costs, which were not cancelled out by the longer changeover times for roll forming. The research project was carried out at the Institute for Production Engineering and Forming Machines, Technical University of Darmstadt, with technical support and financial backing from the Forschungsvereinigung Stahlanwendung e. V., Düsseldorf. Authors: P. Groche, P. Götz, R. Salomon Publication: 2009
available anytime
€20.00
excl. VAT

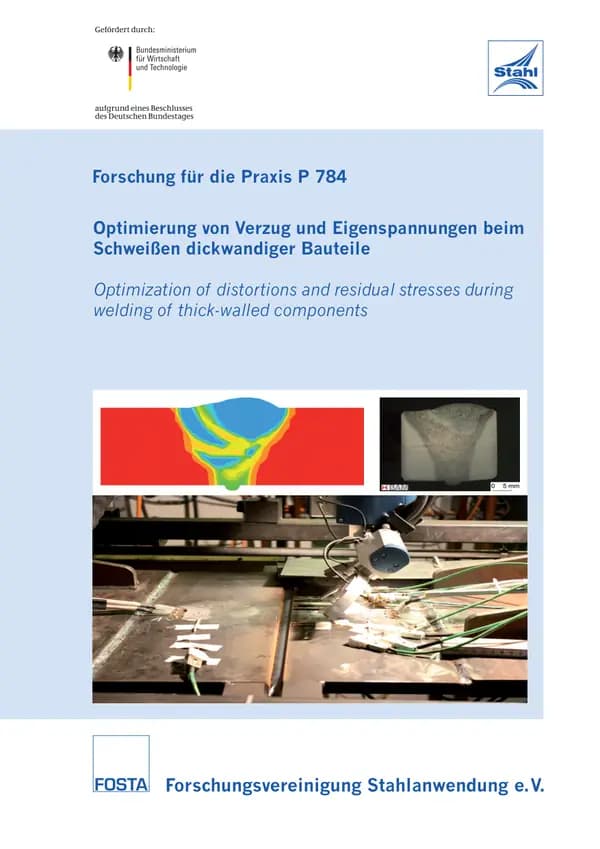
P 784 - Optimisation of distortion and residual stresses when welding thick-walled components The welding simulation of thick-walled components places high demands on commercially available welding simulation software due to the increased complexity of the thermophysical and thermomechanical processes involved in multi-layer welding. This includes the distortions and residual stresses induced in the finished component during the joining process, which are of great importance for assessing the production quality. In thick-walled components in particular, the stress state is extremely complex due to the structural rigidity of the individual components and the entire assembly as well as due to additional external clamping devices during production. In addition, in the case of materials with phase transformation, there are the metallurgically induced stress states and, in the case of multi-layer welded joints, the repeated thermal and transformation-related stress formation, so that a rough estimate of the overall deformation and stress state is generally no longer possible, even for experts. However, the prevailing deformations and stresses significantly determine the inherent stress of the welded structure and thus its load-bearing capacity in operation. Precise knowledge of this data would provide valuable information for optimising the quality of the end product. The aim of the project was to investigate, evaluate and predict welding-related distortions and residual stresses in multi-layer welds on unalloyed structural steel S355J2+N. The aspects of phase transformation and tempering behaviour were at the heart of the numerical investigations. The results of the analyses carried out were to be used to optimise distortion and residual stresses when welding thick-walled components. Furthermore, the practicability and applicability of the finite element software used with regard to realistic modelling of the processes taking place, computing time and user requirements were always the focus of the project. The increasing complexity of the investigations, from the single-layer weld sample to the four-layer welded test sheet with high component analogy, ensured the analysis of geometric influences (sheet length, tacking points, lead-in and lead-out sheets) and phase transformations on the numerical calculation of welding-induced residual stresses and distortions. Potentials for optimising the calculation of residual stresses and distortions in connection with the transformation behaviour were shown. In addition, the possibilities of welding simulation for the prediction of residual stresses and distortion as well as for the sensitivity analysis of relevant process variables, e.g. preheating or interpass temperature, are presented with the aid of a multi-layer model. The IGF project 15746 N of FOSTA - Forschungsvereinigung Stahlanwendung e. V., Düsseldorf, was funded at the Federal Institute for Materials Research and Testing (BAM), Berlin, via the AiF within the framework of the programme for the promotion of joint industrial research and development (IGF) by the Federal Ministry of Economics and Technology on the basis of a resolution of the German Bundestag. Authors: M. Rethmeier, C. Schwenk, C. Heinze, R. Salomon Publication: 2011
available anytime
€30.00
excl. VAT

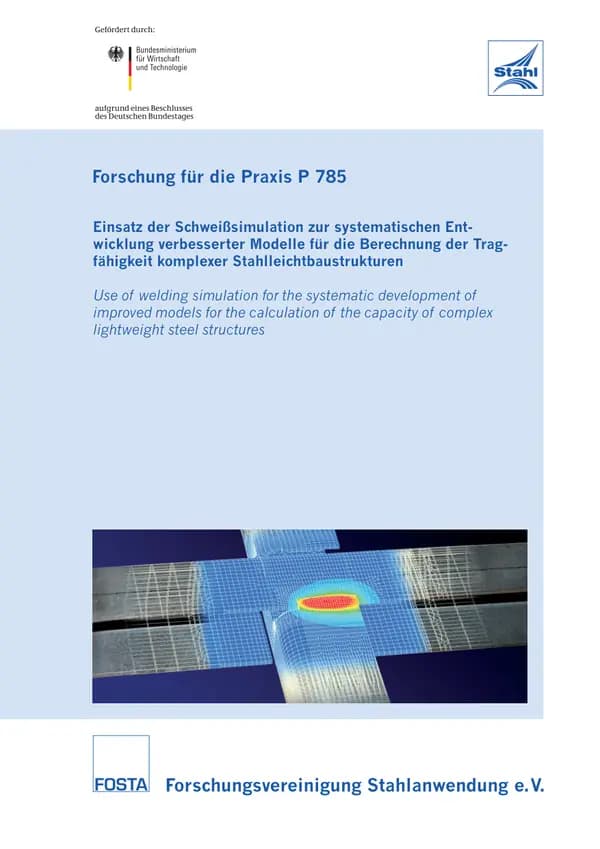
P 785 - Use of welding simulation for the systematic development of improved models for the calculation of the load-bearing capacity of complex lightweight steel structures Lightweight construction is also becoming increasingly important in the construction industry. The aim is to improve load-bearing functions without increasing weight. Improved load-bearing capacity can be achieved primarily through the skilful design of complex lightweight steel structures. The aim of the research project was to improve the calculation of the load-bearing capacity of complex lightweight steel structures using the example of truss and corrugated web beams. For this purpose, extensive geometric and physically non-linear FE load-bearing capacity analyses were carried out in the project. The derivation of engineering models and the development of proposals for practical design were a key focus of the investigations. Furthermore, load-bearing and deformation analyses as well as optimisation processes could be carried out on the virtual component, which saves costs for component tests and leads to significantly shorter development times. The basis for an improved load-bearing capacity verification is formed by the use of welding simulation and the consideration of local component properties that this makes possible. Welding simulations of the seams on the selected components were carried out at the Institute of Joining and Welding Technology at the TU Braunschweig. The results, such as the size of the heat-affected zone or the resulting residual stresses, were handed over to the Chair of Steel and Timber Construction at the BTU Cottbus for integration into the numerical load-bearing capacity calculation of large component structures. The results were used to derive simplified analytical formulae that enable a more precise calculation. The IGF project 287 ZBG of FOSTA -Forschungsvereinigung Stahlanwendung e.V., Düsseldorf, was funded by the Federal Ministry of Economics and Technology via the AiF as part of the programme for the promotion of joint industrial research and development (IGF) on the basis of a resolution of the German Bundestag. The project was carried out at the Institute for Joining and Welding Technology at the Carolo-Wilhelmina University of Technology in Braunschweig and at the Chair of Steel and Timber Construction at the Brandenburg University of Technology in Cottbus. Authors: K. Dilger, M. Vogt, M. Umer, H. Pastemak, V. Bachmann, G. Kubieniec Publication: 2013
available anytime
€40.00
excl. VAT

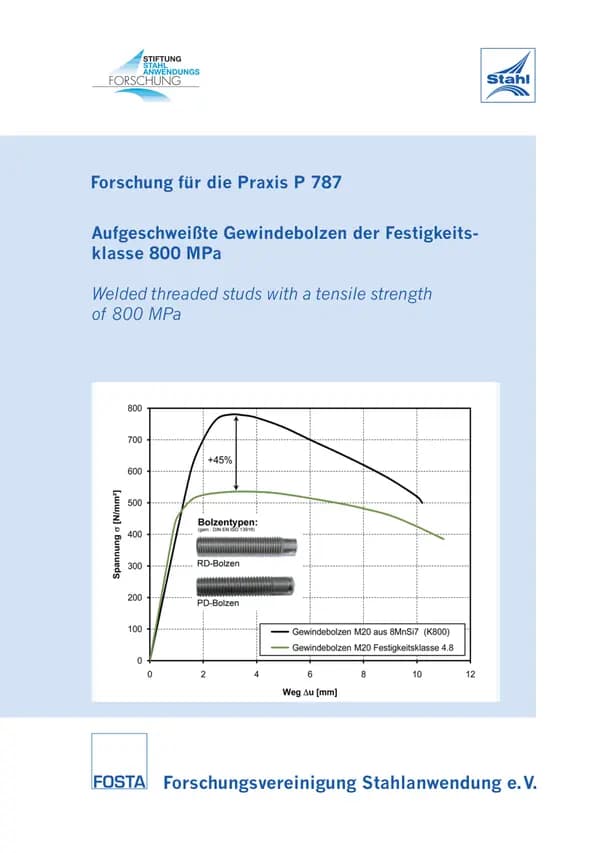
P 787 - Welded-on threaded studs of strength class 800 MPa Due to the joining process, welded-on threaded studs must be made of a material suitable for welding. For this reason, in addition to some austenitic steels, only steels of strength class 4.8 according to ISO 898-1 with a maximum carbon mass fraction of C = 0.20% are currently permitted for threaded studs. Steels of higher strength classes generally have a carbon mass fraction of C ≥ 0.20% and are therefore only conditionally weldable. In order to satisfy the market demand for threaded studs with higher strengths, stud manufacturers are currently turning to the cold heading steel 20MnB4 (1.5525), which roughly fulfils the requirements of strength class 8.8 thanks to thermal post-tempering. From a welding point of view, 20MnB4 with a carbon mass fraction of up to C = 0.23% can only be classified as conditionally weldable and, due to the additional costs for thermal tempering, bolts made of 20MnB4 have not been able to establish themselves on the market. Another alternative material is 8MnSi7 (1.5113), which also comes from the group of cold heading steels and which, with a carbon mass fraction of C = 0.10%, suggests good welding properties. The tensile strength of wire rod made from 8MnSi7 is between 520 and 620 MPa, but achieves tensile strengths of over 800 MPa due to the drawing process and the associated work hardening. This material therefore has the potential for the economical production of higher-strength threaded bolts. The aim of this research project was to verify the weldability and classification of threaded studs made of 8MnSi7 in accordance with the strength classes according to ISO 898-1. A total of 91 test studs of types PD and RD with nominal diameters M8 and M20 were welded onto high-strength base materials (fy ≥ 680MPa) and subjected to centric tensile tests with static loading to fracture. Sheet thicknesses between 2 and 40 mm were used. The suitability of the 8MnSi7 threaded studs for welding was proven in the tests. Material tests showed that the threaded studs could not be fully categorised in strength class 800 (8.8). The research project therefore used statistical analyses of the test results to derive characteristic load-bearing capacities and associated partial safety factors γ* M2 in accordance with DIN EN 1990, which allow the threaded studs to be safely designed using the nominal tensile strength of 800 MPa and enable the economical use of higher-strength threaded studs made of 8MnSi7. The use of welded threaded studs made of the material 8MnSi7 (1.5113) is therefore possible. The associated verification rules have been developed and allow safe and economical use. The research project was carried out at the Technical University of Dortmund by the Chair of Steel Construction with technical support and financial support from the Forschungsvereinigung Stahlanwendung e. V., Düsseldorf, with funds from the Stiftung Stahlanwendungsforschung, Essen Authors: D. Ungermann, S. Schneider Publication: 2014
available anytime
€30.00
excl. VAT
Payment by card (Stripe) or invoice (DE, AT, CH). Download link by email: automatically after ordering by card, after order approval for invoice (valid for 30 days). Terms