
FOSTA
The new basic steel construction standard DIN 18800 was published in November 1990. In this standard, the load-bearing capacity method plays an important role in the structural safety analysis, as its application in the …
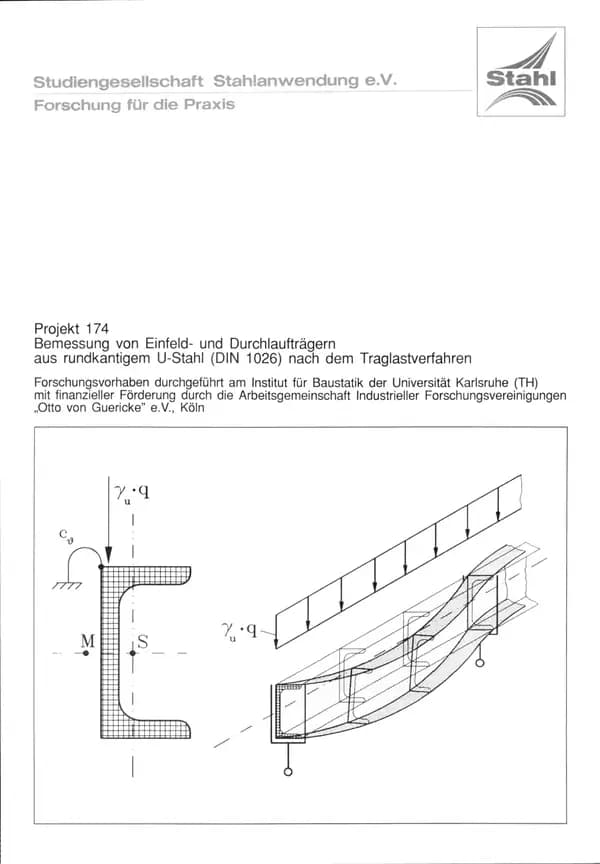
The new basic steel construction standard DIN 18800 was published in November 1990. In this standard, the load-bearing capacity method plays an important role in the structural safety analysis, as its application in the design of steel structures utilises the pronounced yielding capacity of structural steel and thus enables a more economical design on the one hand, and on the other hand a realistic statement can be made about the safety available in the structure. Up to now, there has been no simple way of determining the load-bearing capacity of U-profiles, as they are always subjected to torsional stress in addition to bending stress.
Because of the great numerical effort involved, load tests are therefore usually restricted to research institutes with appropriate computer programmes and computer equipment. The aim of this work is to determine ultimate loads for single-span and continuous beams made of round-edged U-steel (DIN 1026), taking into account a rotational bedding, and to prepare them in the form of ultimate load tables and design formulae for use in practice. This makes it possible to utilise the advantages of the ultimate load method in the design of beams made of U-section without great expenditure of time.
Machine-translated title and description. The document itself is in German.
Payment by card (Stripe) or invoice (DE, AT, CH). Download link by email: automatically after ordering by card, after order approval for invoice (valid for 30 days). Terms
Digital download
Payment by card (Stripe) or invoice (DE, AT, CH). Download link by email: automatically after ordering by card, after order approval for invoice (valid for 30 days). Terms
Other parts and editions as well as neighbouring documents of the same series.
P 100 - Development of characteristic values for the production of cold rolled profiles from the point of view of economical production of dimensionally accurate profiles Cold profiling using the roll forming process is a forming process that has been used industrially for over half a century. It allows the production of cold-formed profiles with consistent and high dimensional accuracy, some with sharp-edged bends, many curved sections, complicated double folds, with - if desired - targeted work hardening of the starting material and finally the combination of profile shaping with further processing steps such as punching, beading and bending. Although the diverse requirements and the general technical development of mechanical engineering have led to a wide variety of roll forming systems over the course of time, the technology of roll forming is still largely based on practical experience. This applies both to the dimensioning of production facilities and to the design of forming tools. This unsatisfactory situation can probably be explained essentially by the fact that the entire process - in addition to the rather difficult geometric relationships of forming - is governed by numerous working conditions which influence each other. For this reason, the Technical Committee of the German Cold Forming Association has been working closely with a well-known plant manufacturer for several years on the development and dimensioning of a machine and drive concept for research purposes. A machine and control technology solution was developed and realised which for the first time makes it possible to empirically investigate the interactions between the parameters of the production process and the properties of the product in a reproducible manner. This research work was carried out on behalf of the Studiengesellschaft für Anwendungstechnik von Eisen und Stahl e.V. by Prof. Dr.-Ing. D. Schmoeckel, Institute for Forming Technology at Darmstadt Technical University. In addition to confirming some of the results of earlier investigations, new findings of practical relevance were obtained. This applies in particular to the experiments on slip reduction, which resulted in a drastic saving in the energy used, and on the relationship between the quality of the finished product and the selected forming strategy. These results represent a step towards a better understanding of the complex manufacturing process, but at the same time demonstrate the need for further intensive efforts to conduct in-depth research into roll forming technology. The research project was funded by the Federal Ministry of Research and Technology (BMFT) and was supervised by Kernforschungsanlage Jülich GmbH (KFA) as the project sponsor for the raw materials research programme. STUDIENGESELLSCHAFT FÜR ANWENDUNGSTECHNIK VON EISEN UND STAHL e.V. Publication: 1986 Authors: Prof. Dr.-Ing. D. Schmoeckel, Dipl.-Wirtsch.-Ing. U. Eichler
available anytime
€30.00
excl. VAT