GMAW thick-wire welding with wire diameters up to d = 4.0 mm is a promising high-performance welding process which, however, has not yet enabled reproducible and economical joint welding of long weld seams. The …
GMAW thick-wire welding with wire diameters up to d = 4.0 mm is a promising high-performance welding process which, however, has not yet enabled reproducible and economical joint welding of long weld seams. The applicability of the high-performance welding process in the area of temperature-sensitive, high-strength fine-grain structural steels was also previously unknown. In the research project, the new welding process was analysed and validated with regard to its suitability for the material-specific processing of fine-grain structural steels in the thick plate range (t ? 10 mm). The base material S690Q (1.8931) was used as the reference material for the group of high-strength fine-grain structural steels within the process qualification.
In preliminary tests, a thermophysical material characterisation was carried out on a dilatometer, whereby the critical limit ranges of the cooling times t8/5 were defined and confirmed (5 s ? t8/5 ? 15 s). Within the project, systematic welding tests were carried out to analyse the influence of different wire diameters on the welding behaviour and the welding result at the upper technical test limit for MSG thick-wire welding. Solid wires of type G69 with diameters of d = 2.4; 3.0; 3.2 and 4.0 mm were used for this purpose. The solutions for controlling the energy input into the base material were aimed at extending the determined technical test limit in the upper performance range. For example, upstream wire heating, which was achieved by increasing the contact tube spacing (?s = 30 mm), resulted in a reduction in the absolute welding power requirement of up to 20 %. With the solid wire, deposition rates of approximately MR = 20 kg/h could be achieved. This corresponded to an increase in deposition rate of approx. 30 %. Furthermore, the use of a basic cored wire with a diameter of d = 3.0 mm had a positive effect on the welding behaviour and allowed deposition rates of up to approx. MR = 30 kg/h to be achieved. A separate cold wire feed into the melt during the welding process made it possible to increase the deposition rate of the thick wire process by up to 60 %. Alternatively, significantly reduced cooling times t8/5 could be realised with the help of targeted process adaptation: - Use of cored wire - 35 % - Increased contact tube spacing - 25 - Cold wire feed - 10 % In addition to the direct control of the energy and heat input into the base material, this made it possible to increase economic efficiency by increasing the deposition rate during GMAW thick-wire welding. With the process combination of cored wire, increased contact tube spacing and cold wire feed, maximum deposition rates of approx. MR = 45 kg/h were achieved in the project, which represents the current maximum value for GMAW thick wire welding. The pulsed and alternating current technologies were not considered to be effective in terms of reducing the energy input for the GMAW thick-wire welding process. In comparison with submerged arc welding, the potential of GMAW thick-wire welding was determined with regard to welding parameters and economic parameters, as well as mechanical-technological quality values for joint welds of fine-grain structural steels. Here, t = 20 mm thick sheets of grade S690Q were welded together in only 70 % of the time and with 60 % of the total costs of the submerged arc welding process using GMAW thick wire welding, while saving on powder costs and powder handling. In addition, MSG thick-wire welding enables joint welds up to t = 25 mm with just two welding beads. The process qualification (tensile tests, hardness measurements, notch impact tests and bending tests) did not result in any negative impairment of the mechanical-technological quality values of the high-strength fine-grain structural steel (S690Q) used in the case under consideration with regard to the cooling times t8/5 and processing using GMAW thick-wire welding. It was reproducibly and economically possible to place the failure location of the welded high-strength component outside the weld seam and the heat-affected zone.
Payment by card (Stripe) or invoice (DE, AT, CH). Download link by email: automatically after ordering by card, after order approval for invoice (valid for 30 days). Terms
Machine-translated title and description. The document itself is in German.
Digital download
Other parts and editions as well as neighbouring documents of the same series.

P 1314 - Space-forming load-bearing structures made of sandwich elements In addition to their outstanding space-enclosing function and thermal insulation properties, (steel) sandwich elements have load-bearing properties that allow loads to be transferred in and out of their plane. Single-storey buildings, such as small warehouses, petrol station shops and car washes, can therefore only be built with sandwich elements without additional load-bearing frame substructures. There is a lack of verification methods, in particular for load transfer, which would enable this economical construction method. The aim of the research project was to validate existing calculation approaches for load-bearing and serviceability and the detailed solutions for load transfer and distribution by means of experimental investigations and, if necessary, to develop them further. The knowledge gained from the holistic consideration of the construction method should then serve as a basis for the acquisition of a building authority approval. To achieve these goals, a self-supporting construction made of sandwich elements was first designed as an example object. For this purpose, all necessary construction drawings and detailed solutions for the formation of the load application points and joints were worked out and defined for this application. Experimental investigations into the load-bearing behaviour of a self-supporting construction made of sandwich elements were carried out using a test matrix defined in the research proposal. The extensive local and global axial compression tests were carried out on test specimens, taking into account a practical and application-related design of the load application points. The deformations and maximum loads were measured. The measured loads were then statistically evaluated and the actual local and global load-bearing capacity as well as the failure behaviour of the self-supporting construction made of sandwich elements were analysed. The analytically determined ultimate loads in the ultimate and serviceability limit states were used as a reference. It was found that the experimentally determined loads were far higher than the analytically calculated values. This showed that the design of the structure with the existing design approaches provides conservative results and is therefore on the safe side. The design of the load introduction structure for uplifting forces could also be ensured using a presented design approach. In order to ensure a holistic view of the construction, an economic and ecological analysis of the construction method was carried out. In the economic analysis, it was shown that self-supporting constructions made of sandwich elements without a steel substructure save approx. 9% of the investment costs and approx. 10% of the heating costs. The life cycle assessment also showed that the construction method results in emission and energy savings and is more environmentally friendly. Overall, the research report provides a sound scientific and technical basis for the design, construction and dimensioning of self-supporting structures made of sandwich elements, as well as the necessary test results and analyses for obtaining building authority approval. Publication: September 2022 Authors: Univ.-Prof. Dr.-Ing. D. Ungermann, M.Sc. G. A. Eseme
available anytime
€30.00
excl. VAT

P 1313 - Bimodal toughness behaviour of ultra-high toughness pipeline steels - cross-scale root cause analysis and adapted evaluation concepts For many decades now, fossil fuels have been transported through kilometres of pipelines. The need for a reliable pipeline transport network will continue to be indispensable in the future in order to make hydrogen available to end consumers as an energy source in addition to fossil fuels. The pipeline steels required for the conversion and expansion of the supply network have been continuously improved in recent years thanks to the great efforts of the steel and pipeline industry. Thanks to thermo-mechanical rolling strategies and an increase in the purity of the steels, damage-tolerant microstructures have been developed, leading to an increase in strength and toughness properties. These excellent material property profiles offer great resource-saving lightweight construction potential for future applications. However, these modern pipeline steels are subject to failure phenomena during toughness testing that have not yet been sufficiently researched. These include inverse fracture behaviour, fracture surface tearing and compressed or overlapping transition behaviour. The latter is characterised by an overlap of the low and high layer branches over a temperature range of 10-30°C in the notched impact energy-temperature diagram, which in turn leads to uncertainties in component design and associated application inhibitions. As part of this project, a bainitic pipeline material of grade X65, which exhibits overlapping toughness behaviour, was extensively characterised. Titanium nitrides (TiN) and calcium sulphides (CaS) were identified as crack-initiating structural components for both brittle and ductile material failure. Using microstructure simulations, it could be shown that the local stress and strain concentrations in the microstructure vary greatly depending on the position, size and tilting of the inclusion. The highest stress concentration was found for a 6 µm TiN inclusion with a 45° tilt. The development of a cross-scale simulation methodology subsequently made it possible to evaluate the influence of different inclusion configurations on the material and component behaviour. The microstructure-related parameter sets derived in the simulation of representative volume elements (RVE) were used in the macroscopic damage model to map the material behaviour in the notched bar impact test. Using this methodology, the compressed transition behaviour could be described numerically and the model transferred to piping applications. In the component simulations, brittle or ductile component failure occurs in the pipeline pipe depending on the selected microstructure-based parameter set. A microstructure with critical inclusion leads to brittle component failure and a higher crack propagation velocity, while a microstructure without critical inclusion causes ductile component failure. The developed cross-scale simulation approach for microstructure-based component evaluation can be transferred to other material concepts and areas of application in the future. On the one hand, this makes it possible to support the clarification of material-physical phenomena and, on the other hand, to inspire integrative material and component design for resource-saving lightweight construction. Publication: 2021 Authors: Prof. Dr.-Ing. S. Münstermann, M.Sc. Y. Sparrer
available anytime
€30.00
excl. VAT

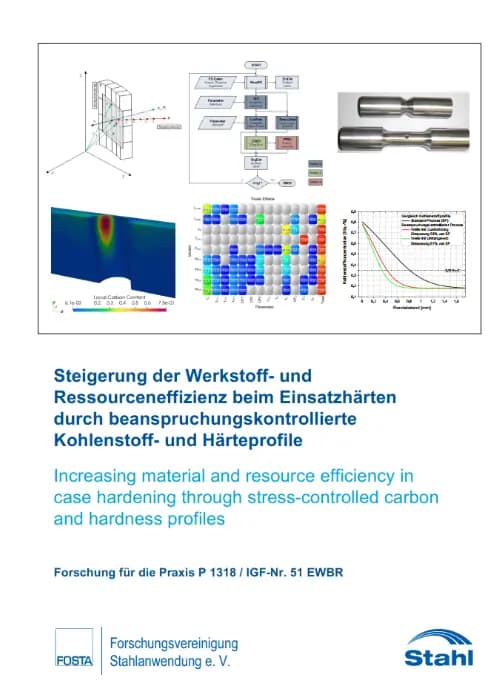
P 1318 - Increasing material and resource efficiency in case hardening through stress-controlled carbon and hardness profiles The thermochemical case hardening process can increase the required local material strength against component failure of steel components. The basis for this is the increase in material hardness as a result of higher-strength structural components and the associated induction of residual compressive stresses in the failure-relevant component edge area. In addition to their effect as mould notches on component strength, design details also have an effect on key component properties after case hardening, such as surface carbon content and surface hardness as well as carburisation and case hardening depth. At present, component notches are neither taken into account within the component-related specification of target values for case hardening nor within the definition of process parameters by the control and regulation software of case hardening systems. The research project developed a concept for the numerically based determination of stress-controlled target and process parameters for case hardening. In this concept, the condition of the steel component as a result of an external load forms the decisive basis. The actual stress condition in the failure-critical area of the steel component is decisive. The necessary target values for case hardening are defined for precisely this area. The process parameters required to meet the target values are generated taking into account the geometry of the failure-relevant component area. This makes it possible to significantly reduce the required carburising and case hardening depths and thus the overall process times for the respective case hardening of steel components. Compared to the previous empirical approach, the energy and resource efficiency of case hardening can thus be increased. The analytical results of the research project were validated using shaft samples made of 16MnCrS5 case-hardening steel with different design details acting as mould notches. Compared to standard case hardening in practice, the total process time was reduced by 53 % in the case of stress-controlled case hardening of the shaft with a transverse bore and by 61 % in the case of stress-controlled case hardening of the shaft with a circumferential notch. Vibration tests carried out in the fatigue strength range showed that stress-controlled case hardening does not have any negative effects on the load-bearing capacity of the shaft samples. Publication: June 2022 Authors: Dr.-Ing. A. Diemar, Dr.-Ing. U. Gerth, Prof. Dr.-Ing. habil. C. Könke
available anytime
€30.00
excl. VAT

P 1311 - Stress-optimised repair of welded joints in the production of components made of high-strength fine-grained structural steels During the assembly of steel structures, unacceptable irregularities are occasionally detected in the weld area, despite the fact that the welds have been produced in accordance with the requirements. The processing regulations recommend localised thermal gouging of affected areas and rewelding, but provide little information on adequate repair concepts due to a lack of scientifically sound investigations. This applies in particular to the consideration and optimisation of resulting welding-related stresses due to high shrinkage restraints in the gouging grooves and the structural degradation of adjacent areas due to gouging and rewelding. Especially with high-strength steel grades, this often results in reduced mechanical properties and additional welding-related stresses as well as recurring weld defects. For this reason, systematic component-relevant investigations of the welding-related stresses and structural changes in repaired weld seams were carried out for the research project as a function of the shrinkage restraint and heat conduction during welding and gouging as well as the number of repair cycles. The results of the investigation show which factors are suitable for reducing stresses even under high clamping conditions and how degradation of the microstructure and properties of the weld seam and repeated weld seam defects in the repair seam can be avoided. In particular, adaptive heat conduction can be used to reduce welding-related stresses in the repair weld seams. Component tests also ensure the transferability of the welding experiments into practice. Based on the findings, recommendations for stress and material-appropriate repair concepts could be derived and made. The analyses were carried out on the high-strength steel grades S500MLO for the offshore sector and S960QL for mobile crane construction. This takes particular account of the economic production of highly efficient structures for wind turbines and the high-strength structures required for their erection. The research results provide an essential basis for the further development of corresponding standards and regulations. This can ultimately prevent damage and often expensive reworking and improve the utilisation of the high strength potential of high-strength steels. SMEs in particular can also benefit from the findings on the use of high-strength steels, which are necessary for the efficient realisation of the energy transition in Germany, with regard to the costs of production, welding work and materials. Publication: July 2022 Authors: M. Sc. A. Becker, Dr.-Ing. D. Schröpfer, Univ.-Prof. Dr.-Ing. habil T. Kannengießer
available anytime
€30.00
excl. VAT
Payment by card (Stripe) or invoice (DE, AT, CH). Download link by email: automatically after ordering by card, after order approval for invoice (valid for 30 days). Terms