One effective way of reducing emissions from passenger cars is to reduce the weight of the vehicle. The greatest savings potential lies in the area of car body construction, where, for example, high-strength steels are …
One effective way of reducing emissions from passenger cars is to reduce the weight of the vehicle. The greatest savings potential lies in the area of car body construction, where, for example, high-strength steels are now replacing conventional thin sheet materials. However, the use of high-strength steels to increase vehicle safety in the event of a crash is particularly challenging. One of the most efficient processes for manufacturing crash-relevant components, such as the B-pillar, is press hardening, in which forming and hardening are combined in a single process step. The material 22MnB5 (1.5528) is currently used in the industrial series production of press-hardened components, but its ductility in the hardened state is limited due to the alloy concept.
An improved property profile consisting of strength and residual formability is being sought for increased vehicle occupant safety in the event of a crash. This project is therefore concerned with the development of new alloy concepts and process strategies to improve the residual formability of press-hardened steels. Three different alloying concepts were investigated: the dual-phase concept (DP), the grain refinement concept (KF) and the retained austenite concept (RA). Depending on their chemical composition, different heat treatment cycles were combined with press hardening for a total of 6 steels. The investigations focussed on the microstructure development and the resulting characteristic properties in the tensile and bending test. In addition, the coatability and further processability by welding were investigated. It was demonstrated that an improvement in the ductility of press-hardened materials in the RA concept can be achieved by complex Q&P structures (quench&partitioning). In contrast, the DP and KF concepts, which were also investigated, showed only a marginal improvement in the property profile. The best properties in the RA concept result for a material with 0.3 wt% C and 2.5 wt% Mn with tensile strength values of 1400-1500 MPa and elongation at break values of 14-19 % depending on the respective heat treatment. Further tests on this alloy show that the material is temper resistant and therefore suitable for stove enamelling in vehicle production. Joining can be carried out by both laser beam and spot welding. Hot-dip coating with both AlSi and zinc coatings is possible in principle. This project has thus succeeded in demonstrating possibilities for improving the material properties of press-hardened steels using a Q&P heat treatment strategy. The crash absorption potential of the materials produced was doubled compared to the reference material 22MnB5.
Payment by card (Stripe) or invoice (DE, AT, CH). Download link by email: automatically after ordering by card, after order approval for invoice (valid for 30 days). Terms
Machine-translated title and description. The document itself is in German.
Digital download
Other parts and editions as well as neighbouring documents of the same series.

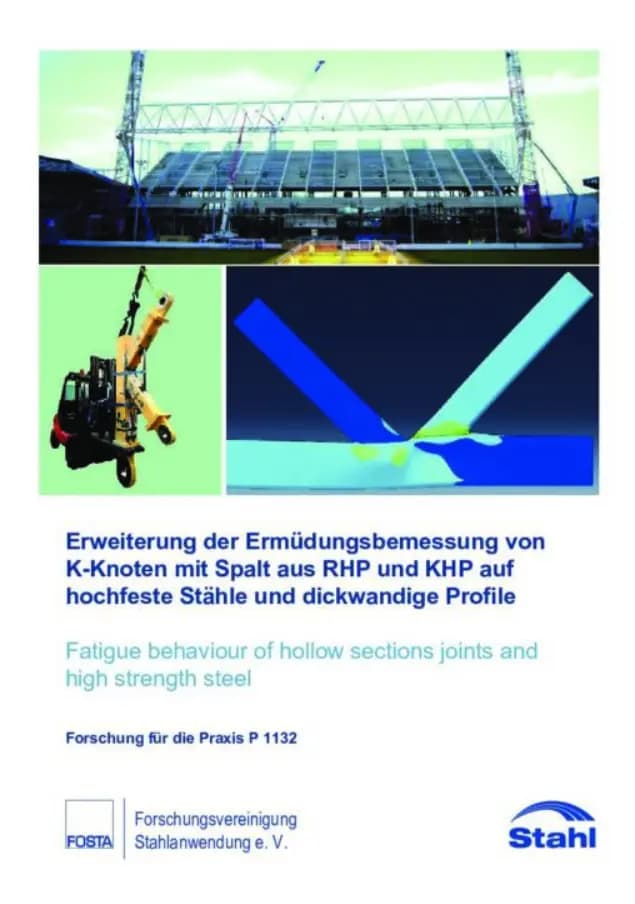
P 1132 - Extension of the fatigue design of K-nodes with gap made of RHP and KHP to high-strength steels and thick-walled sections Fatigue-stressed structures are increasingly being manufactured from high-strength steels in order to realise lightweight construction. In truss construction, the K-node with gap is the favoured node configuration. To facilitate the application and design of such nodes made of high-strength steel grades and with greater wall thicknesses, the existing design rules must be adapted and extended. The test programme carried out for this purpose comprises a total of 55 fatigue tests on K-nodes made of rectangular hollow sections (RHP) and circular hollow sections (KHP) of different dimensions made of S355, S500 and S700. K-knots of smaller dimensions are tested at TNO in Delft, Netherlands, on a test rig with individual cylinders. K-knots with large dimensions are tested at KIT in Karlsruhe on a specially manufactured test frame. The experimental tests are analysed according to the nominal stress concept of EN 1993-1-9 (2010) by creating Wöhler curves. In particular, the tests on small KHP K nodes with a welded gap show that the fatigue strength depends not only on the node dimensions and geometric parameters but also on the weld design and geometry. This is not taken into account in the design rules, but can be used for the design of fatigue-compliant structures. For example, the fatigue strength of KHP K nodes with a welded gap can be increased by two notch classes from 71 to 90. In contrast, the small RHP K-nodes investigated are manufactured with weld start and end points in the corners of the strut profiles, which means that the weak point of the weld seam coincides with the hot spot of the geometry. The test results of these test specimens therefore represent a lower limit for the fatigue strength. The fatigue strength of K-nodes depends heavily on the wall thickness of the components and their ratio value <span class="fontstyle3">t</span>. The classification for the nominal stress approach is therefore rightly based on the inverse wall thickness ratio 1/<span class="fontstyle3">Τ = t0 / Τi. The results of the fatigue tests on large RHP and KHP K-nodes made of S355 and S700 with 20 mm wall thickness fit well into the existing notch classes and can be categorised according to CIDECT Design Guide 8 or EN 1993-1-9 (2010) without wall thickness reduction. In parallel, numerical calculations are carried out to extend the scope of validity. The finite element models are calibrated using strain measurements in verification tests. Volume elements are used for this purpose and the weld seams are also modelled in order to enable an exact representation of the local stresses in the weld seam. A parameter study is carried out to extend the parameter range under consideration and to identify the influence of individual geometric parameters such as chord slenderness 2<span class="fontstyle3">y, wall thickness ratio <span class="fontstyle3">t, width or diameter ratio ß or strut inclination angle O<span class="fontstyle3">. For RHP K-nodes, 72 different node configurations are calculated, each with 4 separate load cases. KHP K-nodes are calculated in 16 different dimensions with 3 load cases each, so that a total of 336 FE models are created, calculated and analysed within the parameter study. In addition, stress concentration factors are determined on the basis of the strain measurements in the test. These are then used together with the results of numerical parameter studies to validate or adapt existing SCF formulae. For RHP K-nodes, a re-evaluation of previous and new data for the load case "Axial loading of the strut (AX)" is carried out and suitable formulas with a slight modification of existing CIDECT formulas are provided. For RHP K-nodes with gap under in-plane strut bending (IPB), no formulae are given in CIDECT. A new set of equations has been developed for this purpose. The evaluation of the structural stresses of KHP K-nodes under axial loading of the struts shows that the SCFs according to CIDECT formulas often provide very conservative values compared to the SCFs according to DNV GL-PR-C203 (2016) and from FEA. Since DNV GL-PR-C203 (2016) has a wider range of application and provides SCF formulas for the IPB and out-of-plane bending (OPB) load cases, it makes sense to use these formulas. Only the formula for SCFs for the belt under IPB is modified so that the SCFs are on the safe side. As the fatigue strength of hollow section connections is heavily dependent on the non-dimensional parameters, this should be taken into account at the planning stage by selecting suitable parameters. Through careful planning and execution, fatigue-resistant hollow section structures can be realised, even when using high-strength steels. Publication: March 2020 Authors: Dr.-Ing. S. Herion, Dr.-Ing. Hrabowski, Prof. Dr.-Ing. T. Ummenhofer, Dipl.-Ing. P. Ladendorf, Dr. ir. R. Pijpers
available anytime
€50.00
excl. VAT

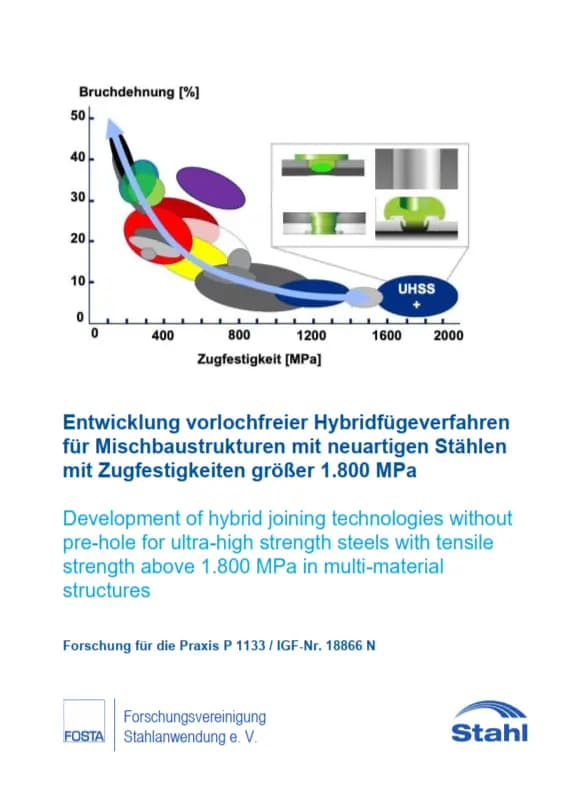
P 1133 - Development of pre-hole-free hybrid joining processes for mixed structures with novel steels with tensile strengths greater than 1,800 MPa The statutory regulations to reduce greenhouse gas emissions are prompting the automotive industry to implement consistent lightweight construction. The reduction of CO2 emissions to an average of 95g CO2/km in passenger car traffic by 2020 has been agreed. The vehicle body, which accounts for over 30% of the total weight, offers the greatest potential for implementing lightweight construction, which can be achieved by using high-strength steels and other lightweight materials such as aluminium. In particular, the mixed construction of press-hardened 22MnB5 steel and aluminium in combination with adhesive bonding leads to economical lightweight construction solutions. Even higher degrees of lightweight construction can be achieved by using even stronger steels with strengths above 1800 MPa (referred to as "UHSS+" in this report). This allows a further reduction in material thickness to be achieved while essentially maintaining component performance. The prerequisite for a design made of UHSS+ in combination with aluminium structures is the applicability of a cost-efficient and robust joining technology. The aim of the research project is therefore to develop pre-hole-free hybrid joining processes for mixed structures with new types of steel with tensile strengths greater than 1,800 MPa. To this end, the processes of solid self-pierce riveting, semi-tubular self-pierce riveting, friction element welding and resistance element welding are being qualified for joining the aforementioned material combination by adapting the process parameters, the tools and the auxiliary joining parts. In the case of semi-tubular self-pierce riveting processes, numerically supported optimisations of dies are used to determine various options for improving the joint quality. The deformations in solid self-pierce riveting can be reduced through the use of upset area dies. For the element welding processes, on the other hand, the process parameters are adapted so that welds with reproducibly good mechanical strength properties are possible. In addition, local conditioning is used to modify the UHSS+ sheet materials so that joinability can also be guaranteed with conventional mechanical joining processes. The results presented for hybrid joining indicate that the processes shown can be combined well with adhesive bonding technology. The determined property profile of joints made of UHSS+ and the aluminium alloy EN AW-5182 shows that a reproducible joint quality can be achieved. Publication: 2021 Authors: Prof. Dr.-Ing. G. Meschut , Sc. V. Sartisson
available anytime
€30.00
excl. VAT

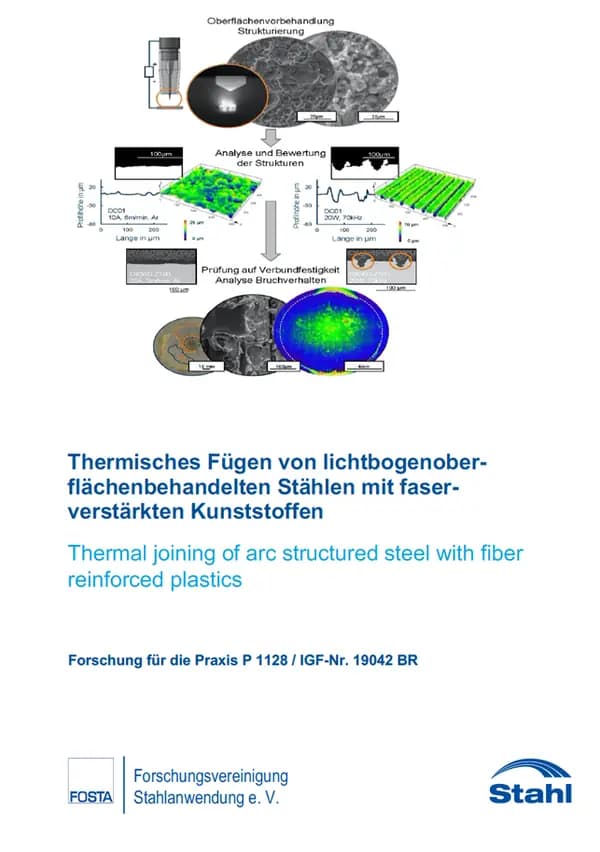
P 1128 - Thermal joining of arc surface-treated steels with fibre-reinforced plastics The thermal joining of metallic and polymer materials offers advantages over mechanical joining processes and bonding. In order to achieve sufficient adhesive strength, it is advantageous to increase the surface area of the metallic joining partner. Beam or laser processes are mainly used for this purpose. The surfaces produced are evaluated by determining geometric parameters, but also by wettability tests. Depending on the material and structuring process, adhesion strengths of between 5.2 MPa and 43 MPa could be researched in the available literature. Surface structuring using electric arcs has hardly been documented to date. The structures produced are highly irregular and it is not known to what extent existing methods can be used for surface evaluation. The aim of the project was to structure metallic surface structures using conventional arc technology. The surface-treated metals are used to produce hybrid metal-plastic composites. Laser structures were generated in continuous wave (cw) and pulsed mode as a reference for the arc structure. The focus of the investigations was the characterisation of the generated structures with regard to their topographical and energetic properties as well as their effects on the wetting and the resulting fracture behaviour. The investigations were initially carried out on model point-shaped tests to determine the tensile strength for different material pairings. The results were then transferred to industrial joining geometries (linear tests). In addition to the materials mentioned, fibre-reinforced thermoplastics were also used. The knowledge gained is intended to contribute to current research into new joining processes for hybrid material composites. The process parameter analysis for the creation of laser-structured surfaces in pulsed and cw laser operation shows clear differences in the achievable structural shapes. Using the cw process, mainly deep structures can be produced. The number of passes is decisive for the geometry of the resulting pattern. From a number of passes of i = 2, a drop-shaped pattern with undercuts is produced. Pulsed laser radiation can be used to create wide, flat structures with low pulse frequencies (f = 20 kHz). As the pulse frequency increases (f = 60 - 70 kHz), drop-shaped structures can be produced due to the resulting pressure. Publication: January 2021 Authors: M.Sc. M.-L. Solf, Dr.-Ing. K. Schricker, Univ.-Prof. Dr.-Ing. habil. J. P. Bergmann, Dipl.-Ing. M. Lohse, Dr.-Ing. M. Hertel, Prof. Dr.-Ing. habil. U. Füssel
available anytime
€30.00
excl. VAT

P 1135 - Hot moulding process integrated surface structuring for hybrid components Due to increasing requirements in the areas of safety, comfort and lightweight construction, the demand for structural parts made of ultra-high-strength steels is growing in the automotive body-in-white. By using these steels, the sheet thickness of the components can be reduced and thus the weight lowered. However, the production of complex geometries proves to be problematic due to the high mechanical strength, as large loads act on the forming tools and the process accuracy is impaired by the springback behaviour. The press hardening process provides a solution to this problem. Press hardening is a non-isothermal process that combines the forming of the component and the hardening of the material. In this process, martensitic hardening of the sheet metal component can be achieved. However, stability problems with reduced sheet thicknesses limit the lightweight construction potential of press-hardened components. In other branches of industry, such as the aerospace industry, structural components are often made from fibre-reinforced plastic composites (FRP) or, in more recent approaches, in a hybrid composite of metal and FRP, while high-strength steels continue to dominate the automotive mass market. A targeted combination of metal and FRP leads to stress-adapted and cost-effective hybrid lightweight structures. In the load application area of such hybrid components, concentrated, three-dimensionally effective load collectives often occur, which are preferably absorbed by isotropically acting metallic components. The transition area or the interface from the metallic component to the fibre composite structure, where the forces have to be transferred, is critical. New surface pre-treatment processes can help to improve component performance by creating targeted interlocking effects. The aim of this project is to develop a process that introduces surface structuring into the hot forming process of high-strength steels in order to subsequently achieve improved bonding of fibre-reinforced plastics. The structuring is applied using the corresponding hot forming tool, which eliminates an additional work step compared to other structuring processes. For this purpose, a tool for structuring at sample body level is first developed, with which the samples are simultaneously structured and hardened. The mechanical properties of the hybrid structures made of FRP and 22MnB5 are then determined experimentally. Based on the knowledge gained, the method is then applied to an automotive body structure and validated. Publication: 2020 Authors: T. Tröster, K. Dröder
available anytime
€30.00
excl. VAT
Payment by card (Stripe) or invoice (DE, AT, CH). Download link by email: automatically after ordering by card, after order approval for invoice (valid for 30 days). Terms