In the interests of saving resources in an environmentally friendly manner, lightweight construction concepts are becoming increasingly important in the development and production of sustainable products. Many of these …
P1006 - Design of cold-bonded steel-FVC mixed joints for structures subject to sudden loads In the interests of saving resources in an environmentally friendly manner, lightweight construction concepts are becoming increasingly important in the development and production of sustainable products. Many of these concepts are characterised by the term mixed construction. Weight savings can be achieved in combination with high-strength steels through the use of fibre-reinforced plastic composites (FRP), which are excellent lightweight construction materials due to their properties. Joining technology plays a special role in the realisation of mixed joints.
Cold-curing 2-component adhesives are increasingly being used for steel-FRP mixed joints. However, the realisation of the lightweight construction concept must not compromise the customer-specific requirement for safety. The crash behaviour of steel-FRP composite joints in particular must therefore be taken into account. The failure behaviour of a bonded FRP composite joint is significantly more varied and less calculable compared to a bonded steel-steel joint. While a bonded steel-steel joint can lead to a cohesive adhesive layer or joint part failure if there is sufficient adhesion between the adhesive and the joining partners, fibre-reinforced plastics also exhibit inter-fibre cracks, fibre cracks and delamination due to their anisotropic structure. The overarching aim of the research project was to develop a method for designing cold-bonded steel-FRP mixed joints for structures subject to sudden loads. In this context, a mixed joint is understood to be the combination of fibre-reinforced plastic composites and typical materials corresponding to cold bodyshell construction or assembly, such as KTL-coated or painted sheet steel. The focus is on the influence of the structural design of the fibre-reinforced composites as well as an optimal joining zone design for material-compatible force transmission into the joined parts in order to guarantee a connection that is as impact-resistant as possible. In this way, the potential of the high-performance materials (steel in combination with fibre-reinforced composites) is to be fully exploited. The results obtained as part of the research project will enable steel processors to design and optimise crash-relevant or impact-loaded components made of steel and FRP with regard to the bonding technology, so that new lightweight products can be realised with reduced testing costs for steel manufacturers and processors. Responsible for FOSTA - Forschungsvereinigung Stahlanwendung e. V. Dipl.-Ing. Franz-Josef Heise
Payment by card (Stripe) or invoice (DE, AT, CH). Download link by email: automatically after ordering by card, after order approval for invoice (valid for 30 days). Terms
Machine-translated title and description. The document itself is in German.
Digital download
Other parts and editions as well as neighbouring documents of the same series.

P 1005 - Investigations into the load-bearing behaviour and service life of bonded joints in steel structures under cyclic loading The use of innovative adhesive bonding technology increases the productivity, quality and efficiency of German steel construction. It also represents an alternative to conventional joining methods, which have fundamental disadvantages for steel structures. For example, the bonding joining process can avoid welding-related component distortion and cross-sectional weakening due to bolt holes. Due to the high degree of prefabrication, steel construction is predestined for the use of adhesive bonding, as load-bearing, serviceable and durable bonded joints can be produced under workshop conditions. However, it is not possible to verify such bonded steel joints on the basis of current standards. Time-consuming and expensive approval procedures would be necessary, which is why small and medium-sized enterprises (SMEs) decide against adhesive bonding technology. The inclusion of bonded steel joints in standardisation would provide a remedy here. For this reason, the first step is to develop basic principles for the verification of load-bearing capacity using two application cases from steel façade construction, which relate exclusively to short-term, one-off and quasi-static loads. A further aim of the project is to supplement these findings by investigating the long-term load-bearing behaviour of bonded joints under cyclic loading. The results of the analyses provide input parameters for the development of verification concepts for bonded steel joints. Publication: 2018 Authors: Prof Pasternak, Prof Dilger
available anytime
€30.00
excl. VAT

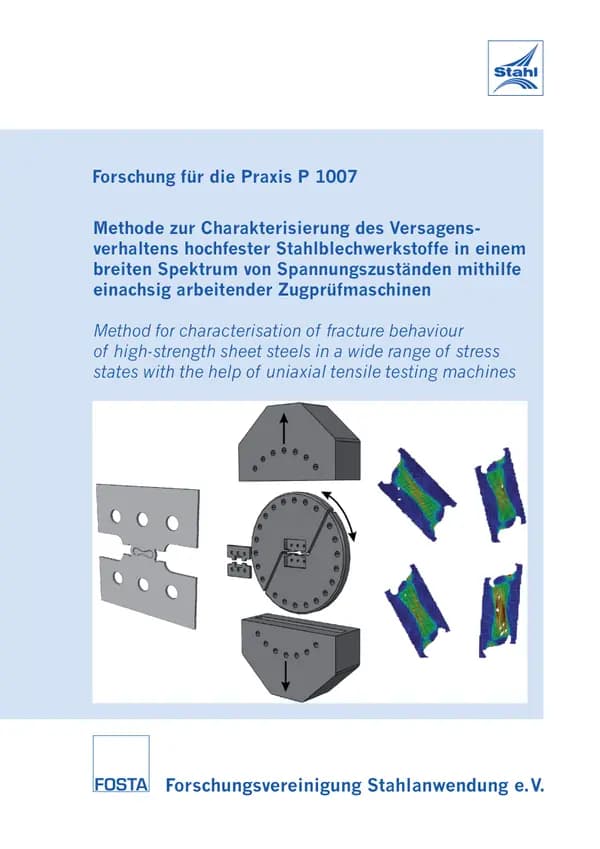
P 1007 - Method for characterising the failure behaviour of high-strength sheet steel materials in a wide range of stress states using uniaxial tensile testing machines The main objective of the project was to develop a new method for characterising the failure behaviour of high-strength sheet steel materials. This method should be based on shear tensile tests on new shear tensile specimens using a new testing module in uniaxial tensile testing machines as well as on hydraulic cupping tests and enable failure characterisation in a wider range of stress states compared to the conventional forming limit curve. The core of the developed approach is the new shear tensile specimen, which is characterised by a localisation of deformation leading to crack initiation inside the material and not at a free edge, regardless of the direction of an external uniaxial load in the specimen plane. A new test module was designed and manufactured for the shear tensile tests on the new shear tensile specimens, which applies a uniaxial test load into the following stresses in the material to be tested: a uniaxial tensile load with a superposition of hydrostatic tension, five different tensile shear loads with a dominant tensile or shear component and a compressive shear load with a dominant shear component. The degree of failure deformation of a dual-phase sheet steel material was experimentally determined using shear tensile tests with five different specimen orientations to the test load using an optical measuring system. In addition, the prevailing stress triaxiality at the material point of crack initiation was determined by numerically modelling the shear tensile tests performed. By combining the respective mean value of the experimentally determined degrees of failure deformation and the respective characteristic value of the numerically determined stress triaxiality, a support point for the fit of the material-specific failure curve was obtained for each tested material stress. In addition to these five support points, a support point from hydraulic cupping tests was also included. From the relative arrangement of the six support points, it can be seen that the dependence of the degree of failure deformation on the stress triaxiality is fundamentally captured using the developed approach. Although the work carried out confirms the fundamental suitability of the approach for characterising the failure behaviour of high-strength sheet steel materials, it also reveals possibilities for its further development. Individual focal points of this further development are an optimisation of the sample geometry to suppress edge cracks, an investigation into the influence of sample production on test results, improvements in recording the time and position of crack initiation and an investigation into the transferability of test results to the numerical simulation of forming processes. In the foreseeable future, these focal points are to be addressed more intensively in newIF UM research projects in order to promote acceptance of the newly developed method in the simulation-based design of sheet metal forming processes in the research landscape and in industrial practice. The research project P 1007 of the Forschungsvereinigung Stahlanwendung e.V., Düsseldorf, was carried out by the Institute of Forming Technology and Machines, University of Hanover, with technical support and financial assistance from FOSTA. Publication: 2015 Authors: B.A. Behrens, M. Vucetic, I. Peshekhodov
available anytime
€20.00
excl. VAT

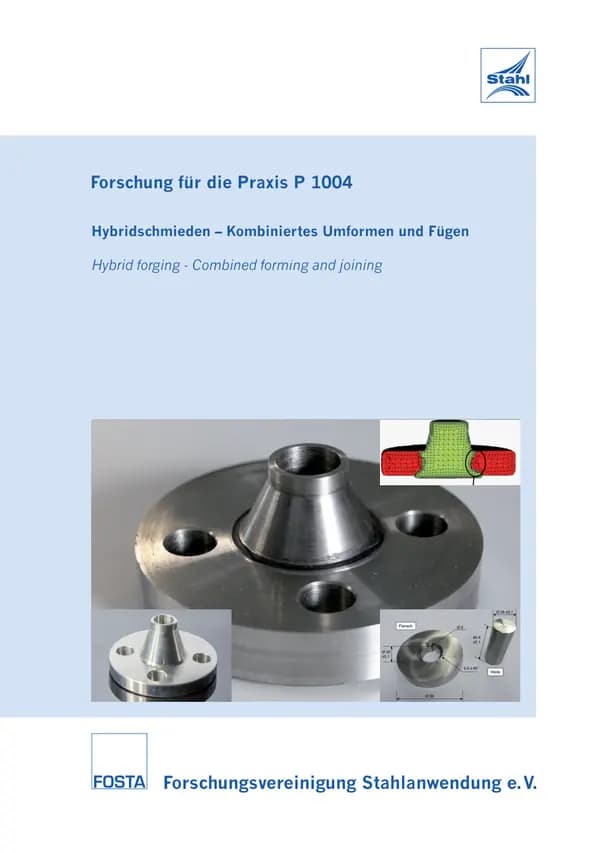
P 1004 - Hybrid forging - Combined forming and joining This study investigated the feasibility and potential of a hot Hyrid forging process for a pressure flange. This process is characterised by the simultaneous forming and joining of a thick plate and a shaft in one step. Firstly, the process was designed using FEM software. Compared to a reference process, significant reductions in the press force were achieved, making it possible to forge larger flanges on smaller forming units. The stainless steel X6CrNiMoTi17-12-2 (1.4571) was used as the material. Tests were then carried out on an industrially used eccentric press. The key feature was to ensure a positive fit between the two components, as it was not possible to achieve a material bond. For this purpose, the sheets were provided with a chamfer and recesses, which were filled with the material of the shaft during the forming process to prevent axial and radial displacement. This goal was achieved. To achieve this, however, the sheet metal had to be heated more than the shaft material, as otherwise gaps would have formed after cooling due to thermal shrinkage. The pressing forces could also be reduced in reality. Normally, the real process requires press forces of approx. 800 tonnes for forging with burrs. These forces are higher with burrless forging. A significant reduction in pressing forces has therefore been achieved. Forging companies can now manufacture rotationally symmetrical parts in a manual production process using hybrid forging. This means that parts can be produced without burrs with a low forming force. This leads to a reduction in tool stress and thus to an increase in tool life. Smaller presses can be used for comparable parts. Automation including feeding technology is still to be developed. This means that long parts can also be produced, which make up a larger proportion of solid moulded components in industry. The research project P 1004 of the Forschungsvereinigung Stahlanwendung e.V., Düsseldorf was carried out by the IPH - Institut für Integrierte Produktion Hannover GmbH with technical support and financial assistance from the Forschungsvereinigung Stahlanwendung e. V., Düsseldorf. Publication: 2015 Authors: J. Langner, M. Stonis
available anytime
€20.00
excl. VAT

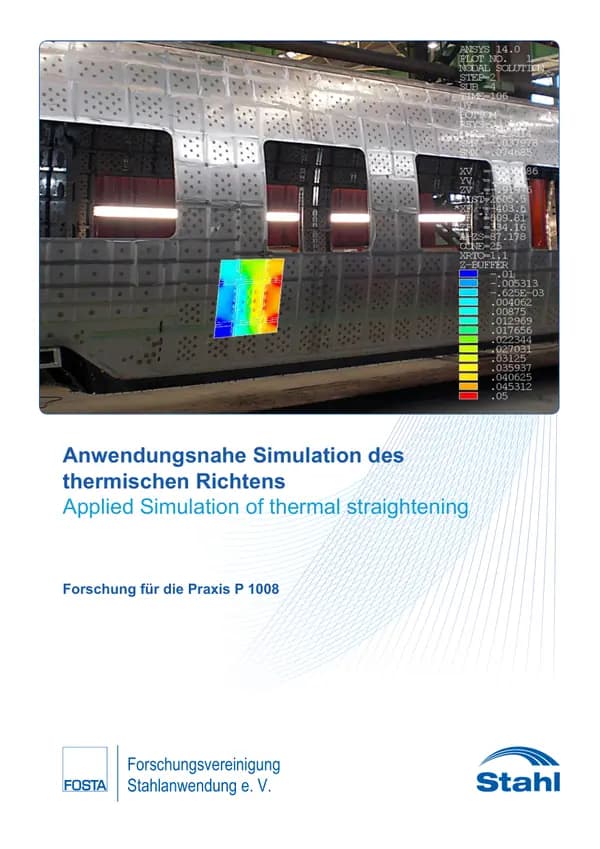
P 1008 - Application-oriented simulation of thermal straightening Particularly in the case of large structures, such as those welded in ship and rail vehicle construction, the remaining distortions are very critical due to their enormous dimensions of up to several centimetres. Post-treatment must therefore be included in the work planning just as much as the welding itself. Thermal straightening has been an established process for decades. The straightening process parameters are currently selected on the basis of practical experience. However, the influence of design conditions, the material and the different straightening processes are extremely difficult to determine in this way. The basics of the analytical model, the realisation for practical application and the coupling with the numerical calculation are presented. The coupled analytical-numerical hybrid model is designed to capture the welding process chain and the subsequent thermal straightening. The analytical model is used to determine the equivalent shrinkage strain for the thermomechanical load of each straightening point, taking into account the significant influencing factors. This is transferred to an FE model of the structure and the deformation of the entire structure is calculated using an elastic analysis. The mutual influence of the existing residual welding stresses and individual alignment points is taken into account iteratively by means of feedback. The calculation is based on the application of the analytical numerical hybrid model for welding distortion simulation. The methodological approach is explained in detail in the report. In addition to the fundamentals of the hybrid model, other important aspects such as the recording of different straightening processes, process conditions and industry-relevant materials are also discussed. In addition, the qualitative interaction between thermal levelling and the welding process was investigated and integrated into the calculation procedure. The hybrid model was initially applied and validated on simple sheet metal specimens. Based on a structure joined by means of eight seams, the consideration of the welding sequence and the straightening sequence in the hybrid model was investigated. in the hybrid model was analysed. This was then applied to a test structure from the railway vehicle construction industry. Four 2 mm thick profiles were joined to a base plate measuring 500 x 400 mm using 16 weld seams and then straightened using two independent scenarios. The CPU time of the numerical calculation on the structures was less than 10 minutes in each case. The validity of the calculations was thus verified experimentally. Publication: 2016 Authors: V. Mikhailov, N. Doynov, F. Kuke
available anytime
€30.00
excl. VAT
Payment by card (Stripe) or invoice (DE, AT, CH). Download link by email: automatically after ordering by card, after order approval for invoice (valid for 30 days). Terms